Organic fertilizer pneumatic conveying systems represent a sophisticated approach to material handling in agricultural and industrial settings. These systems utilize air pressure to transport organic materials, such as compost, manure, and other biodegradable substances, from one location to another. The core principle involves creating a pressure differential that propels the material through a pipeline network, enabling efficient and hygienic transfer without the need for mechanical components like belts or buckets.
Key Components and Operational Mechanism
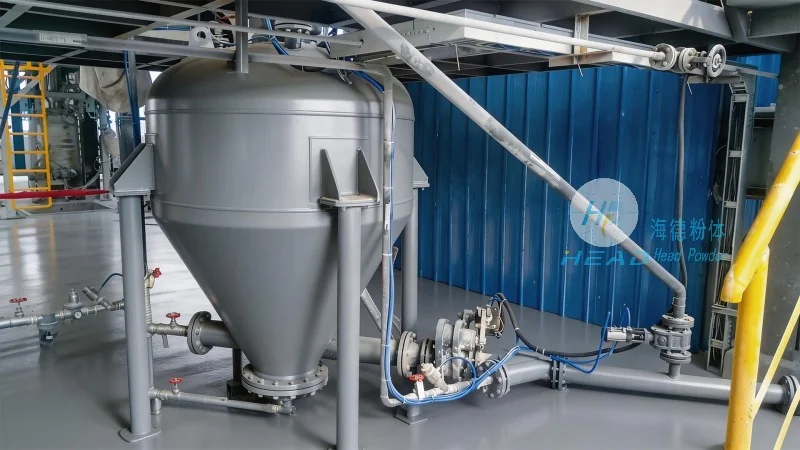
The effectiveness of an organic fertilizer pneumatic conveying system is determined by its integrated components, each playing a critical role in the overall process. The system typically includes a material feed hopper, a blower or compressor that generates the necessary air pressure, a pipeline network for material transport, and a discharge unit at the destination. The feed hopper ensures a consistent supply of organic material, while the blower provides the motive force. As the material is introduced into the pipeline, it is entrained by the moving air, creating a slurry-like mixture that travels through the system. The discharge unit then separates the material from the air, allowing for clean and efficient delivery at the end point.
Advantages of Pneumatic Conveying for Organic Fertilizers
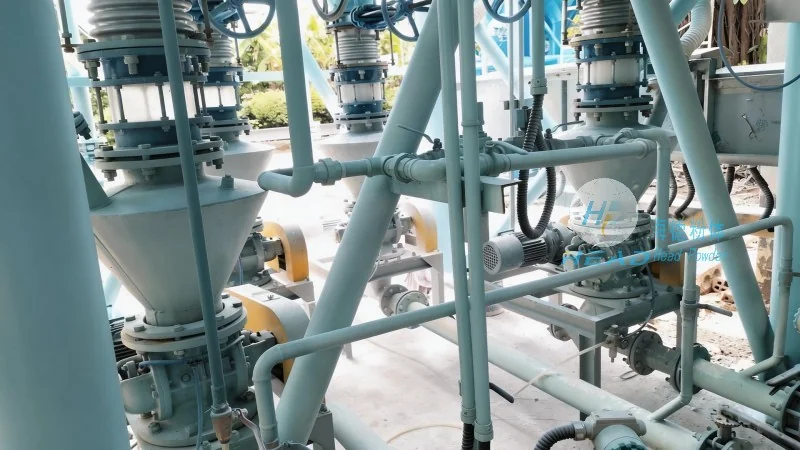
Compared to traditional mechanical conveying methods, organic fertilizer pneumatic conveying systems offer several distinct advantages. Firstly, they provide a hygienic and dust-free environment, which is crucial for maintaining the quality of organic materials and preventing contamination. Secondly, the system minimizes material degradation, as the lack of mechanical contact reduces the risk of breakage or compaction. Additionally, pneumatic conveying allows for flexible pipeline configurations, enabling the system to adapt to various site layouts and operational requirements. The energy efficiency of these systems is also notable, as they can achieve high material throughput with relatively low power consumption compared to other methods.
Application Scenarios and Customization
Organic fertilizer pneumatic conveying systems are widely used in various applications, including large-scale agricultural operations, composting facilities, and organic waste processing plants. In agricultural settings, these systems facilitate the distribution of compost and manure to fields, ensuring even application and optimal nutrient distribution. Composting facilities benefit from efficient material transfer between processing stages, such as mixing, aerating, and screening. The flexibility of the system allows for customization based on specific site requirements, including pipeline length, material type, and throughput capacity. For instance, systems can be designed for low-pressure, low-speed conveying for fine materials like compost, or high-pressure, high-speed conveying for bulkier materials like manure.
Company Profile: Shandong HeadPowder Engineering Co., Ltd.
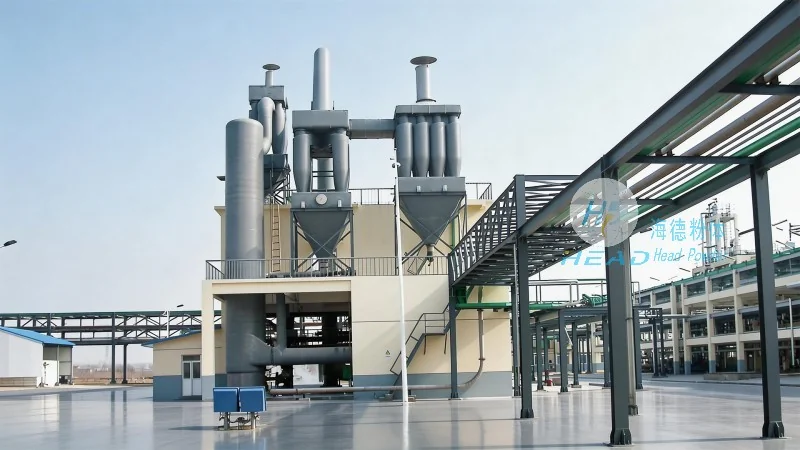
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a leading provider of specialized engineering solutions for material handling and processing. With a focus on innovation and customer-centric design, the company has established itself as a trusted partner in the agricultural and industrial sectors. HeadPowder specializes in the design, manufacturing, and installation of organic fertilizer pneumatic conveying systems, leveraging advanced technology and extensive industry experience to deliver high-quality solutions. The company's headquarters is located in Shandong, China, where it operates a state-of-the-art facility dedicated to research, development, and production.




