For industries dealing with potassium sulfate, a specialized type of bulk material handling system is often essential: the potassium sulfate powder conveying line. This system is engineered to efficiently transport potassium sulfate, a crucial fertilizer and industrial chemical, from storage to processing or packaging areas. The design of such a line is critical, as it must ensure reliable, low-dust, and energy-efficient operation while maintaining product integrity. In this article, we explore the fundamental aspects of potassium sulfate powder conveying lines, focusing on their design principles and key components.
Key Components of a Potassium Sulfate Powder Conveying Line
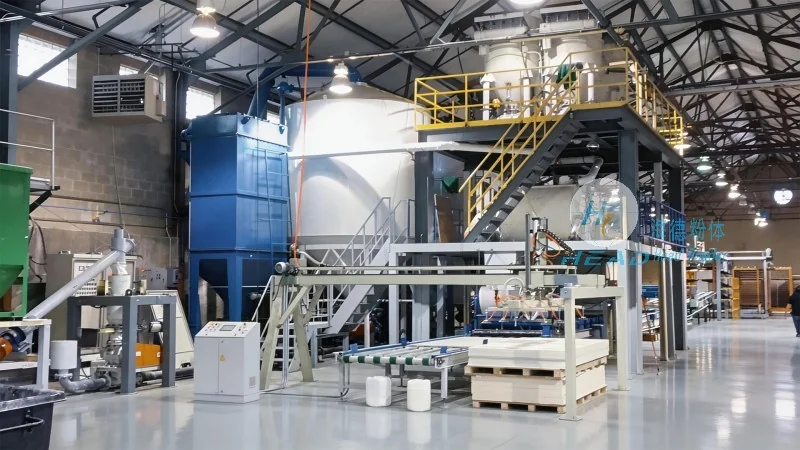
The core of any potassium sulfate powder conveying line consists of several interconnected components, each playing a vital role in the overall system. The primary elements include a hopper for material storage, a feeder to control the flow rate, a conveyor (such as a screw or pneumatic conveyor) to transport the powder, and a dust collection system to maintain air quality. The hopper is typically designed with a conical or rectangular shape to prevent material bridging and ensure smooth discharge. The feeder, often a rotary valve or a vibratory feeder, regulates the flow of potassium sulfate, preventing overloading or underflow. The conveyor system, chosen based on the material's properties and the required distance, can be either mechanical (e.g., screw conveyors) or pneumatic (e.g., air slides). Pneumatic systems are particularly effective for fine powders like potassium sulfate, as they minimize dust generation and provide gentle handling. Finally, the dust collection system, usually an air filter or cyclone, captures any airborne particles, ensuring compliance with environmental regulations and maintaining a safe working environment.
Design Principles for Optimal Performance
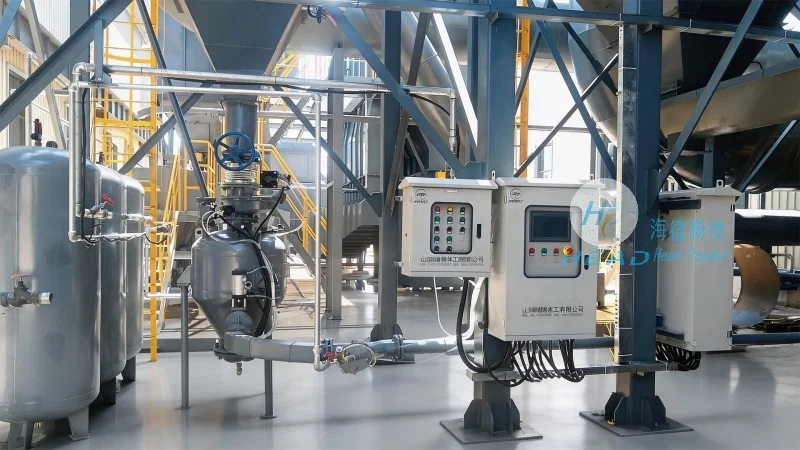
The design of a potassium sulfate powder conveying line is guided by several key principles to achieve efficiency, reliability, and safety. First, the system must be tailored to the specific characteristics of potassium sulfate, including its particle size, density, and flowability. For example, if the powder is fine and prone to caking, the hopper and feeder may need special anti-caking measures, such as heating or vibration. Second, the conveyor must be sized appropriately to handle the required throughput without causing excessive pressure drops or energy consumption. This involves selecting the right diameter for screw conveyors or the correct air velocity for pneumatic systems. Third, dust control is a critical design consideration. Potassium sulfate is a fine powder that can generate significant dust during handling, which poses health risks and environmental concerns. Therefore, the system incorporates robust dust collection and filtration equipment to capture and neutralize airborne particles. Fourth, the overall layout of the conveying line should minimize the number of bends and changes in direction, as these can cause material degradation or blockages. Smooth, gradual transitions between components help maintain the integrity of the powder and reduce maintenance requirements. Finally, the system is designed with safety in mind, incorporating features such as emergency shut-off valves, pressure relief devices, and proper grounding to prevent accidents and ensure compliance with industrial safety standards.
Application and Benefits in Industrial Settings
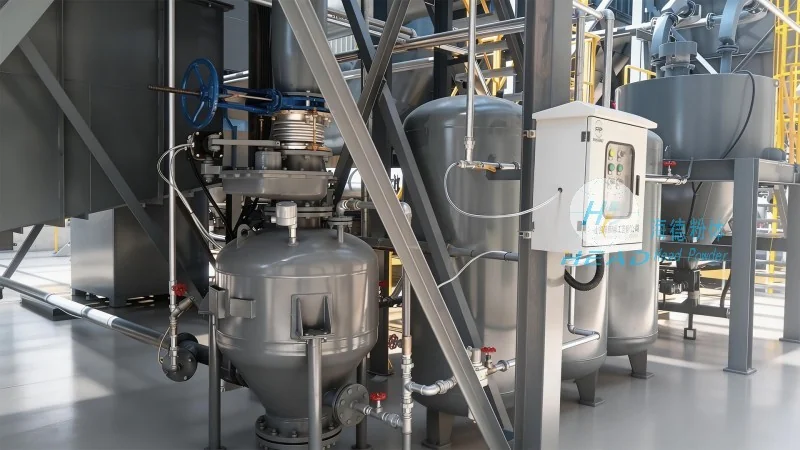
Potassium sulfate powder conveying lines are widely used in various industrial applications, particularly in the fertilizer and chemical industries. They are essential for moving potassium sulfate from storage silos to processing facilities, where it may be blended with other nutrients or converted into other products. In the fertilizer industry, these systems ensure that potassium sulfate is delivered to packaging lines efficiently, maintaining product quality and reducing downtime. The benefits of using a specialized conveying line for potassium sulfate include improved operational efficiency, reduced labor costs, and enhanced safety. By automating the material handling process, the system minimizes the need for manual handling, which is both labor-intensive and risky. Additionally, the low-dust design of the system helps maintain a clean working environment, reducing the risk of respiratory issues for workers. The energy efficiency of modern conveying systems also contributes to cost savings, as they operate with minimal power consumption compared to older, less efficient methods. Overall, a well-designed potassium sulfate powder conveying line is a critical investment for any facility handling this valuable material, providing reliable performance and long-term benefits.
Conclusion: The Importance of Professional Design and Implementation
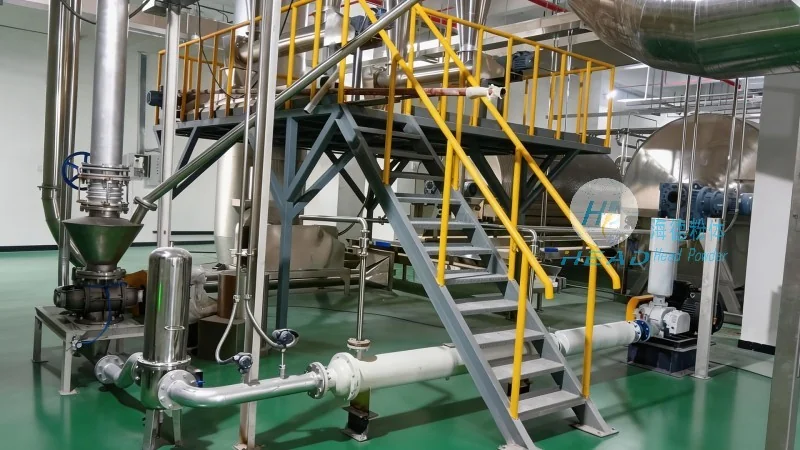
Designing and implementing a potassium sulfate powder conveying line requires expertise and attention to detail, as the system must balance efficiency, safety, and product integrity. Companies like Shandong HeadPowder Engineering Co., Ltd., a leading provider of bulk material handling solutions in China, offer tailored solutions that meet the specific needs of each client. With a focus on innovation and quality, HeadPowder ensures that their systems meet the highest standards of performance and safety. By leveraging their expertise in material flow dynamics and dust control, they deliver reliable solutions that enhance operational efficiency and reduce downtime. The company's headquarters is located in Shandong, China, where they have established a strong presence in the industrial equipment sector. Their commitment to customer satisfaction and technical excellence has made them a trusted partner for businesses in the fertilizer and chemical industries, helping them optimize their material handling processes and achieve their production goals.




