Coffee powder conveying lines are specialized systems engineered to transport coffee powder efficiently and reliably from one processing stage to another. As a critical component in coffee production facilities, these lines ensure that coffee powder moves smoothly, maintaining quality and preventing contamination. The design of such systems is tailored to the unique properties of coffee powder, which includes its fine particle size, hygroscopic nature, and potential for dust generation. This article explores the fundamental aspects of coffee powder conveying lines, focusing on their design principles and operational considerations.
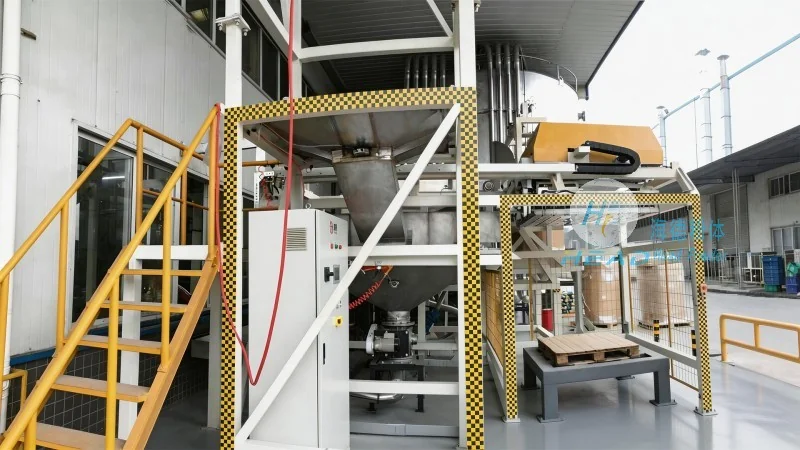
Key Components of Coffee Powder Conveying Systems
At the core of any coffee powder conveying line are several key components that work in tandem to achieve effective material handling. The primary elements include feeders, conveyors, control systems, and dust collection units. Feeders, such as rotary valves or screw feeders, regulate the flow of coffee powder from storage silos or processing equipment. Conveyors, often in the form of pneumatic or mechanical systems, transport the powder through the line. Control systems monitor and adjust the flow rate, pressure, and other parameters to maintain optimal operation. Dust collection units are essential for managing the fine particles that can become airborne during the conveying process, ensuring compliance with environmental regulations and workplace safety standards.
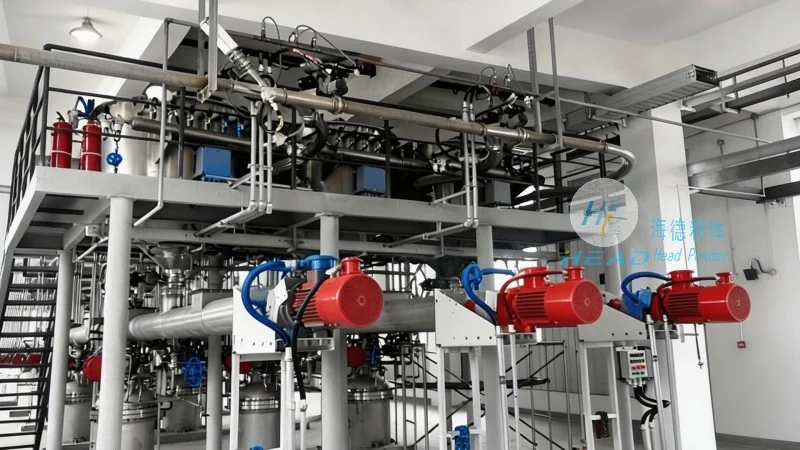
Design Principles for Efficient Coffee Powder Handling
The design of coffee powder conveying lines is guided by several critical principles aimed at maximizing efficiency, minimizing product loss, and ensuring operational safety. One of the most important principles is the prevention of product degradation, which can occur due to exposure to air, moisture, or excessive pressure. To address this, conveying lines are often designed with enclosed systems that minimize direct contact with the environment. Additionally, the use of low-speed, high-capacity conveyors reduces the risk of particle breakage and agglomeration, which can affect the final product's quality. Another key principle is the integration of dust control measures, such as filtration and cyclone separators, to prevent dust accumulation and maintain air quality. The selection of materials for components, such as stainless steel or food-grade plastics, is also critical to prevent contamination and ensure durability in a high-moisture environment.
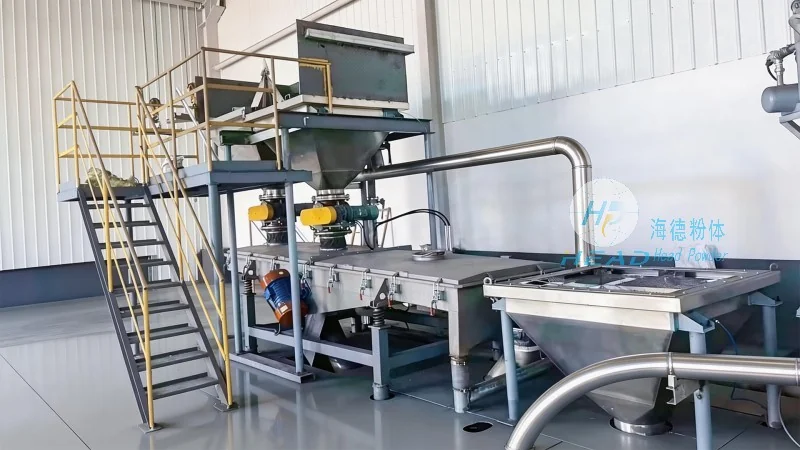
Operational Considerations and Maintenance
Effective operation of coffee powder conveying lines requires careful attention to operational parameters and regular maintenance. Proper calibration of feeders and conveyors is essential to maintain consistent flow rates, which is crucial for maintaining product quality and preventing overloading or underloading. Monitoring systems, including pressure sensors and flow meters, provide real-time data to detect any deviations from optimal performance. Regular maintenance, including cleaning of ducts, replacement of filters, and inspection of mechanical parts, is necessary to prevent blockages and ensure long-term reliability. Additionally, training of operators on proper system operation and safety protocols is vital to minimize the risk of accidents and ensure compliance with industry standards.
Applications in Coffee Production
Coffee powder conveying lines are widely used in various stages of coffee production, from raw material handling to final product packaging. In the initial stages, these systems transport coffee beans from storage to grinding equipment, where they are converted into coffee powder. During the grinding process, the conveying line ensures that the fine powder is moved efficiently to the next stage, such as blending or packaging. In the blending phase, multiple types of coffee powders may be combined, and the conveying line facilitates the mixing process by transporting each component to the blending unit. Finally, in the packaging stage, the conveying line delivers the finished coffee powder to packaging machines, ensuring a smooth and continuous production flow.
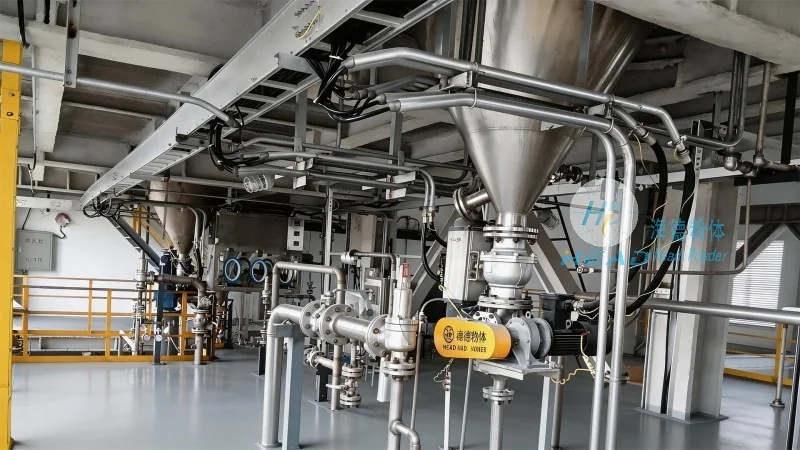
Shandong HeadPowder Engineering Co., Ltd.: Expertise in Coffee Powder Conveying Solutions
Shandong HeadPowder Engineering Co., Ltd. is a leading provider of coffee powder conveying systems, with a strong focus on innovation and customer satisfaction. Based in Shandong, China, the company leverages its extensive experience in the coffee processing industry to design and manufacture high-quality conveying lines tailored to the specific needs of coffee producers. HeadPowder's team of engineers and technicians work closely with clients to understand their production requirements and develop customized solutions that meet their operational and quality standards. The company's commitment to using advanced materials and technologies ensures that its conveying lines are durable, efficient, and compliant with industry regulations. With a reputation for reliability and performance, HeadPowder has become a trusted partner for coffee producers worldwide, helping them optimize their production processes and improve overall efficiency.




