HeadPowder, or Shandong HeadPowder Engineering Co., Ltd., is a professional manufacturer specializing in the design and production of material handling systems for rare earth powders. Our company is located in Shandong, China, and has been committed to providing high-quality solutions for the efficient and safe transportation of rare earth powders in various industrial applications.
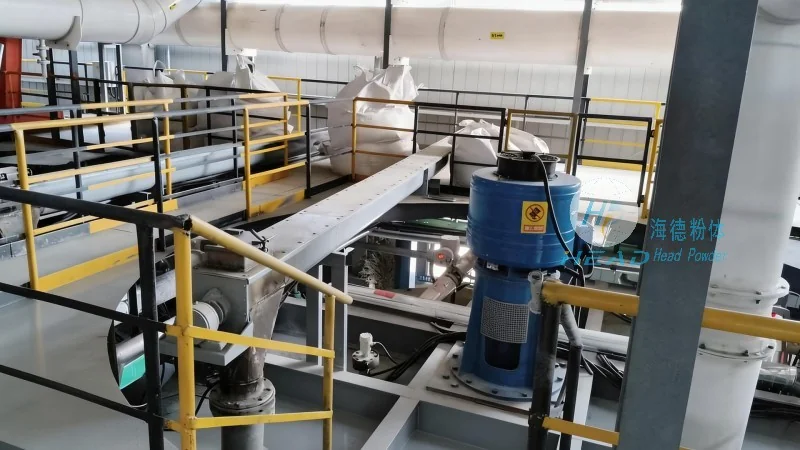
What is a Rare Earth Powder Material Handling System?
A rare earth powder material handling system is a specialized equipment setup designed to transport, store, and manage rare earth powders efficiently. These systems are crucial in industries such as metallurgy, electronics, and new energy, where the handling of rare earth powders requires precision and safety due to their unique chemical and physical properties. The system typically includes components like hoppers, conveyors, feeding devices, and control systems, all working in tandem to ensure the smooth and controlled movement of the powder material from one point to another.
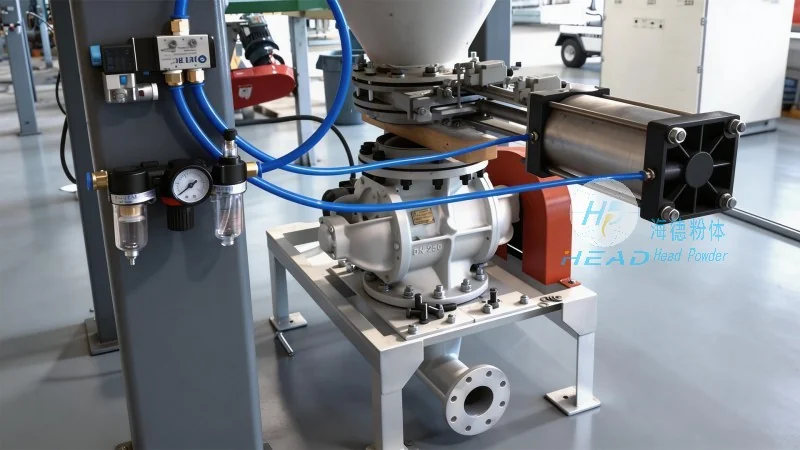
Design Principles of Rare Earth Powder Material Handling Systems
The design of a rare earth powder material handling system follows several key principles to ensure optimal performance, safety, and efficiency. First, the system must consider the hygroscopic and reactive nature of rare earth powders. This means that the equipment is often constructed with materials that are resistant to corrosion and moisture, such as stainless steel or special alloys, to prevent contamination and degradation of the powder. Second, the design emphasizes dust control and explosion prevention. Rare earth powders can be combustible under certain conditions, so the system incorporates explosion-proof components, dust collection systems, and proper ventilation to minimize fire and explosion risks. Third, the system is designed for minimal particle loss and contamination. This involves using sealed hoppers, enclosed conveyors, and precise feeding mechanisms to maintain the purity of the powder and prevent cross-contamination with other materials. Fourth, the design prioritizes ease of maintenance and cleaning. The components are designed to be easily accessible for inspection and cleaning, reducing downtime and ensuring long-term reliability. Finally, the system is tailored to meet specific production requirements, including the volume of material to be handled, the distance of transportation, and the required speed of operation. By adhering to these design principles, the rare earth powder material handling system can effectively meet the demands of modern industrial processes while ensuring safety and efficiency.
Key Components and Their Functions
The effectiveness of a rare earth powder material handling system relies on the integration of several key components, each with a specific function. The hopper is the primary container for storing the powder, typically designed with a conical or rectangular shape to facilitate uniform feeding. The feeding device, often a rotary valve or a screw feeder, regulates the flow of powder from the hopper into the conveyor system. The conveyor, which can be a belt conveyor, screw conveyor, or pneumatic conveyor, transports the powder to the desired location. The control system monitors and adjusts the operation of the components, ensuring smooth and consistent material flow. Additionally, the system may include dust collection equipment to capture and filter airborne particles, and a safety system to detect and mitigate potential hazards such as overfilling or blockages.
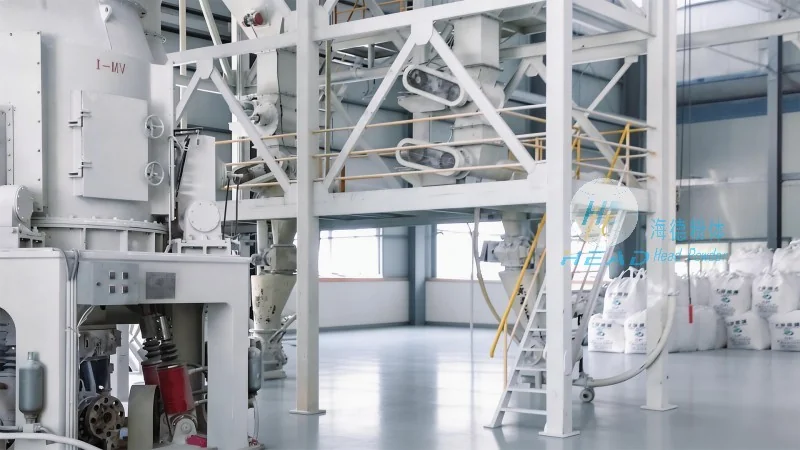
Advantages of Using a Professional Material Handling System
Implementing a professional rare earth powder material handling system offers numerous advantages for industrial operations. Firstly, it enhances operational efficiency by automating the material handling process, reducing the need for manual labor and minimizing the risk of human error. Secondly, it improves safety by controlling dust and preventing accidents, which is critical given the hazardous nature of rare earth powders. Thirdly, it maintains the quality of the powder by preventing contamination and loss, which is essential for downstream processes. Fourthly, it reduces maintenance costs and downtime by using durable and well-designed components. Finally, it provides flexibility to adapt to changing production needs, allowing for scalability and customization of the system. Overall, a well-designed rare earth powder material handling system is a vital investment for industries that rely on the consistent and safe handling of rare earth powders.




