Understanding the design principles and functionality of a sodium stearate material handling system is crucial for industries that rely on this chemical for various applications. This system is engineered to efficiently transport sodium stearate, a widely used surfactant and emulsifier, from storage to processing units. The system's design considers the physical and chemical properties of sodium stearate, such as its solid form at room temperature and its tendency to agglomerate, to ensure smooth and reliable operation.
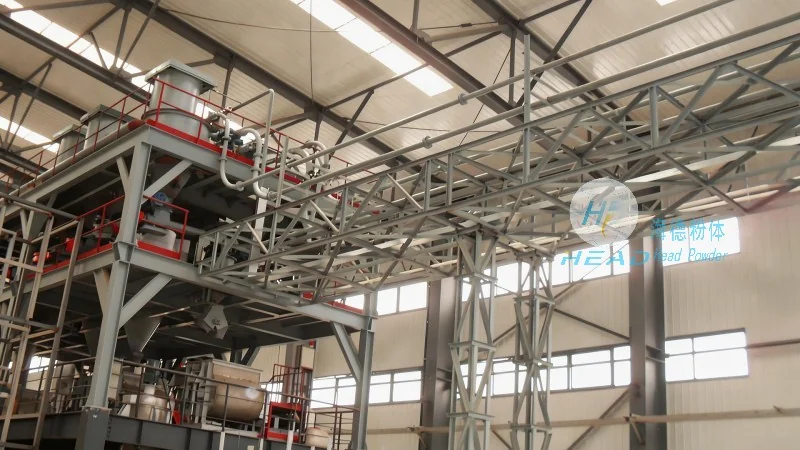
Components of a Sodium Stearate Material Handling System
A typical sodium stearate material handling system consists of several key components that work in tandem to facilitate the movement of the material. These components include bulk storage silos or hoppers, conveying equipment like screw conveyors or pneumatic systems, feeding mechanisms, and control systems. The storage silos are designed to hold large quantities of sodium stearate, ensuring a steady supply for processing. The conveying equipment is selected based on the material's characteristics, such as its density and flowability, to prevent blockages and ensure consistent flow rates.
Design Principles for Efficient Material Handling
The design of a sodium stearate material handling system follows several fundamental principles to maximize efficiency and minimize downtime. One key principle is the consideration of the material's flow properties. Sodium stearate, when stored in bulk, can form lumps or agglomerates, which may impede the smooth movement through conveying systems. Therefore, the system incorporates features like agitators or vibrators in the storage silos to break up agglomerates and maintain a free-flowing condition. Additionally, the system may include pre-drying or pre-heating steps to adjust the moisture content and temperature of the material, as these factors can significantly affect its flowability.
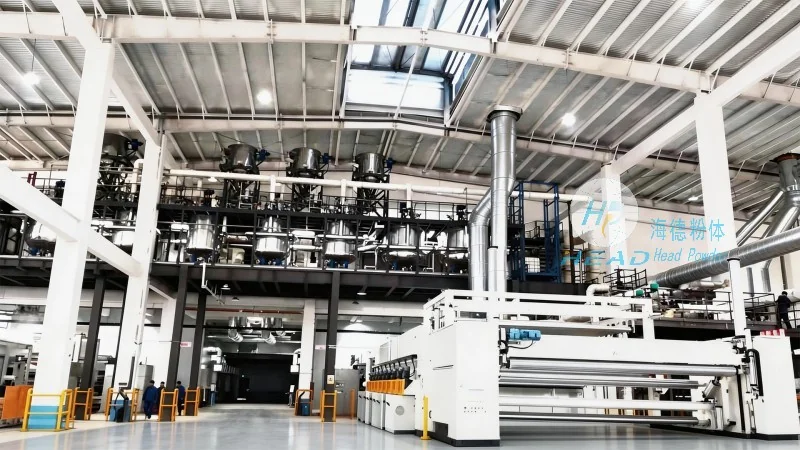
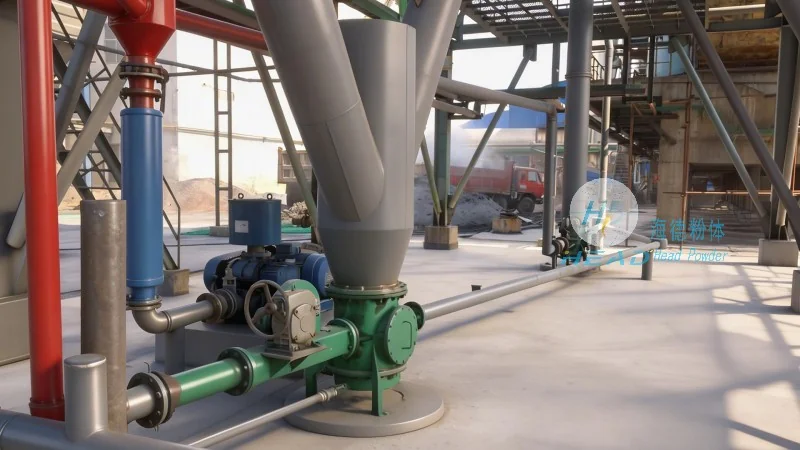
Another critical design principle is the selection of appropriate conveying equipment. Screw conveyors are commonly used for horizontal or slight incline transport due to their ability to handle bulk solids without the need for external power sources beyond the motor. However, for vertical or longer horizontal distances, pneumatic conveying systems may be employed. These systems use air pressure to move the material through pipes, which is particularly effective for handling fine powders like sodium stearate, as it reduces the risk of material degradation and contamination.
Control and Monitoring Systems
Modern sodium stearate material handling systems are equipped with advanced control and monitoring systems to ensure optimal performance and safety. These systems typically include level sensors in the storage silos to detect the material level and trigger feeding when the level drops below a certain threshold. Flow meters are installed in the conveying lines to monitor the flow rate and adjust the speed of the conveying equipment as needed. Additionally, temperature and humidity sensors may be integrated to maintain the material's quality during transport, as variations in these parameters can affect its chemical properties and usability.
Application-Specific Considerations
The design of a sodium stearate material handling system may also need to consider the specific application of the material. For example, in the production of detergents or cosmetics, the system may need to integrate with other processing equipment, such as mixers or reactors, to ensure a seamless flow of the material into the next stage of production. The system may also need to comply with industry standards and regulations regarding material handling, such as those related to safety and environmental protection.
About Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a leading provider of material handling solutions for various chemical industries. With a focus on innovation and customer satisfaction, HeadPowder designs and manufactures systems tailored to the unique needs of its clients. The company's expertise in handling specialty chemicals like sodium stearate has enabled it to serve a wide range of industries, including personal care, pharmaceuticals, and food processing. HeadPowder's commitment to quality and reliability has made it a trusted partner for businesses seeking efficient and reliable material handling systems.
Located in Shandong, China, HeadPowder leverages its local presence and extensive industry knowledge to deliver comprehensive solutions that meet the evolving demands of the market. The company's team of engineers and technicians work closely with clients to understand their specific requirements and develop customized systems that enhance productivity and reduce operational costs. By combining advanced technology with practical experience, HeadPowder ensures that its material handling systems are not only efficient but also safe and environmentally friendly.




