When it comes to handling and conveying feed materials in industries such as pharmaceuticals, food processing, and chemical manufacturing, maintaining a clean and contamination-free environment is paramount. This is where dust-free feed material handling equipment plays a crucial role. These specialized systems are engineered to transport bulk materials while minimizing dust generation and ensuring compliance with stringent hygiene standards. In this article, we will explore what these equipment systems are and delve into the fundamental design principles that underpin their functionality.
Understanding Dust-Free Feed Material Handling Equipment
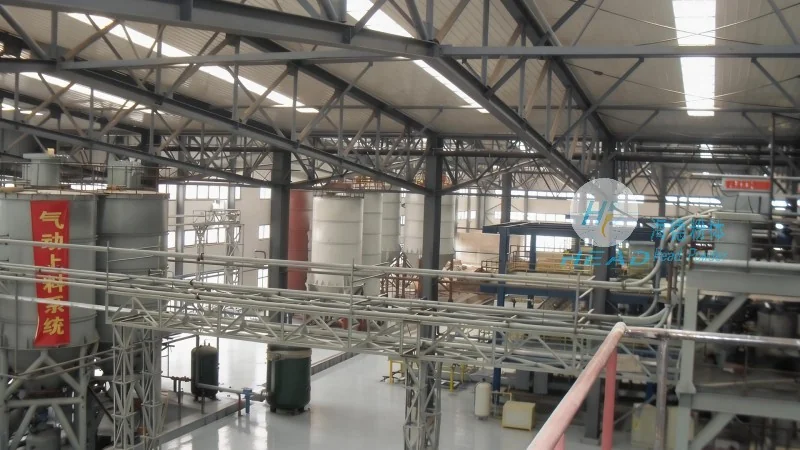
At its core, dust-free feed material handling equipment is a sophisticated system designed to move bulk feed materials from one location to another without releasing dust or particles into the surrounding environment. These systems are typically used in applications where material purity and product safety are critical. The equipment often includes components such as feed hoppers, conveyors, and dust collection systems, all integrated to ensure a seamless and clean material transfer process.
Key Components and Functions
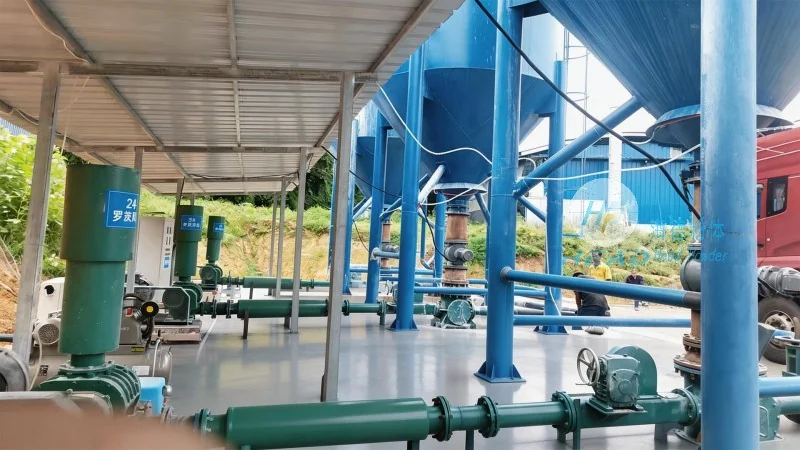
The effectiveness of dust-free feed material handling equipment relies on several key components that work in concert to achieve its primary objectives. First, the feed hopper is designed to store and feed the bulk material into the conveying system. It often features a sealed design to prevent dust from escaping and to maintain material integrity. Next, the conveying mechanism—such as screw conveyors, pneumatic conveyors, or belt conveyors—transports the material through a sealed pipeline. This ensures that the material remains contained and does not come into contact with the external environment. Finally, the dust collection system, which may include filters or cyclones, captures any airborne particles that might be generated during the process, further enhancing the overall cleanliness of the operation.
Design Principles for Optimal Performance
The design of dust-free feed material handling equipment is guided by several critical principles aimed at maximizing efficiency, safety, and compliance. One of the most important principles is the implementation of a fully enclosed system. By enclosing all material pathways and transfer points, the equipment minimizes the risk of dust leakage and cross-contamination. This is particularly vital in industries where product quality and regulatory standards are non-negotiable. Another key principle is the selection of appropriate materials for construction. Components such as hoppers, conveyors, and pipelines are often made from stainless steel or other corrosion-resistant materials to withstand the abrasive nature of feed materials and to maintain hygiene standards. Additionally, the design incorporates features that facilitate easy cleaning and maintenance, ensuring that the equipment remains in optimal condition over time.
Sealing and Containment Mechanisms
A critical aspect of dust-free feed material handling equipment is the sealing technology employed to prevent dust from escaping. Sealing mechanisms such as O-rings, gaskets, and clamped connections are used at all joints and connections to create a tight seal. In some advanced systems, dynamic seals are employed to accommodate movement and vibrations without compromising the seal integrity. The use of airtight enclosures and pressure differentials also contributes to maintaining a controlled environment within the system. For instance, maintaining a slight negative pressure inside the conveying line can help prevent dust from escaping into the ambient air. These sealing strategies are essential for ensuring that the equipment operates within the required cleanliness levels, often specified by industry standards like ISO 14644 or FDA guidelines.
Material Handling Efficiency and Control
Beyond containment, dust-free feed material handling equipment is designed to optimize material flow and control. Variable speed drives are commonly used to adjust the conveyor speed based on the material characteristics and processing requirements. This allows for precise control over the feed rate, preventing overloading or underloading of the system. Additionally, the integration of sensors and control systems enables real-time monitoring of the material level, flow rate, and system performance. This not only enhances operational efficiency but also provides early detection of potential issues, such as blockages or leaks, allowing for timely intervention. The design also considers the need for easy access to maintenance points, ensuring that routine checks and repairs can be performed without disrupting the overall operation.
Application in Various Industries
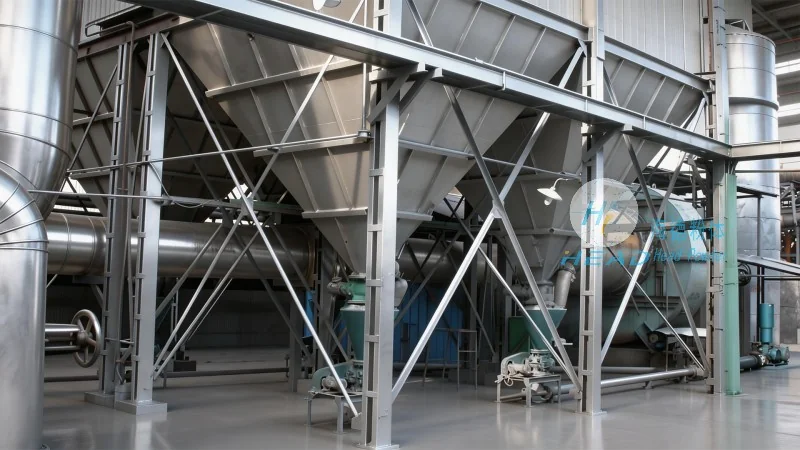
Dust-free feed material handling equipment is widely used across multiple industries due to its ability to handle a diverse range of materials while maintaining high standards of cleanliness. In the pharmaceutical industry, for example, these systems are essential for handling active pharmaceutical ingredients (APIs) and excipients, where even minute amounts of contamination can affect product efficacy and safety. In the food processing sector, they are used to handle ingredients like grains, powders, and spices, ensuring that the final products meet stringent food safety regulations. Similarly, in the chemical manufacturing industry, these equipment systems are crucial for handling raw materials and intermediates, preventing cross-contamination and ensuring product purity.
Conclusion
In conclusion, dust-free feed material handling equipment is a vital component in industries where material purity and environmental safety are paramount. By understanding its design principles and components, businesses can select and implement the most suitable systems to meet their operational needs. The integration of advanced sealing technologies, material handling controls, and monitoring systems ensures that these equipment systems not only enhance productivity but also maintain the highest standards of cleanliness and compliance. As industries continue to evolve and demand stricter regulations, the importance of dust-free feed material handling equipment will only grow, making it an indispensable asset for modern manufacturing processes.




