High-temperature fly ash, a byproduct of coal combustion in thermal power plants, poses significant challenges for efficient and safe handling. The traditional methods of transporting such material often involve complex and costly systems, leading to the adoption of advanced pneumatic conveying technologies. This article explores the working principle and key characteristics of high-temperature fly ash pneumatic conveying, highlighting the technological advancements that enable effective material transport under challenging conditions.
The Working Principle of High-Temperature Fly Ash Pneumatic Conveying
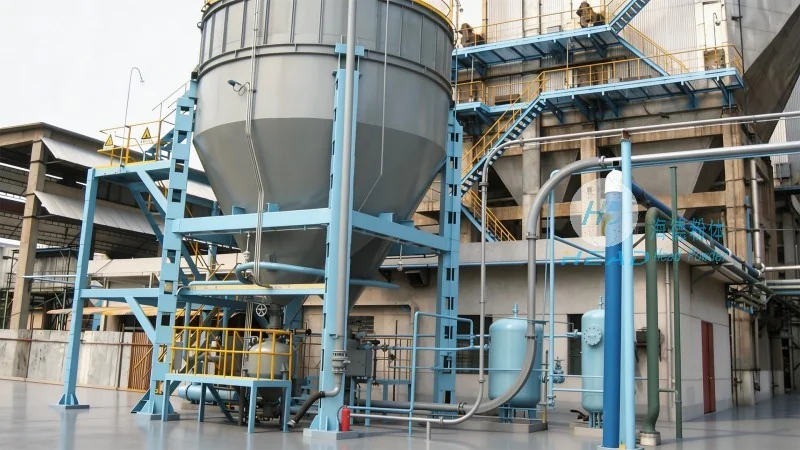
High-temperature fly ash pneumatic conveying systems operate on the principle of using pressurized air or vacuum to move particulate materials through a pipeline. In the case of high-temperature fly ash, the system is designed to handle materials with temperatures up to several hundred degrees Celsius, which requires specialized components to withstand thermal stress and prevent material degradation. The process typically involves the following steps: material feeding, air injection, and transportation through the pipeline. The feed hopper is equipped with a heating element or insulation to maintain the material's temperature, ensuring consistent flow. Air is then introduced into the system, either by a positive displacement blower or a vacuum pump, creating a flow that carries the fly ash particles through the pipeline to the discharge point. The system's design includes temperature-resistant seals, insulated pipelines, and specialized valves to prevent heat loss and material caking, which are critical for maintaining the material's quality and the system's efficiency.
Key Characteristics of High-Temperature Fly Ash Pneumatic Conveying Systems
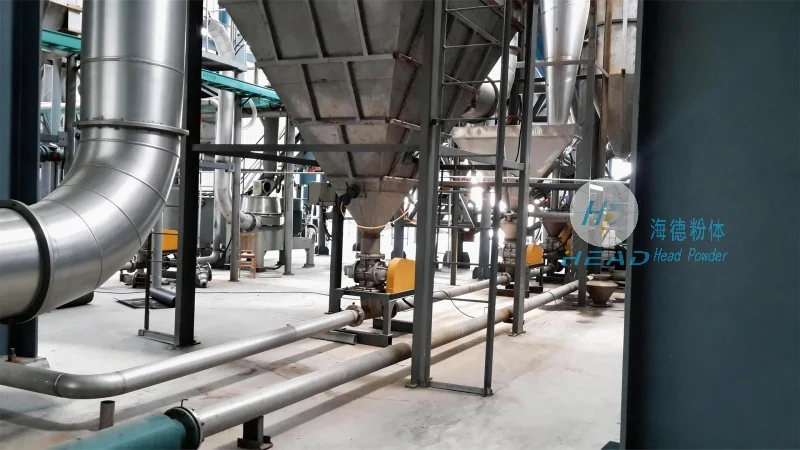
High-temperature fly ash pneumatic conveying systems exhibit several distinct characteristics that make them suitable for industrial applications. Firstly, their ability to handle materials at elevated temperatures is a primary advantage, as it allows for direct transport from the boiler outlet without intermediate cooling steps, which can be energy-intensive and time-consuming. Secondly, the systems are designed for high efficiency, with minimal material loss and low maintenance requirements. The use of positive pressure systems ensures that the material is transported under pressure, reducing the risk of dust emissions and improving safety in industrial environments. Additionally, the systems offer flexibility in terms of pipeline layout, allowing for complex routes that can accommodate the spatial constraints of power plant facilities. Another important characteristic is the system's reliability, which is crucial for continuous operation in power generation plants. The components are engineered to withstand the harsh conditions of high-temperature environments, with materials such as stainless steel and heat-resistant alloys used in critical parts to ensure long-term durability.
Applications and Benefits in Industrial Settings
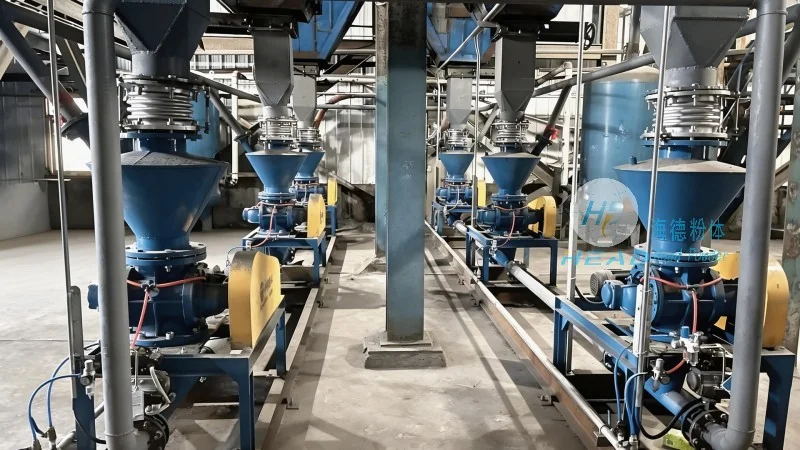
High-temperature fly ash pneumatic conveying systems are widely used in thermal power plants, cement factories, and other industrial facilities where fly ash needs to be transported from the combustion chamber to storage or processing units. The primary benefits of these systems include improved operational efficiency, reduced labor costs, and enhanced safety compared to traditional methods like bucket elevators or conveyor belts. By eliminating the need for manual handling and reducing the risk of dust exposure, the systems contribute to a safer working environment. Furthermore, the systems can be integrated with other processing equipment, such as grinding mills or pelletizing machines, to form a complete material handling line. The ability to handle high-temperature materials directly from the source also minimizes energy losses associated with cooling and re-heating, making the overall process more economical and environmentally friendly.
About Shandong HeadPowder Engineering Co., Ltd.
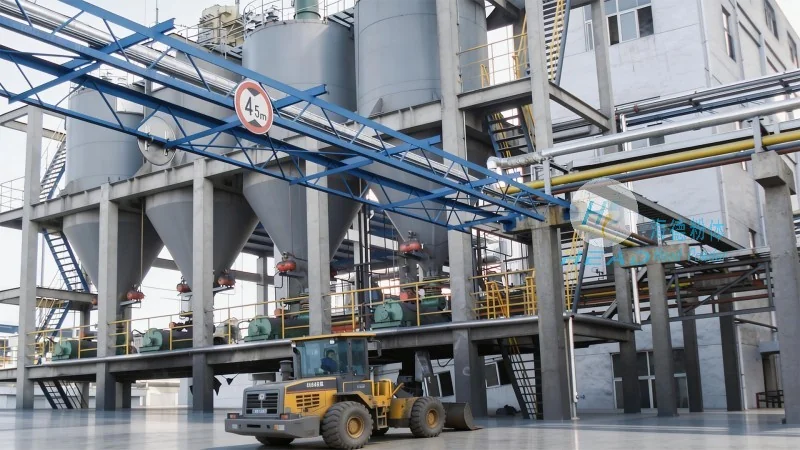
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a leading manufacturer and supplier of advanced material handling solutions, including high-temperature fly ash pneumatic conveying systems. With a strong focus on innovation and quality, the company has developed state-of-the-art technologies to address the unique challenges of transporting high-temperature fly ash. HeadPowder's products are designed to meet the stringent requirements of industrial applications, ensuring reliability, efficiency, and safety. The company's headquarters is located in Shandong, China, where it maintains a comprehensive research and development facility dedicated to improving material handling technologies. HeadPowder's commitment to customer satisfaction and technological excellence has made it a trusted partner for power plants and industrial facilities worldwide.




