Working Principle and Features of Powdered Mineral Air Conveying System Equipment
Release time:2026-09-17 07:17:19
name of the company:Shandong Headpowder Engineering Co., Ltd.
telephone:156-6277-7102
contacts:Zhang manager
Understanding the operation and advantages of powdered mineral air conveying systems is crucial for industries dealing with bulk material handling. These systems are engineered to efficiently transport fine powders and granular materials over long distances using compressed air. The following overview explores the fundamental working principles and distinctive characteristics of such equipment, presented by Shandong HeadPowder Engineering Co., Ltd., a leading manufacturer in the field.
Working Principle of Powdered Mineral Air Conveying Systems
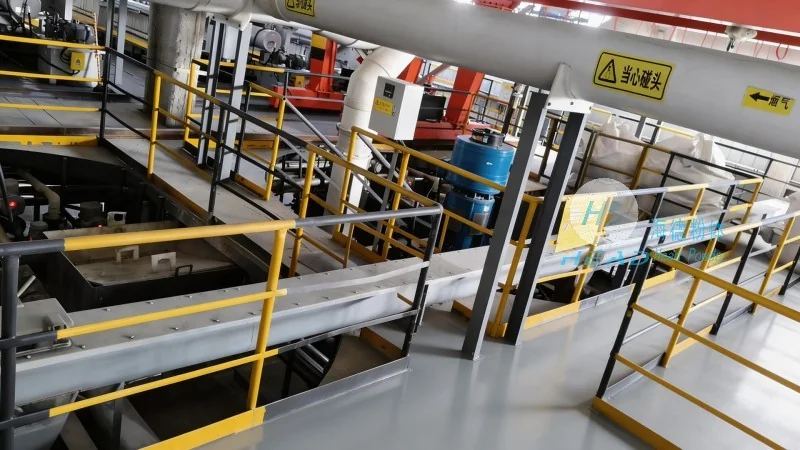
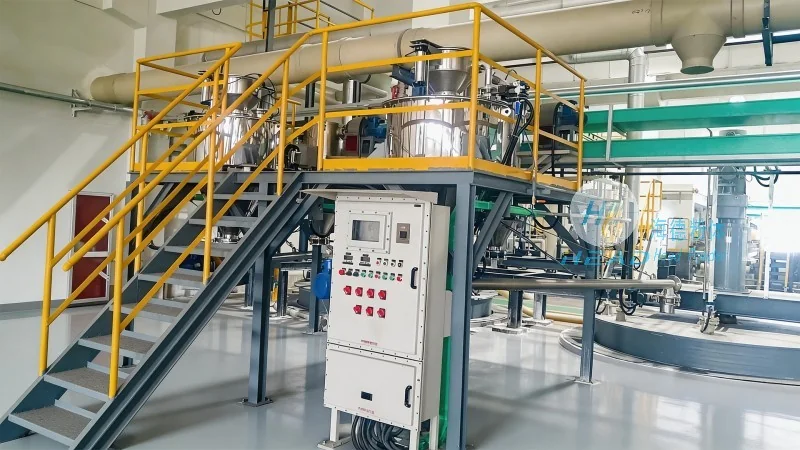
The core mechanism of air conveying systems involves the use of a blower or compressor to generate a high-pressure air stream. This air stream is then directed through a pipeline system where the powdered material is introduced and carried along with the air flow. The system typically operates on the principle of pneumatic transport, where the air velocity is maintained above the material's terminal velocity to ensure stable suspension and efficient movement. The process begins with the material being fed into the inlet of the conveying line, where it is mixed with the air. As the air flows through the pipeline, it transports the material to the discharge point. The system may include components such as a hopper, feeder, and control valves to regulate the flow rate and pressure. The air is then discharged at the receiving end, often through a cyclone separator or filter to separate the material from the air, allowing for clean material collection and air recycling.
Key Features of Powdered Mineral Air Conveying Systems
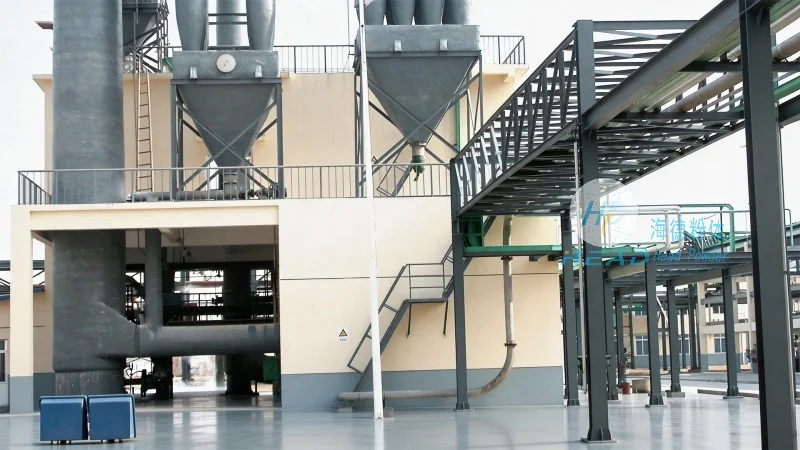
Efficiency and reliability are paramount in the design of powdered mineral air conveying systems. These systems offer several advantages over traditional mechanical conveying methods. Firstly, they provide a dust-free and hygienic environment, which is essential for industries like food processing and pharmaceuticals. The pneumatic transport method minimizes material contamination and reduces the risk of product degradation. Secondly, air conveying systems can handle a wide range of materials, from fine powders to granules, with minimal maintenance requirements. The flexibility in material handling allows for adaptability to various production processes. Additionally, these systems are capable of transporting materials over long distances without the need for multiple transfer points, reducing the overall system complexity and cost. The use of compressed air also enables precise control over the material flow rate, ensuring consistent delivery to downstream processes. Another notable feature is the ability to handle abrasive materials without causing excessive wear on the equipment, as the air acts as a cushioning medium. The systems are also designed for easy integration with existing production lines, making them a cost-effective solution for material transport needs.
Company Profile: Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., operating under the brand name headpowder, is a reputable manufacturer specializing in the design, development, and production of advanced air conveying systems for powdered minerals. With a strong focus on innovation and quality, the company has established itself as a trusted partner in the bulk material handling industry. HeadPowder's products are engineered to meet the stringent requirements of various industrial applications, ensuring high performance and durability. The company's headquarters is located in Shandong, China, where a team of experienced engineers and technicians work diligently to deliver customized solutions tailored to client needs. By leveraging cutting-edge technology and adhering to international standards, HeadPowder provides reliable and efficient air conveying equipment that enhances operational efficiency and reduces downtime for its customers. The company's commitment to customer satisfaction and technical excellence has earned it a solid reputation in the market, making it a preferred choice for businesses seeking advanced material handling solutions.




