The tonne bag quantitative feeding powder material conveying line is a specialized industrial system designed for efficient and precise handling of bulk powders from tonne bags. This equipment is widely used in various industries such as chemical, food, pharmaceutical, and mining, where accurate material transfer and consistent feeding rates are critical for production processes. The system integrates advanced technologies to ensure reliable operation, minimal material loss, and compliance with industry standards.
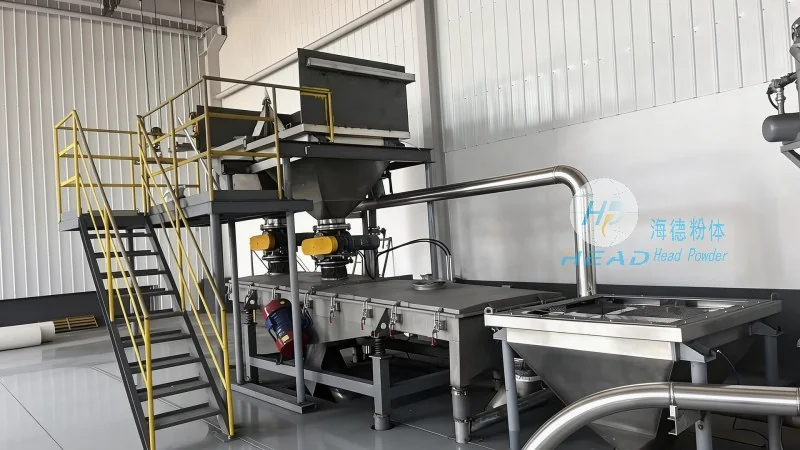
Working Principle of the Tonne Bag Quantitative Feeding Powder Material Conveying Line
The core operational mechanism of the tonne bag quantitative feeding system begins with the secure placement of a tonne bag on a dedicated loading platform. This platform is equipped with a robust lifting and clamping mechanism that firmly holds the bag while simultaneously opening the top seal. Following this, the system activates a vacuum or pressure differential system to draw the bulk powder from the bag into a high-capacity hopper or intermediate storage tank. A precision dosing valve, often a rotary or vibratory feeder, regulates the flow rate of the material, ensuring that the exact target weight is delivered to downstream processing equipment. The entire process is monitored by a network of sensors, including load cells on the hopper to track weight and flow sensors to measure material throughput. This real-time data is fed into a programmable logic controller (PLC), which continuously adjusts the dosing parameters to maintain the set accuracy, typically within ±0.5% of the desired weight. The automation level is high, with minimal human intervention required, enhancing operational efficiency and reducing the risk of human error.
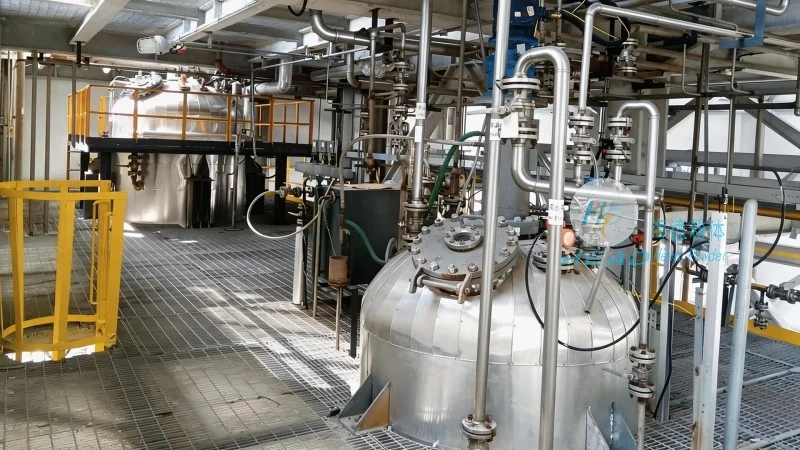
Key Features and Advantages of the Tonne Bag Quantitative Feeding Powder Material Conveying Line
One of the primary features of this system is its high precision in material measurement. The integrated dosing mechanism can achieve accuracy levels within ±0.5% of the set weight, which is crucial for applications such as pharmaceutical manufacturing or food processing where exact dosing is required. Another significant advantage is the system's ability to handle a wide range of powder types, including fine, cohesive, or abrasive materials, without clogging or degradation. The design incorporates dust collection and filtration systems to maintain a clean working environment and prevent product contamination. Additionally, the system is equipped with safety features like overload protection and emergency stop buttons, ensuring safe operation in industrial settings. The modular construction allows for easy integration with existing production lines and facilitates maintenance, reducing downtime and operational costs.
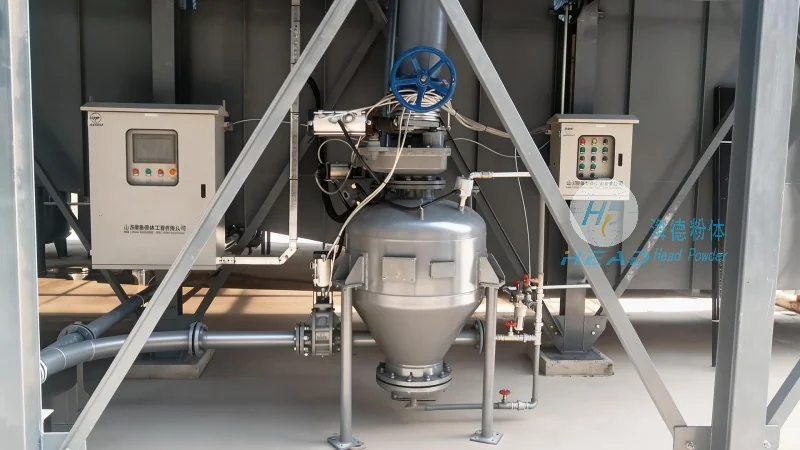
Technical Advantages and Performance Metrics
The tonne bag quantitative feeding powder material conveying line offers several technical advantages that enhance its performance. The use of high-quality materials for the hopper and conveying components ensures durability and resistance to corrosion, especially when handling corrosive or abrasive powders. The system's energy efficiency is another notable feature, with optimized motor control and reduced power consumption during operation. The automation level is high, with minimal manual intervention required, which increases production efficiency and reduces labor costs. The system also provides real-time data on material flow, weight, and operational status, which can be used for process optimization and quality control. The compact design of the equipment allows for installation in limited spaces, making it suitable for both new and retrofit applications.
Application Scenarios and Industry Use Cases
This powder conveying line is particularly suitable for industries that require large-scale handling of bulk powders from tonne bags. In the chemical industry, it is used for transporting raw materials like polymers, pigments, and catalysts to reactors with precise dosing. In the food industry, it ensures accurate feeding of ingredients such as flour, sugar, and spices into processing equipment, maintaining product consistency. The pharmaceutical industry benefits from the system's ability to handle active pharmaceutical ingredients (APIs) with high purity and accuracy, which is essential for drug manufacturing. The mining sector uses the equipment to transport ore concentrates from bulk bags to processing plants, improving operational efficiency and reducing material loss. Overall, the system's versatility and reliability make it a valuable asset for any industry that relies on bulk powder handling.
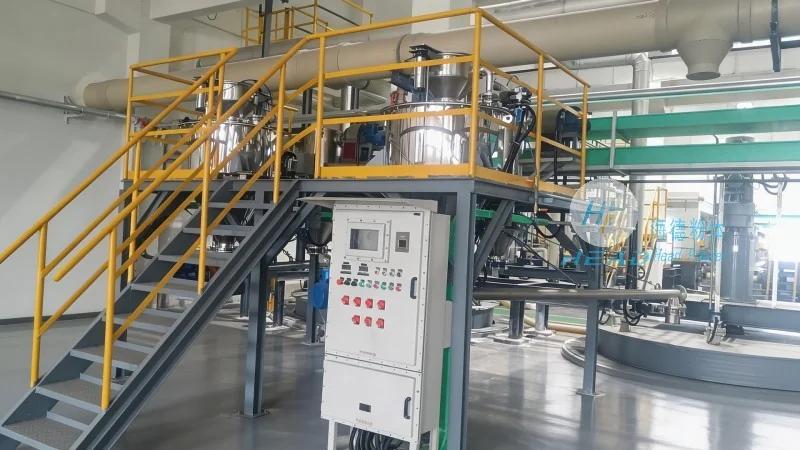
About Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., operating under the brand name headpowder, is a leading manufacturer of specialized powder handling equipment. With a focus on innovation and quality, the company has developed advanced solutions for efficient material transfer and processing. HeadPowder's tonne bag quantitative feeding powder material conveying line is a testament to their commitment to providing reliable and high-performance equipment for industrial applications. The company's products are designed to meet the diverse needs of various industries, ensuring optimal performance and customer satisfaction.




