Positive pressure dilute phase material handling equipment is a specialized system designed for the efficient transport of bulk materials over long distances. This technology is widely used in various industries, including chemical, pharmaceutical, food processing, and mining, where the reliable and safe transfer of powders and granules is critical. The equipment operates by creating a positive pressure environment within the conveying line, ensuring that the material is continuously moved from the source to the destination without the need for external vacuum assistance.
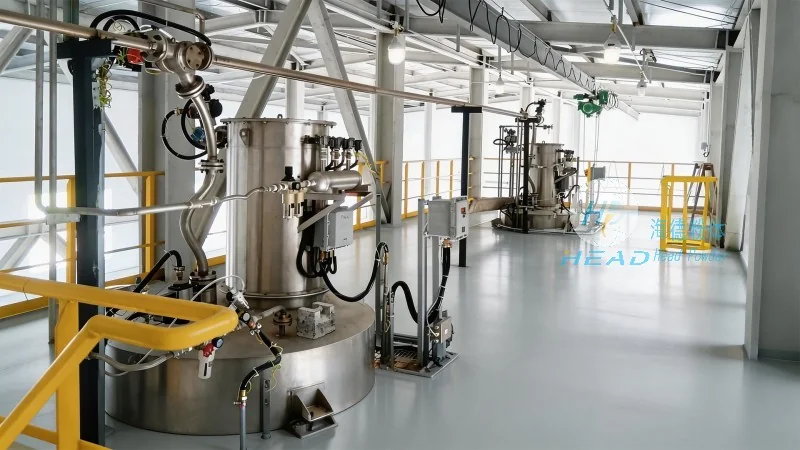
Working Principle of Positive Pressure Dilute Phase Conveying Systems
The core working principle of this equipment involves the use of a positive pressure blower or compressor to generate airflow that propels the material particles through the pipeline. The material is typically fed into the system at the inlet, where it is mixed with the air stream. As the air flows through the pipeline, it carries the material particles forward, maintaining a dilute phase condition—meaning the material is dispersed in the air rather than forming a dense, cohesive flow. This dilute phase ensures minimal pressure drop and efficient energy utilization. The system includes key components such as the air supply unit, material feed hopper, conveying pipeline, and discharge unit. The air supply unit provides the necessary pressure and volume of air, while the feed hopper ensures a consistent material feed rate. The pipeline is designed with appropriate bends and fittings to minimize resistance and maintain the dilute phase. The discharge unit then separates the material from the air, allowing the material to be deposited at the desired location.
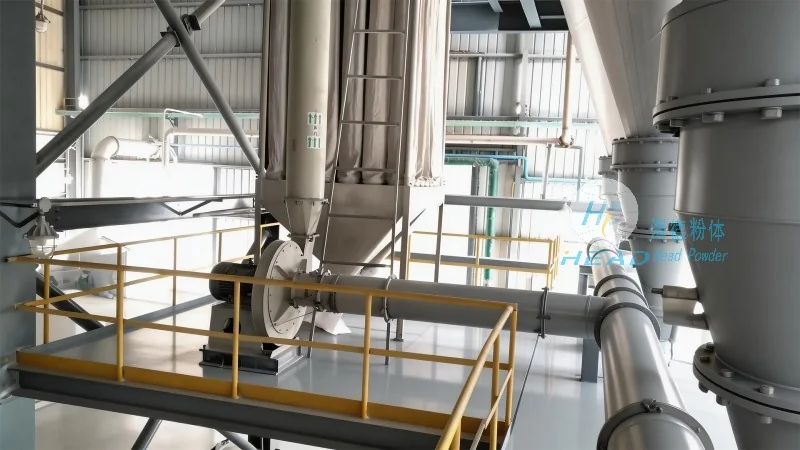
Key Features and Advantages of Positive Pressure Dilute Phase Equipment
Positive pressure dilute phase material handling equipment offers several distinct advantages that make it a preferred choice for many applications. One of the primary features is its ability to handle a wide range of materials, from fine powders to coarse granules, with minimal degradation or segregation. The positive pressure operation ensures that the material is not exposed to negative pressures, which can cause caking or agglomeration in some materials. Another key feature is the high conveying capacity, which allows for the transport of large volumes of material over long distances, often exceeding 100 meters or more. The system is also relatively low in maintenance, as the components are designed for durability and resistance to wear from the material being conveyed. Additionally, the equipment is energy-efficient, as the positive pressure system minimizes energy loss compared to vacuum systems. The dilute phase operation also reduces the risk of blockages and ensures smooth, continuous operation. Furthermore, the system can be easily integrated with other process equipment, such as storage silos or processing units, providing a seamless material flow within the plant.
Applications and Industries Served by Positive Pressure Dilute Phase Systems
Positive pressure dilute phase material handling equipment is applied in various industries where bulk material transport is essential. In the chemical industry, it is used to transport raw materials, intermediates, and finished products, such as powders and granules. The pharmaceutical industry relies on this equipment for the safe and hygienic transfer of active pharmaceutical ingredients (APIs) and other powders, ensuring compliance with GMP (Good Manufacturing Practice) standards. The food processing industry uses it to handle ingredients like flour, sugar, and spices, maintaining product quality and preventing contamination. In the mining and minerals sector, the equipment is used to transport ore and other bulk materials from processing plants to storage or shipping facilities. The system is also utilized in the agricultural industry for the transport of fertilizers and other agricultural products. Each application benefits from the equipment's ability to handle different material characteristics while maintaining efficiency and reliability.
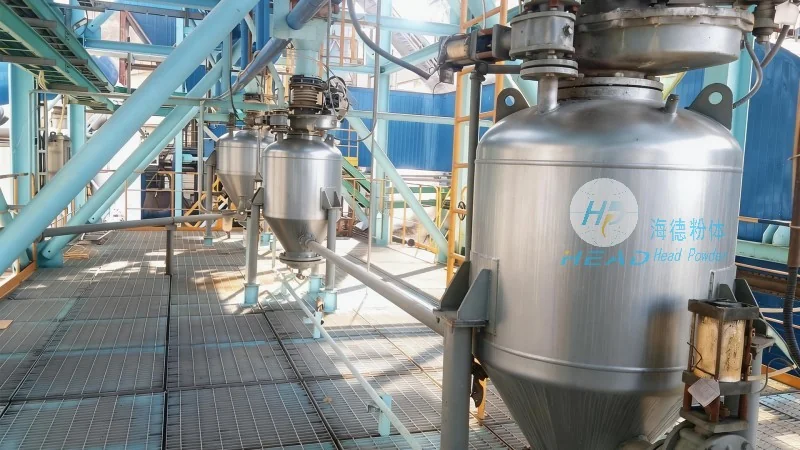
About Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a leading manufacturer and supplier of positive pressure dilute phase material handling equipment. With a strong focus on innovation and quality, the company has established itself as a trusted partner in the material handling industry. HeadPowder's products are designed to meet the specific needs of various industries, offering reliable and efficient solutions for bulk material transport. The company's team of engineers and technicians has extensive experience in designing and manufacturing conveying systems, ensuring that each product is tailored to the customer's requirements. HeadPowder's commitment to customer satisfaction and technical excellence has earned it a reputation for delivering high-quality equipment that meets international standards. The company's headquarters is located in Shandong, China, where it operates a state-of-the-art manufacturing facility equipped with advanced technology and quality control measures. HeadPowder continues to invest in research and development to improve its products and stay at the forefront of the material handling industry.




