For industries dealing with sugar processing, efficient material handling is crucial to maintaining production efficiency and product quality. Pneumatic conveying systems have emerged as a preferred solution for transporting sugar materials due to their ability to handle bulk materials in a clean, controlled manner. This article explores the working principle and key characteristics of pneumatic conveying systems specifically designed for sugar materials, highlighting the technical advantages and practical applications.
Working Principle of Pneumatic Conveying Systems
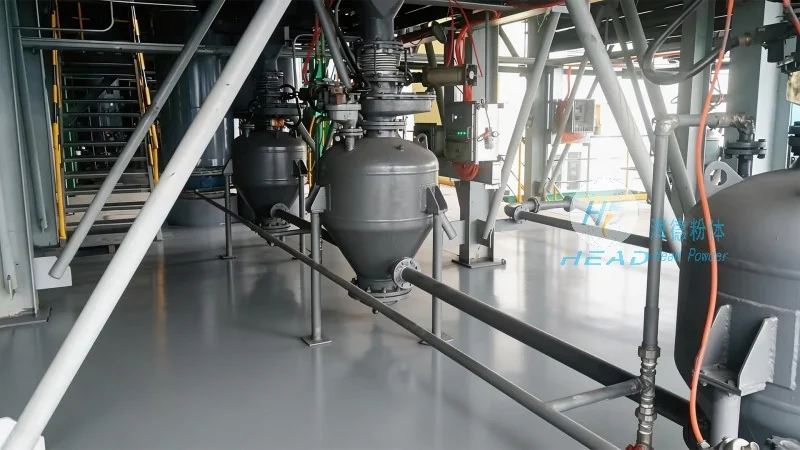
Pneumatic conveying for sugar materials operates on the principle of using air or gas to transport solid particles through a pipeline. The system typically consists of a material feed hopper, a conveying line, and a discharge point. The process begins with the sugar material being introduced into the hopper, where it is then drawn into the conveying line by a vacuum or pressure source. The air flow, either in suction (negative pressure) or pressure (positive pressure) mode, carries the sugar particles along the pipeline. The interaction between the air velocity and the sugar particles determines the conveying efficiency and system performance. In suction systems, a vacuum pump creates a low-pressure environment that pulls the material into the line, while pressure systems use a blower to push the material through the pipeline under positive pressure. The design of the conveying line, including the diameter, length, and bends, is critical to ensure smooth material flow and prevent blockages or degradation of the sugar product.
Key Characteristics of Pneumatic Conveying for Sugar Processing
When considering pneumatic conveying for sugar materials, several key characteristics stand out as advantages. Firstly, the system offers a high degree of cleanliness and hygiene, which is essential for food-grade products like sugar. Unlike mechanical conveyors, which may introduce contaminants or cause product degradation through friction, pneumatic systems minimize direct contact with surfaces, reducing the risk of contamination and maintaining product purity. Secondly, pneumatic conveying provides excellent control over material flow, allowing for precise dosing and regulation of sugar delivery to processing equipment. This is particularly important in sugar refining and blending operations where consistent material feed is critical to product quality. Thirdly, the system is capable of handling a wide range of sugar products, including granulated sugar, powdered sugar, and even sugar syrups, adapting to different particle sizes and moisture contents. The flexibility in material handling makes it suitable for various stages of the sugar production process, from raw material intake to final product packaging.
Application Scenarios and Benefits
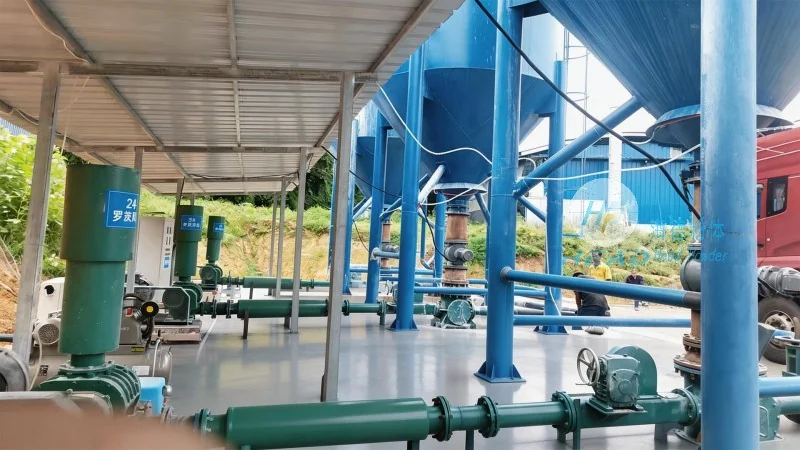
Pneumatic conveying systems are widely used in the sugar industry for several key applications. In raw material handling, they efficiently transport sugar beets or cane into processing facilities, reducing the need for manual labor and improving safety. During the refining process, pneumatic systems are used to convey sugar crystals from one stage to another, such as from the crystallizer to the centrifuge or from the drying oven to the packaging line. In blending operations, the system ensures uniform mixing of different sugar grades or additives, enhancing product consistency. The benefits of using pneumatic conveying for sugar materials extend beyond operational efficiency. The reduced need for manual handling minimizes labor costs and workplace injuries, while the clean and controlled environment improves product quality and reduces waste. Additionally, the system's ability to handle materials in a dust-free manner helps maintain a safe working environment and complies with industry regulations regarding air quality and product purity.
Technical Advantages and Operational Efficiency
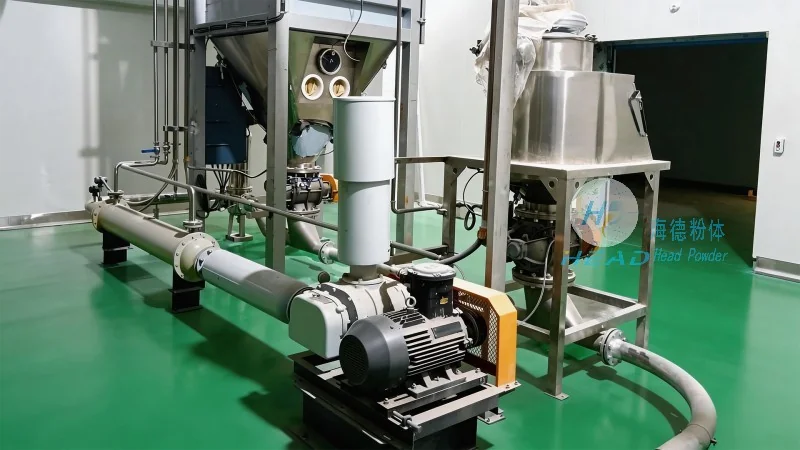
The technical design of pneumatic conveying systems for sugar materials focuses on optimizing performance and reliability. Advanced materials and coatings are used for the conveying lines to prevent corrosion and ensure long service life, especially when handling acidic or moisture-rich sugar products. The system's control mechanisms, including variable speed drives and pressure sensors, allow for real-time monitoring and adjustment of the conveying process, ensuring optimal air flow and material transport. This automation enhances operational efficiency by minimizing downtime and maximizing throughput. Furthermore, the system's compact design and modular components enable easy installation and integration into existing sugar processing facilities, reducing construction time and costs. The energy efficiency of modern pneumatic conveying systems is also a significant advantage, with optimized air flow and reduced pressure drops contributing to lower operational costs over time.
Customization and Integration Capabilities
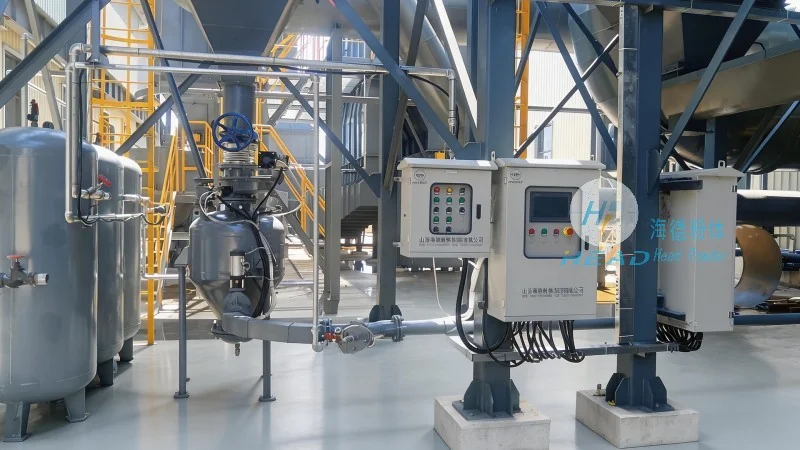
Shandong HeadPowder Engineering Co., Ltd., a leading provider of pneumatic conveying solutions, specializes in designing and manufacturing customized systems tailored to the specific needs of sugar processing facilities. The company's expertise lies in understanding the unique challenges of sugar material handling, such as particle size variations, moisture content, and product purity requirements. By working closely with clients, HeadPowder engineers develop solutions that integrate seamlessly with existing equipment and processes. The company offers a range of options, including suction and pressure conveying systems, as well as hybrid systems that combine the benefits of both. Customization may include specialized hopper designs to handle bulk sugar storage, advanced filtration systems to maintain air quality, and automated control panels for easy operation. HeadPowder's commitment to quality and innovation ensures that their pneumatic conveying systems not only meet but exceed industry standards, providing reliable and efficient material handling for sugar production.
Conclusion and Company Profile
Pneumatic conveying systems represent a sophisticated and effective solution for the transportation of sugar materials in modern processing facilities. By leveraging the principles of air flow and material interaction, these systems offer significant advantages in terms of efficiency, cleanliness, and control. The key characteristics and technical advantages discussed highlight why pneumatic conveying has become the preferred method for sugar handling in the industry. For companies seeking reliable and customized material handling solutions, Shandong HeadPowder Engineering Co., Ltd. stands out as a trusted partner, offering expert design, manufacturing, and integration services. With a focus on quality, innovation, and customer satisfaction, HeadPowder continues to deliver cutting-edge pneumatic conveying systems that enhance operational performance and product quality in the sugar industry. Based in Shandong, China, the company serves clients globally, providing tailored solutions that meet the unique demands of sugar processing operations.




