HeadPowder, a leading manufacturer based in Shandong, China, specializes in the design and production of advanced pneumatic conveying systems tailored for industrial applications. The gray bin pneumatic conveying system is a key product line that integrates efficient material handling solutions with robust engineering. This system is engineered to handle various bulk materials with precision, ensuring smooth and reliable operation in different industrial settings.
The Principle of the Gray Bin Pneumatic Conveying System
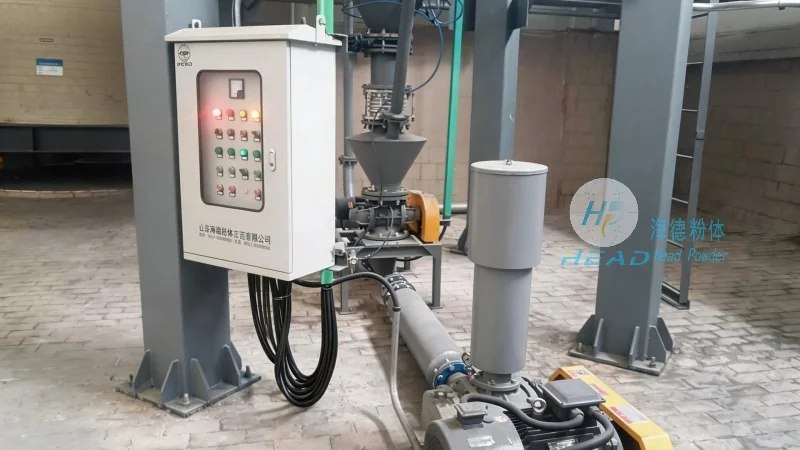
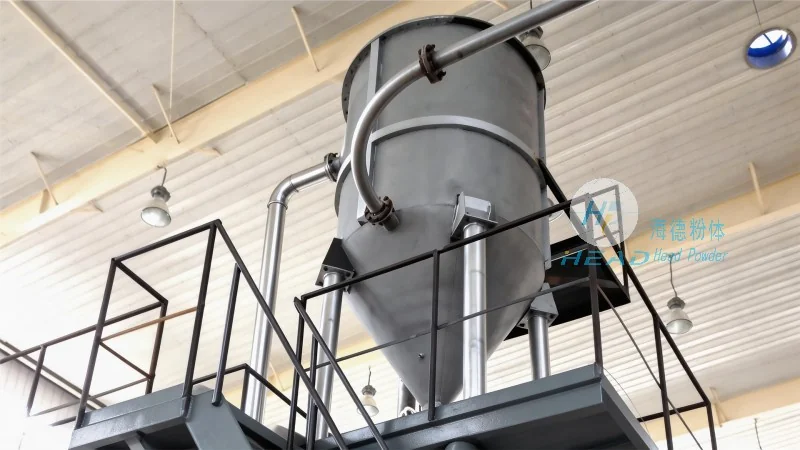
The core principle of the gray bin pneumatic conveying system lies in the use of air as the conveying medium to transport bulk materials from a storage bin to a processing or discharge point. The system operates by creating a pressure differential between the bin and the discharge point, which draws the material into the conveying line. The gray bin itself serves as the primary storage vessel, equipped with a hopper and an airlock mechanism to control material flow and prevent dust leakage. The airlock, typically a rotary or sliding valve, ensures that material is discharged in a controlled manner, maintaining a consistent flow rate. The conveying line, often made of stainless steel or other corrosion-resistant materials, is designed to handle the specific characteristics of the materials being transported, such as particle size, density, and moisture content. The system may utilize positive or negative pressure depending on the application, with positive pressure systems being more common for long-distance or high-capacity conveying. The air compressor, which provides the necessary air pressure, is a critical component that ensures the system operates efficiently and reliably. The control system, which includes sensors and valves, monitors the pressure, flow rate, and material level, allowing for real-time adjustments to maintain optimal performance. This integrated approach ensures that the gray bin pneumatic conveying system can handle a wide range of materials with minimal maintenance and maximum efficiency.
Working Scene Characteristics and Application Scenarios
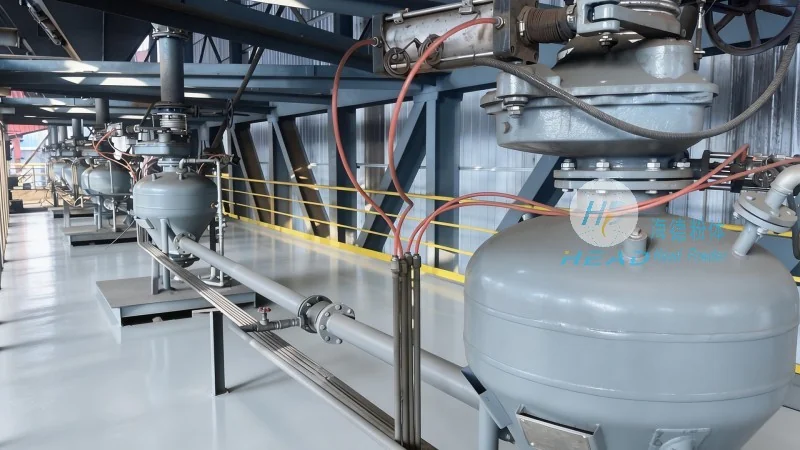
The gray bin pneumatic conveying system is designed to operate in diverse industrial environments, including manufacturing plants, food processing facilities, chemical production sites, and mining operations. Its versatility makes it suitable for handling materials such as powders, granules, and bulk solids. In manufacturing plants, the system is often used to transport raw materials from storage bins to production lines, ensuring a continuous supply of materials without interruptions. The system's ability to handle different particle sizes and densities allows it to be used in food processing facilities, where hygiene and material purity are critical. The chemical industry benefits from the system's corrosion-resistant materials and precise control, enabling the safe handling of hazardous materials. In mining operations, the gray bin pneumatic conveying system is used to transport ore from storage bins to processing equipment, improving operational efficiency and reducing labor costs. The system's compact design and low maintenance requirements make it ideal for applications where space is limited or where frequent maintenance is undesirable. The working scene characteristics of the gray bin pneumatic conveying system include its ability to operate in both indoor and outdoor environments, with the gray bin providing a durable and weather-resistant storage solution. The system's flexibility allows it to be integrated into existing production lines or used as a standalone unit, depending on the specific needs of the application. The control system's user-friendly interface ensures that operators can easily monitor and adjust the system's parameters, enhancing overall operational efficiency. The system's reliability and low downtime make it a preferred choice for industries that require continuous material handling operations, as it minimizes production interruptions and maximizes overall productivity.
Advantages and Key Features of the Gray Bin Pneumatic Conveying System
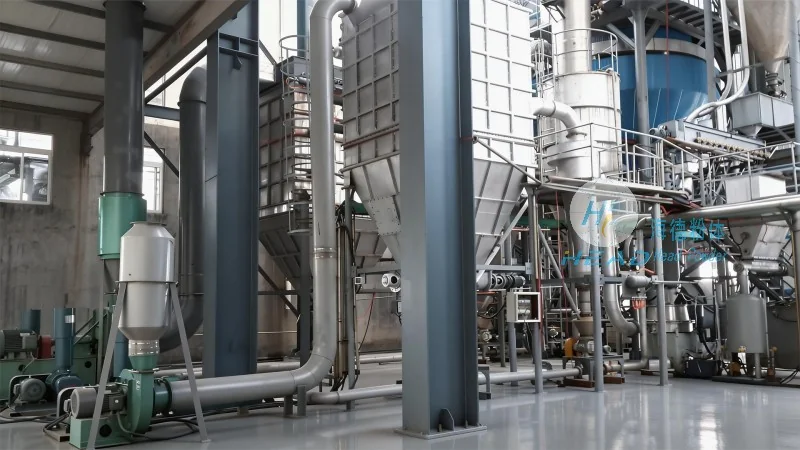
HeadPowder's gray bin pneumatic conveying system offers several advantages that make it a superior choice for industrial material handling. One of the key features is its high conveying efficiency, which allows for the transport of large volumes of material over long distances with minimal energy consumption. The system's ability to handle a wide range of materials, including those with varying particle sizes and moisture content, makes it versatile and adaptable to different applications. The corrosion-resistant materials used in the construction of the system ensure its durability and longevity, reducing the need for frequent replacements or repairs. The system's compact design and low maintenance requirements make it cost-effective and easy to install, even in space-constrained environments. The control system's advanced features, such as real-time monitoring and automatic adjustments, enhance operational efficiency and reduce the risk of material blockages or system failures. The gray bin's design, with its hopper and airlock mechanism, ensures that material flow is controlled and consistent, preventing dust leakage and maintaining a clean working environment. The system's ability to operate under both positive and negative pressure allows for flexibility in different application scenarios, making it suitable for various industrial settings. The use of stainless steel and other high-quality materials in the construction of the conveying line ensures that the system can handle harsh operating conditions, such as high temperatures or corrosive environments. The system's reliability and low downtime make it an essential component for industries that require continuous material handling operations, as it minimizes production interruptions and maximizes overall productivity. The gray bin pneumatic conveying system's integration of advanced engineering and robust construction ensures that it meets the highest standards of performance and safety, making it a trusted solution for industrial material handling needs.




