HeadPowder, a leading provider in the field of bulk powder handling solutions, specializes in advanced systems designed to streamline the process of unpacking and conveying powders. This article delves into the core principles behind intelligent bulk powder unpacking and conveying systems, as well as the specific application scenarios where these technologies offer significant advantages. By understanding the mechanics and operational contexts of such systems, businesses can better evaluate how they can enhance efficiency and reliability in their powder handling operations.
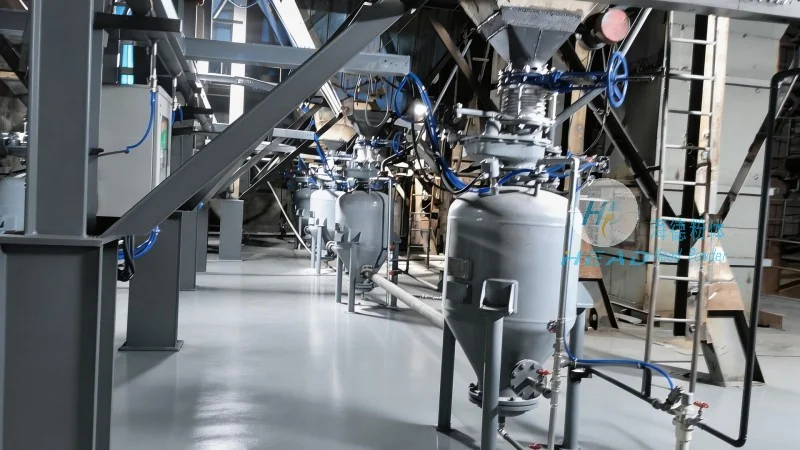
Core Principles of Intelligent Bulk Powder Unpacking and Conveying
The intelligent bulk powder unpacking and conveying system developed by Shandong HeadPowder Engineering Co., Ltd. integrates multiple technologies to achieve seamless material handling. At its heart, the system combines automated unpacking mechanisms with advanced conveying technologies to ensure that powders are transferred from packaging to processing equipment with minimal human intervention. The key principles include:
1. **Automated Unpacking Mechanisms**: The system utilizes precision sensors and actuators to open and empty various types of packaging, such as bags, drums, and containers. This automation reduces the risk of human error and ensures consistent performance across different batches of material.
2. **Integrated Conveying Systems**: Once unpacked, the powder is transferred through a network of conveying components, including screw conveyors, pneumatic systems, or belt conveyors. These systems are designed to maintain the integrity of the powder and prevent segregation or degradation during transport.
3. **Real-Time Monitoring and Control**: Advanced control systems allow operators to monitor the entire process in real-time, adjusting parameters like flow rate, pressure, and temperature as needed. This ensures optimal performance and helps detect any issues promptly.
4. **Modular Design for Flexibility**: The system is built with modular components, enabling easy integration with existing production lines and adaptability to different powder types and packaging formats.
Key Application Scenarios and Operational Benefits
Intelligent bulk powder unpacking and conveying systems are particularly valuable in industries where handling large volumes of powders is critical. The following scenarios highlight the practical applications and benefits of such systems:
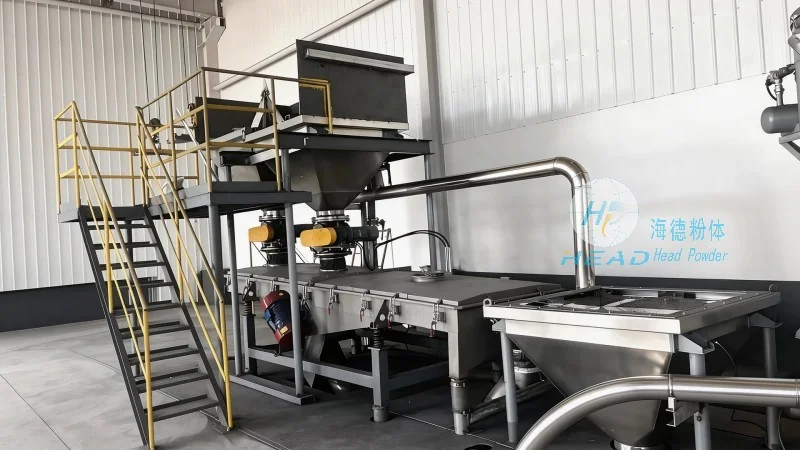
1. **Pharmaceutical Manufacturing**: In pharmaceutical plants, the need for sterile and contamination-free handling is paramount. The intelligent system ensures that powders are transferred without exposure to external contaminants, maintaining compliance with regulatory standards. The automated process also reduces the risk of cross-contamination between batches.
2. **Food Processing Industry**: For food manufacturers, the system helps maintain hygiene and product quality. By eliminating manual handling, it minimizes the risk of bacterial contamination and ensures consistent product quality. The modular design allows for easy cleaning and maintenance, which is essential in food processing environments.
3. **Chemical and Fertilizer Production**: In chemical and fertilizer plants, the system handles abrasive and potentially hazardous powders. The robust design of the conveying components ensures durability and reliability, while the automated unpacking reduces exposure to harmful substances for operators.
4. **Industrial Bulk Handling**: For general industrial applications, the system improves overall operational efficiency by reducing downtime associated with manual unpacking and material transfer. The real-time monitoring feature allows for quick troubleshooting, minimizing production interruptions.
Operational Advantages and Performance Metrics
Implementing an intelligent bulk powder unpacking and conveying system offers several operational advantages that contribute to improved productivity and cost savings. Key benefits include:
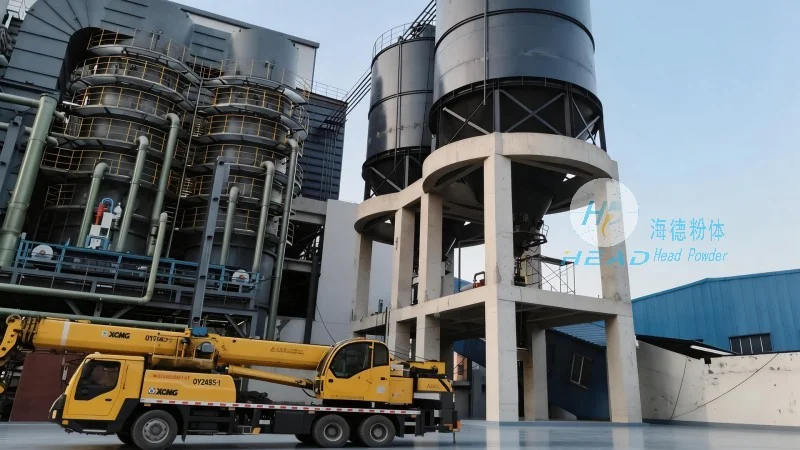
1. **Increased Throughput**: Automated systems can handle higher volumes of material compared to manual processes, leading to increased production rates.
2. **Reduced Labor Costs**: By automating the unpacking and conveying steps, businesses can reduce the need for manual labor, lowering labor costs and associated overhead.
3. **Enhanced Product Quality**: The system maintains the integrity of the powder, preventing segregation and degradation, which results in consistent product quality.
4. **Improved Safety**: Automated handling reduces the risk of accidents and exposure to hazardous materials, creating a safer working environment.
5. **Lower Maintenance Costs**: The modular design and robust components of the system result in lower maintenance requirements and reduced downtime for repairs.
Conclusion
Intelligent bulk powder unpacking and conveying systems represent a significant advancement in material handling technology. By integrating automated unpacking, advanced conveying, and real-time monitoring, these systems offer substantial benefits in terms of efficiency, safety, and product quality. For businesses operating in industries that rely on bulk powder handling, such as pharmaceuticals, food processing, and chemicals, adopting these technologies can provide a competitive edge and ensure long-term operational success. Shandong HeadPowder Engineering Co., Ltd. continues to innovate in this field, providing tailored solutions that meet the specific needs of their clients in China and beyond.




