HeadPowder, a prominent engineering company headquartered in Shandong, China, focuses on delivering advanced powder conveying solutions for the petrochemical industry. This article explores the fundamental principles governing petrochemical powder conveying lines and outlines the key operational characteristics that define their performance in practical applications.
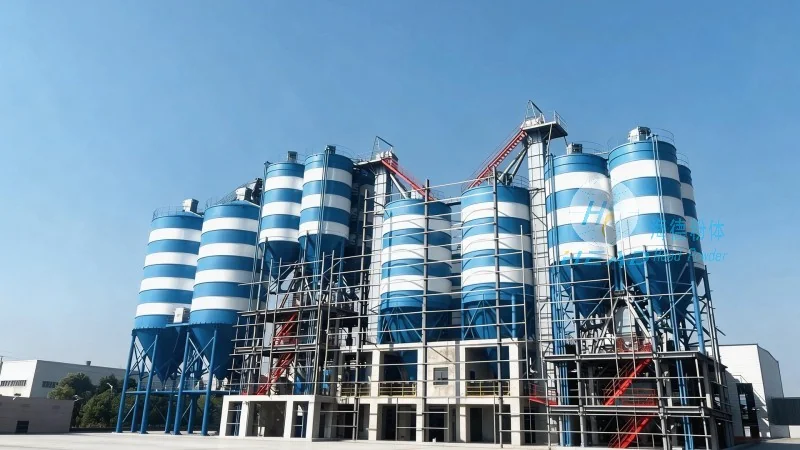
Core Principles Underpinning Petrochemical Powder Conveying Systems
The design and operation of petrochemical powder conveying systems are anchored in several critical principles aimed at ensuring efficient, safe, and reliable material transport. These principles encompass the selection of appropriate conveying technologies, such as screw conveyors, pneumatic systems, and vacuum pumps, which are tailored to handle the unique properties of powders used in petrochemical processes. The systems are engineered to maintain consistent flow rates, prevent material degradation, and minimize contamination risks. Additionally, the integration of advanced control systems enables real-time monitoring and adjustment, allowing operators to optimize performance under varying operational conditions. This proactive approach ensures that the conveying process remains stable and efficient, even when faced with fluctuations in material properties or system load.
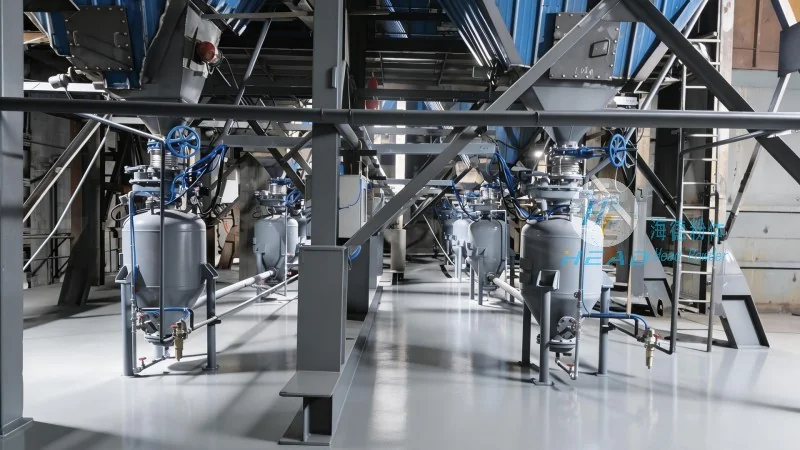
Operational Characteristics in Diverse Working Environments
Petrochemical powder conveying systems are deployed across a wide range of working environments, each presenting distinct challenges that influence system design and functionality. In bulk material handling facilities, these systems play a pivotal role in transporting raw materials like catalysts, additives, and chemical precursors to processing units. The operational characteristics in this context include high throughput capabilities, durability against corrosive substances, and compliance with stringent safety regulations. The systems are constructed using materials resistant to chemical exposure, such as stainless steel or specialized alloys, to extend service life and reduce maintenance requirements. Moreover, the flexibility of these systems allows for integration with existing infrastructure, enabling seamless material flow from storage silos to processing equipment. This adaptability is crucial for optimizing plant layout and minimizing material handling costs.
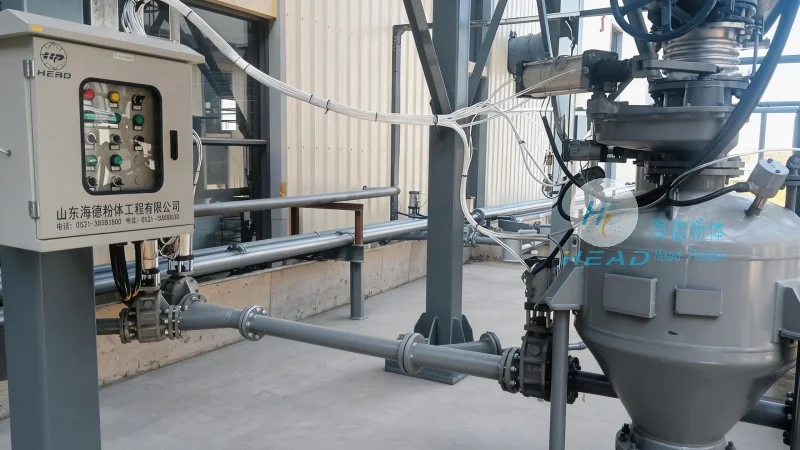
Application-Specific Operational Features and Performance
Each application of petrochemical powder conveying systems exhibits unique operational features that reflect the specific demands of the process. In the production of petrochemical products, the systems must maintain precise control over powder flow to ensure uniform mixing and consistent product quality. This involves the use of variable speed drives and pressure sensors to regulate conveying rates, which is essential for processes like polymerization or catalyst activation. The operational characteristics also include the ability to handle different particle sizes and densities, which may require adjustments in conveyor speed or air pressure. For instance, fine powders may necessitate lower air velocities to prevent segregation, while coarse materials may require higher speeds to maintain flow. The systems are equipped with features like air classifiers or cyclones to separate particles and maintain consistent size distribution, enhancing product quality and process efficiency.
Safety and Reliability in Petrochemical Conveying Operations
Given the hazardous nature of materials handled in the petrochemical industry, safety is a paramount consideration in the design and operation of powder conveying systems. The operational characteristics include robust safety features such as emergency shut-off valves, pressure relief mechanisms, and fire suppression systems. These components are integrated to prevent accidents and protect personnel and equipment from potential hazards. Additionally, the systems are designed with redundancy in critical components, such as motors and control panels, to minimize downtime in case of failures. Regular maintenance and inspection protocols are also implemented to ensure that the systems remain in optimal condition, reducing the risk of malfunctions. The reliability of these systems is further enhanced by the use of high-quality materials and advanced manufacturing techniques, which contribute to longer service life and lower maintenance costs.
Conclusion
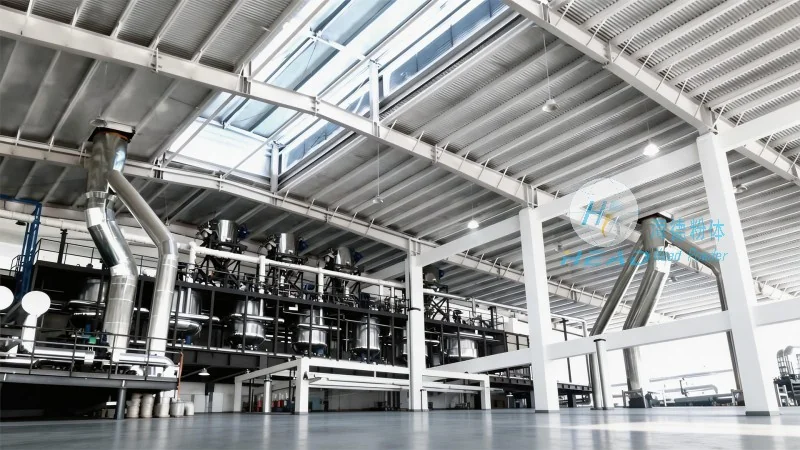
HeadPowder's expertise in petrochemical powder conveying systems ensures that clients receive tailored solutions that meet the specific operational needs of their facilities. By adhering to the core principles of efficient material transport and leveraging advanced technology, these systems enhance productivity, reduce downtime, and maintain compliance with industry standards. The operational characteristics discussed highlight the adaptability and reliability of these systems, making them indispensable in modern petrochemical operations. As the petrochemical industry continues to evolve, the importance of reliable powder conveying systems will only grow, underscoring the value of professional engineering and design in optimizing plant performance.




