Mineral sand material handling systems are critical components in modern industrial operations, particularly within the mining and processing sectors. These systems are engineered to efficiently transport mineral sands such as silica sand, quartz sand, and other abrasive raw materials from extraction sites to processing facilities, ensuring smooth and continuous material flow. The effectiveness of these systems directly impacts operational productivity, cost management, and overall efficiency in industrial settings.
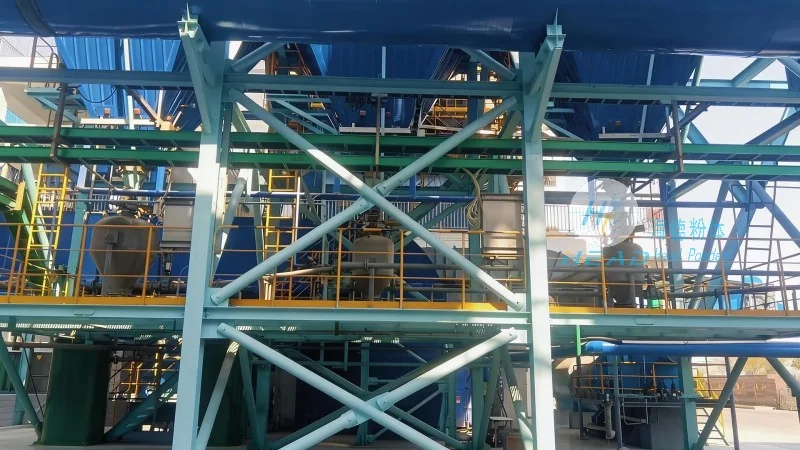
Core Principles of Mineral Sand Material Handling Systems
The fundamental principles of mineral sand material handling systems revolve around specialized machinery designed to handle bulk materials. Key equipment includes conveyors, elevators, and bulk material handling devices, which work in concert to move large volumes of sand with minimal disruption. The design of these systems considers factors like material density, moisture content, and abrasiveness, as these properties influence the choice of mechanical components and operational parameters. For instance, heavy-duty conveyor belts and robust pulley systems are typically employed to withstand the abrasive nature of mineral sands, ensuring long-term durability and reliability.
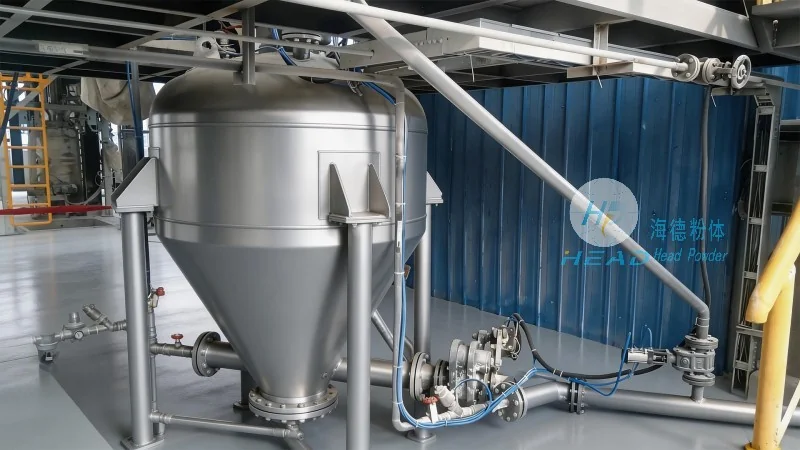
Working Scene Characteristics and Operational Adaptability
The working scene characteristics of mineral sand material handling systems vary significantly based on the specific application and environmental conditions. In open-pit mining operations, systems often integrate with long-distance conveyor belts capable of transporting sand over extensive distances, adapting to rugged terrain and large-scale production needs. Conversely, in processing plants, the systems may utilize more precise mechanisms like bucket elevators or screw conveyors to deliver sand to grinding, sorting, or filtration equipment with high precision. Environmental factors, including temperature fluctuations and humidity levels, also affect system performance, necessitating protective measures and durable materials to prevent wear and maintain efficiency. Moreover, these systems are designed for scalability, accommodating small-scale processing needs as well as large-scale industrial production, providing versatility across different operational scales.
Company Profile: Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., commonly referred to as headpowder, is a leading provider of mineral sand material handling solutions. Headquartered in Shandong, China, the company specializes in designing, manufacturing, and implementing customized material handling systems tailored to the unique demands of mining and processing industries. headpowder's expertise lies in addressing the specific challenges of mineral sand transportation, such as material abrasiveness and varying particle sizes, by developing innovative solutions that enhance operational efficiency and reduce maintenance costs. The company's commitment to quality, customer satisfaction, and technological advancement has established it as a trusted partner in the industry, offering comprehensive services from system design and installation to ongoing maintenance and technical support.
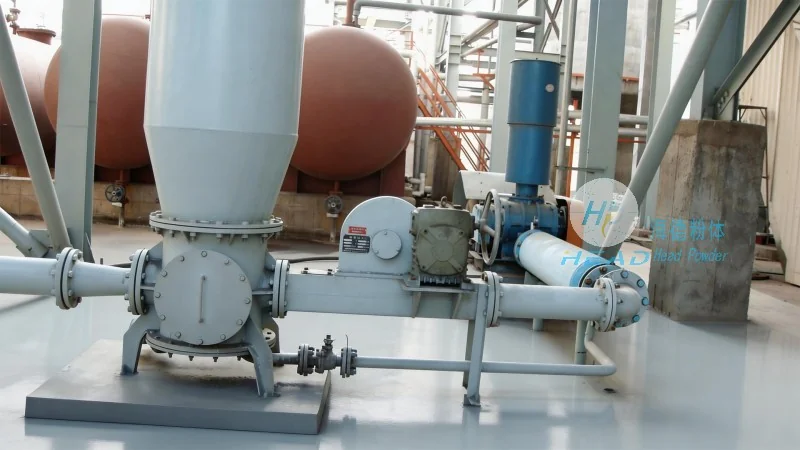
Key Features and Advantages of headpowder's Mineral Sand Material Handling Systems
headpowder's mineral sand material handling systems incorporate advanced engineering and robust construction to deliver superior performance and durability. Key features include high-capacity conveyor belts capable of handling large volumes of sand, mechanically reinforced components designed to withstand abrasive materials, and intelligent control systems that optimize operational efficiency. The benefits of these systems extend beyond basic transportation, contributing to overall process optimization, reduced labor costs, and enhanced workplace safety. By leveraging headpowder's expertise, clients can achieve reliable material flow, ensuring smooth operations and increased productivity in their mining and processing facilities. The company's focus on customization ensures that each system is tailored to meet specific operational requirements, providing a competitive edge in the industry.




