Gray bin material handling systems are critical components in industrial operations, particularly in facilities that process and store bulk materials such as powders, granules, and other fine particulates. These systems are designed to efficiently transport materials from storage bins to processing units, ensuring smooth workflow and operational reliability. The core principle behind these systems revolves around the integration of mechanical, electrical, and control technologies to achieve precise, automated material movement.
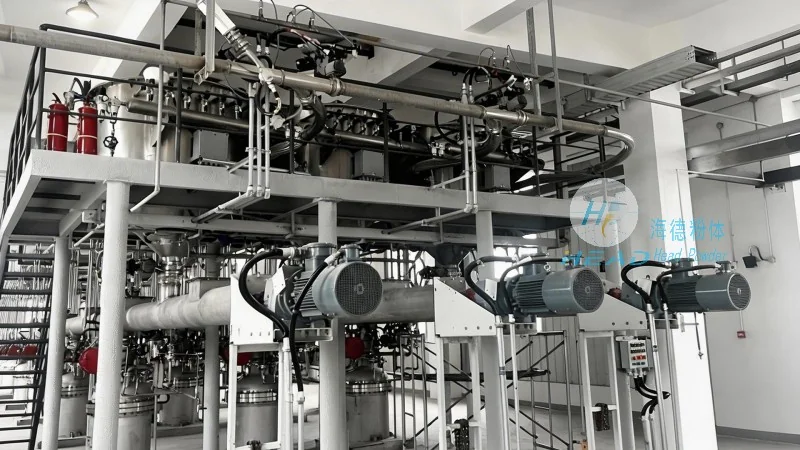
Principle of Material Handling in Gray Bins
The fundamental principle of gray bin material handling systems is to utilize a combination of conveyor mechanisms, such as screw conveyors, belt conveyors, or pneumatic systems, to move bulk materials from the storage bin to the point of use. The system typically includes a hopper or feed mechanism that draws material from the bin, a conveying component that transports it through a defined path, and a discharge mechanism that delivers the material to the next stage of processing. Advanced control systems, often incorporating sensors and programmable logic controllers (PLCs), regulate the speed, direction, and quantity of material flow, ensuring consistent and safe operation. This integrated approach minimizes manual intervention, reduces material loss, and enhances overall production efficiency.
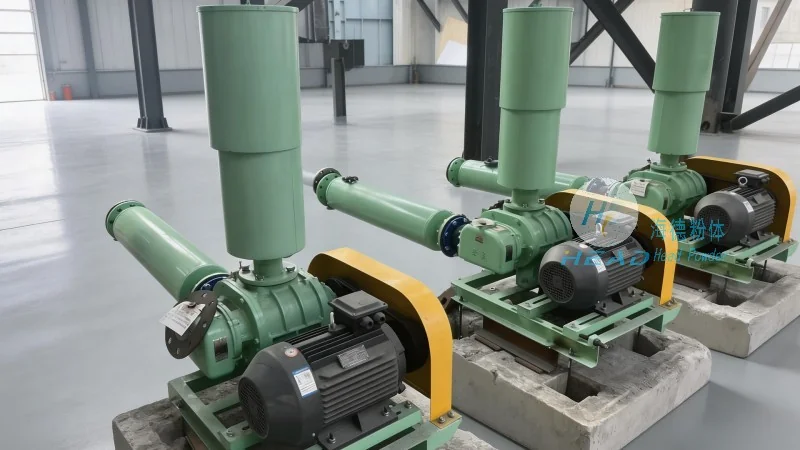
Key Working Scenarios and Operational Characteristics
Gray bin material handling systems are widely applied in various industrial sectors, including cement production, chemical processing, food processing, and pharmaceutical manufacturing. In cement plants, for instance, these systems are essential for transporting raw materials like limestone, clay, and iron ore from storage silos to grinding mills. The systems must handle large volumes of bulk materials with high accuracy, as any deviation can impact the quality of the final cement product. Similarly, in chemical and pharmaceutical industries, where material purity is paramount, the systems are designed to maintain strict contamination control and prevent cross-contamination between different batches. The operational characteristics of these systems include high throughput capacity, low maintenance requirements, and the ability to handle a wide range of material densities and particle sizes. They are also engineered for durability, with robust construction to withstand the harsh conditions often encountered in industrial environments.
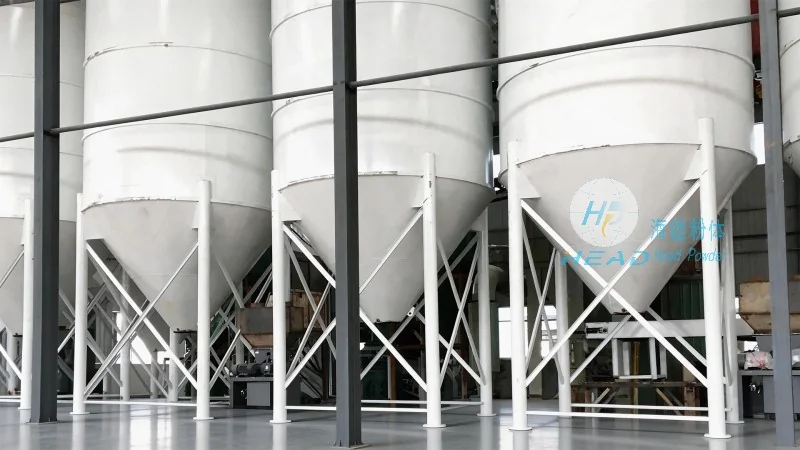
Technical Features and Advantages
Modern gray bin material handling systems are equipped with several technical features that enhance their performance and reliability. One key feature is the use of variable speed drives, which allow for precise control over the conveying speed, enabling the system to adapt to changing production demands. Additionally, the integration of level sensors and pressure transducers provides real-time monitoring of material levels and flow rates, alerting operators to potential issues before they escalate. The systems also often incorporate safety features, such as emergency stop buttons and interlocked access panels, to protect personnel and equipment. These technical advancements result in several operational advantages, including improved material handling efficiency, reduced downtime due to maintenance, and enhanced product quality through consistent material flow. Furthermore, the modular design of many systems allows for easy customization and expansion, making them suitable for both new installations and retrofits in existing facilities.
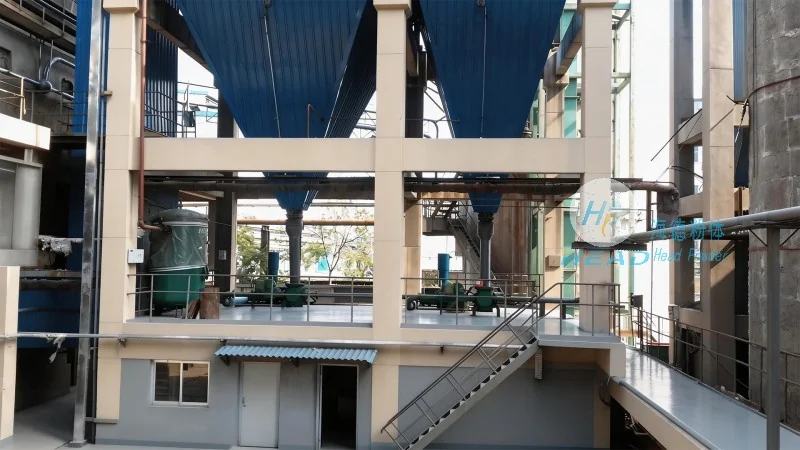
Company Overview: Shandong HeadPowder Engineering Co., Ltd.
HeadPowder, a leading provider of industrial material handling solutions, specializes in designing and manufacturing advanced gray bin material handling systems. With its headquarters in Shandong, China, the company has built a strong reputation for delivering high-quality, reliable equipment tailored to the specific needs of its clients. HeadPowder's team of experienced engineers and technicians leverages cutting-edge technology and rigorous quality control processes to ensure that each system meets the highest industry standards. The company's commitment to innovation and customer satisfaction has enabled it to serve a diverse range of industries, from traditional manufacturing to emerging sectors like renewable energy and advanced materials. By focusing on the principle of efficient material flow and operational excellence, HeadPowder continues to be a trusted partner for businesses seeking to optimize their material handling processes.




