The dust collection ash material conveying system is a specialized equipment designed for the efficient transportation of ash and other fine particulate materials generated from industrial processes. As a critical component in industrial waste management and material handling, this system ensures safe and reliable movement of dust-laden materials from collection points to disposal or processing facilities. The system's design integrates advanced engineering principles to address the unique challenges posed by ash materials, such as high moisture content, abrasive properties, and the need for dust control during transport.
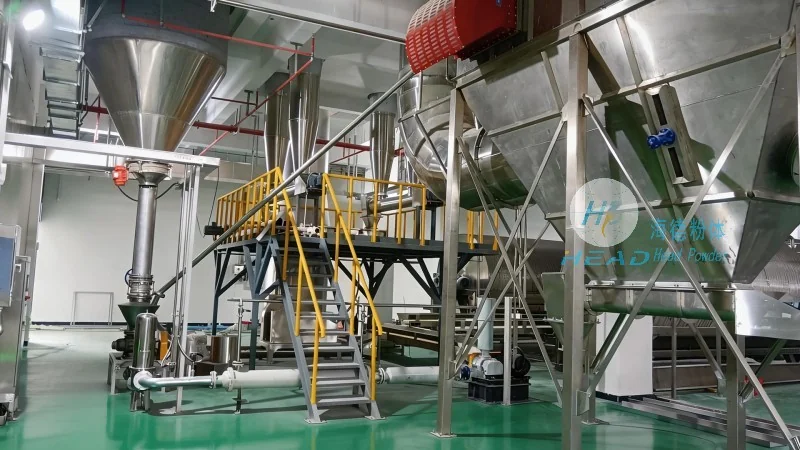
The Core Principle of Material Conveying
The fundamental principle of the material conveying system revolves around the use of positive pressure or negative pressure air flow to transport particulate materials. In positive pressure systems, a fan or blower generates a high-pressure air stream that carries the ash particles through a pipeline network. The air flow is directed through a hopper or collection chamber, where the ash is drawn into the system and propelled forward by the moving air. Negative pressure systems, on the other hand, utilize suction to draw ash from the collection point and transport it through the pipeline. Both systems employ specialized components like rotary valves, airlocks, and dust filters to maintain system integrity and prevent material leakage or air pollution.
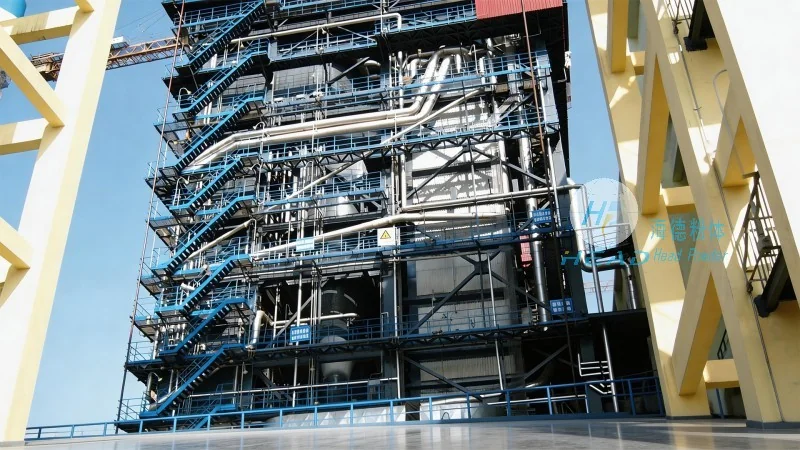
Key Working Scene Characteristics
The working scene characteristics of the dust collection ash material conveying system are tailored to the specific demands of industrial environments. These systems are typically deployed in power plants, cement factories, and other facilities where large volumes of ash are generated. The operational environment often involves high temperatures, high humidity, and the presence of corrosive substances, which requires robust construction materials and durable components. The system's design emphasizes safety, with features such as explosion-proof motors, fire-resistant materials, and automatic shutdown mechanisms to prevent accidents and ensure compliance with industrial safety standards.
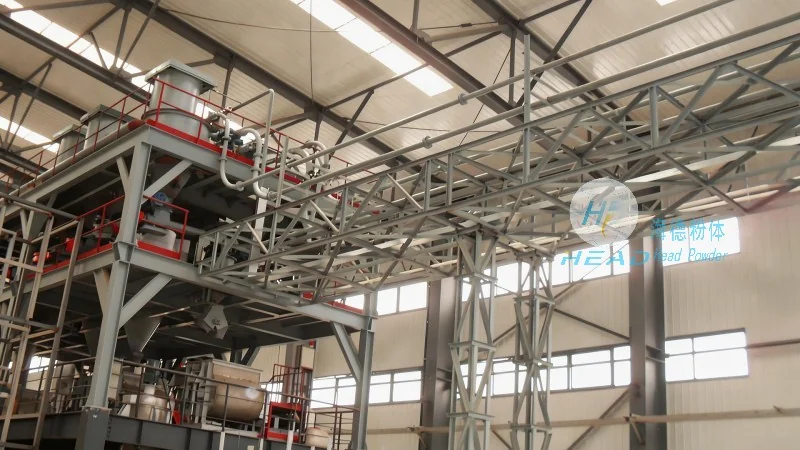
Application Scenarios and Operational Advantages
The application scenarios for the dust collection ash material conveying system are diverse and essential in modern industrial operations. In power plants, the system efficiently transports fly ash from boilers to storage silos or disposal sites, optimizing the plant's operational efficiency and reducing manual handling risks. In cement production, the system handles raw material ash and byproducts, facilitating the continuous flow of materials through the production line. The operational advantages include reduced labor costs, minimized environmental impact, and improved process control. The system's ability to handle high volumes of material at a consistent rate enhances overall production throughput and ensures reliable material supply for downstream processes.
Technical Specifications and System Components
The technical specifications of the dust collection ash material conveying system vary based on the specific application requirements. Key components include:
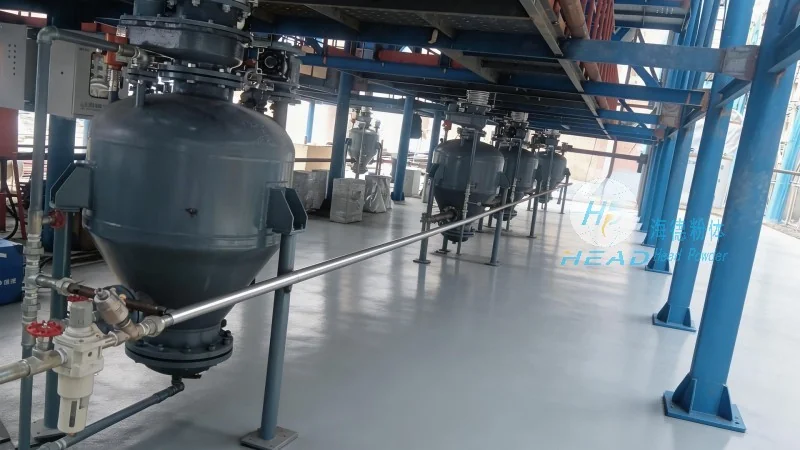
- Fan/Blower Unit: Provides the necessary air pressure to transport ash particles. Options range from centrifugal fans to positive displacement blowers, with specifications tailored to the system's capacity and pressure needs.
- Hopper and Collection Chamber: The initial point of material intake, where ash is collected and fed into the conveying system. These components are designed to handle high moisture content and abrasive materials, with features like heat insulation and wear-resistant linings.
- Rotary Valve and Airlock: Ensures controlled material flow into the pipeline, preventing backflow and maintaining system pressure. These components are critical for maintaining consistent material transport and preventing air leakage.
- Dust Filter and Separator: Removes fine ash particles from the air stream, ensuring compliance with environmental regulations and protecting downstream equipment from dust accumulation.
- Pipeline Network: Constructed from corrosion-resistant materials such as stainless steel or coated steel, the pipeline network is designed to withstand the abrasive nature of ash and maintain system efficiency over long distances.
Company Information and Contact Details
Shandong HeadPowder Engineering Co., Ltd. is a leading manufacturer specializing in industrial material handling systems. With a strong presence in China, particularly in Shandong province, the company has established itself as a trusted provider of dust collection and ash conveying solutions. The company's commitment to quality, innovation, and customer satisfaction has enabled it to serve a wide range of industrial sectors, including power generation, cement production, and chemical processing. HeadPowder's engineering expertise ensures that each system is tailored to meet the unique needs of its clients, delivering reliable and efficient material transport solutions.




