HeadPowder, a leading manufacturer based in Shandong, China, specializes in the design, development, and production of advanced pneumatic conveying systems tailored for flour and similar bulk materials. With a strong commitment to engineering excellence and customer satisfaction, the company has established itself as a trusted partner in the food processing and material handling industries.
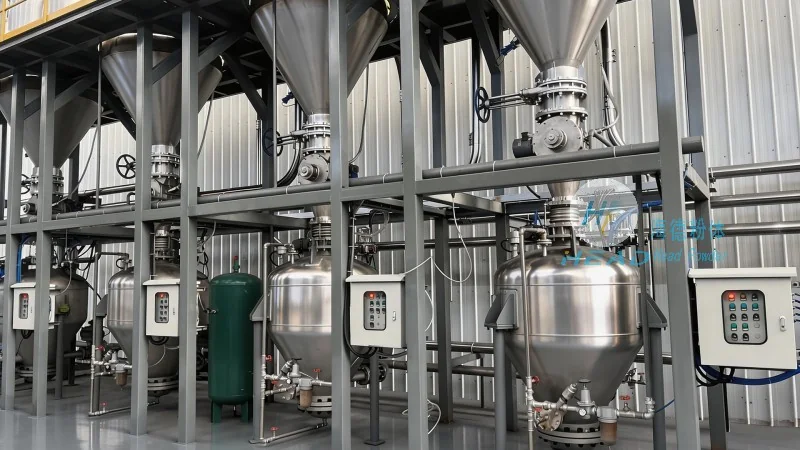
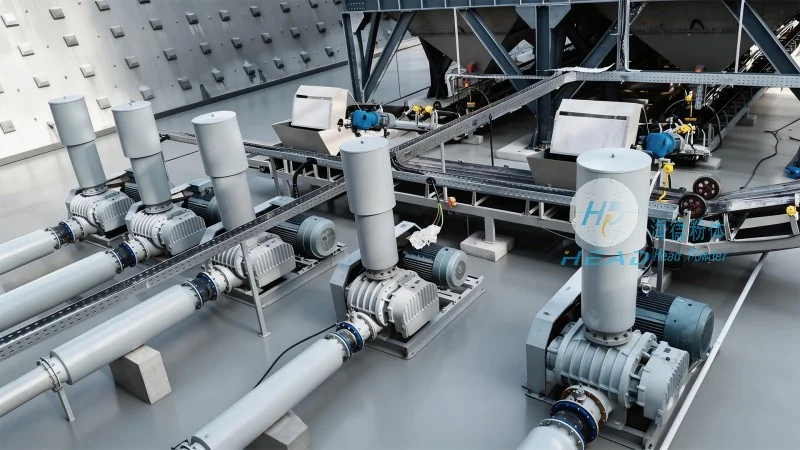
Introduction to Flour Material Pneumatic Conveying Equipment
HeadPowder's flour material pneumatic conveying equipment is engineered to efficiently transport bulk materials like flour, powders, and granules through a pressurized or vacuum system. This technology offers a hygienic, dust-free, and flexible solution for material handling in various industrial applications. The equipment is designed to meet stringent hygiene standards, making it ideal for food processing environments where cleanliness and product integrity are paramount.
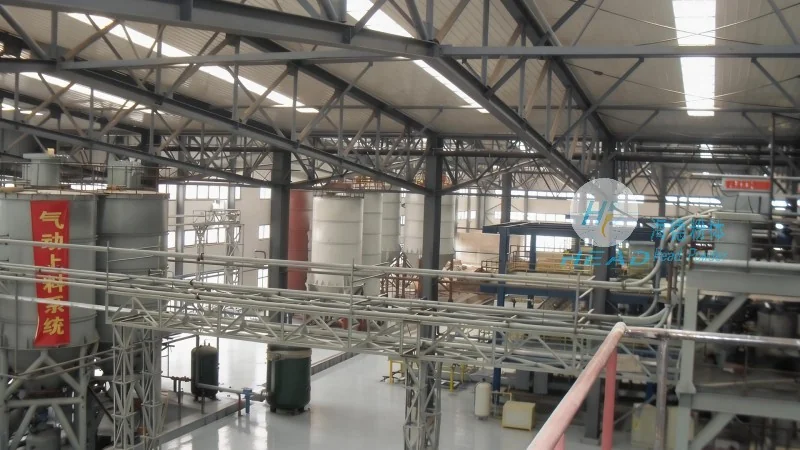
Working Principle of Pneumatic Conveying Systems
The core principle of pneumatic conveying involves using air or gas to move material through a pipeline. In a typical system, material is introduced into a hopper or feeder, where it is then drawn or pushed into the conveying line by the air flow. The system can operate under either positive pressure (pressure conveying) or negative pressure (vacuum conveying), depending on the application requirements. Positive pressure systems use compressed air to push material through the pipeline, while vacuum systems use a vacuum to pull material from the source. The choice between these methods depends on factors such as material characteristics, distance, and system layout. HeadPowder's equipment incorporates advanced control mechanisms to optimize air flow, pressure, and material feed rates, ensuring efficient and reliable operation.
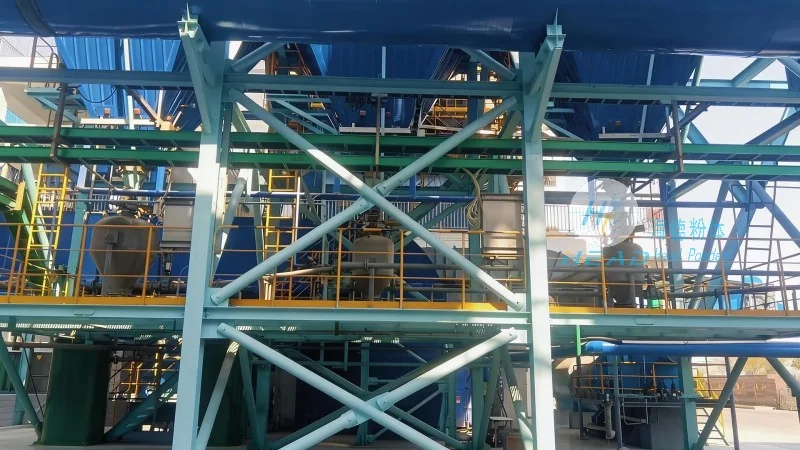
Key Characteristics and Working Scene Applications
HeadPowder's flour material pneumatic conveying equipment is characterized by several advantages that make it suitable for diverse working environments. Firstly, the system provides a dust-free and hygienic handling solution, which is crucial in food processing facilities where contamination control is essential. Secondly, it offers flexibility in material transport, allowing for vertical, horizontal, or inclined conveying paths, adapting to different plant layouts. Thirdly, the equipment is designed for easy integration with existing production lines, minimizing downtime during installation and operation. In working scenes, such as flour mills, bakeries, and food processing plants, this equipment efficiently moves raw materials from storage to processing areas, ensuring smooth workflow and consistent product quality. The system's ability to handle fine powders without clogging or degradation is particularly beneficial for maintaining the quality of flour and other sensitive materials. Additionally, the equipment's low maintenance requirements and energy efficiency contribute to long-term operational cost savings, making it a cost-effective solution for industrial material handling needs.




