Efficient and safe handling of powders is a critical requirement in various industrial sectors, including pharmaceuticals, food processing, and chemical manufacturing. Traditional open systems often lead to dust contamination, product loss, and safety hazards. To address these challenges, advanced dust-free and airtight powder handling equipment has been developed to ensure reliable, clean, and secure material transfer. This article provides an overview of such equipment, focusing on its structural design and operational principles.
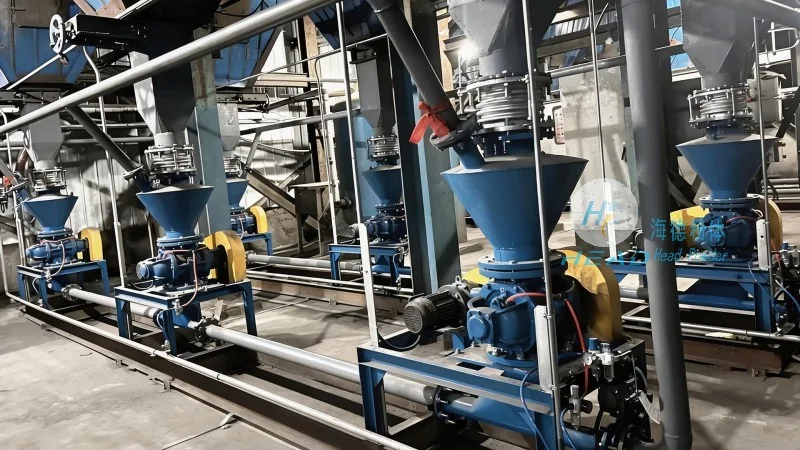
Key Features of Dust-Free and Airtight Powder Handling Equipment
Modern powder handling systems are engineered to minimize particle leakage and prevent cross-contamination. The primary features include:
- Sealed transfer mechanisms that maintain a controlled environment, preventing dust from escaping into the surrounding air.
- Integrated filtration systems that capture any released particles, ensuring compliance with environmental and health regulations.
- Material compatibility with a wide range of powders, including hygroscopic or abrasive substances, to avoid equipment degradation.
- Automated control systems that optimize flow rates and reduce human intervention, enhancing operational efficiency and safety.
Structural Components and Working Principles
The core components of dust-free powder handling equipment typically include feed hoppers, conveyor systems, valves, and dust collection units. The working principle revolves around creating a closed loop where powders are transferred without exposing them to the ambient air. Here’s a breakdown of the key structural elements:
1. Feed Hopper: The hopper is designed to store the powder and feed it into the system. It often includes a discharge valve to control the flow rate. The hopper is made of materials resistant to the specific powder properties, such as stainless steel or special polymers.
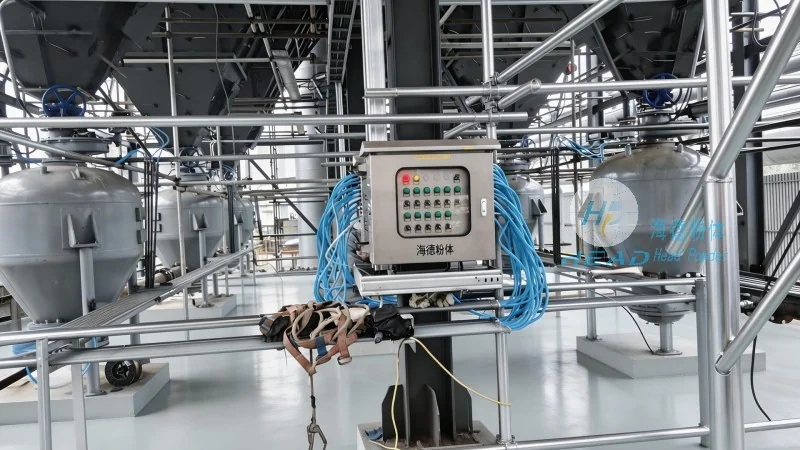
2. Conveyor System: The conveyor, usually a screw or pneumatic type, transports the powder from the hopper to the next stage. Screw conveyors are ideal for dry, free-flowing powders, while pneumatic systems use air to move powders, especially for fine or cohesive materials.
3. Valves and Seals: Specialized valves, such as rotary or slide valves, are used to control the flow and ensure airtight sealing. These components are critical in preventing dust leakage and maintaining the integrity of the system.
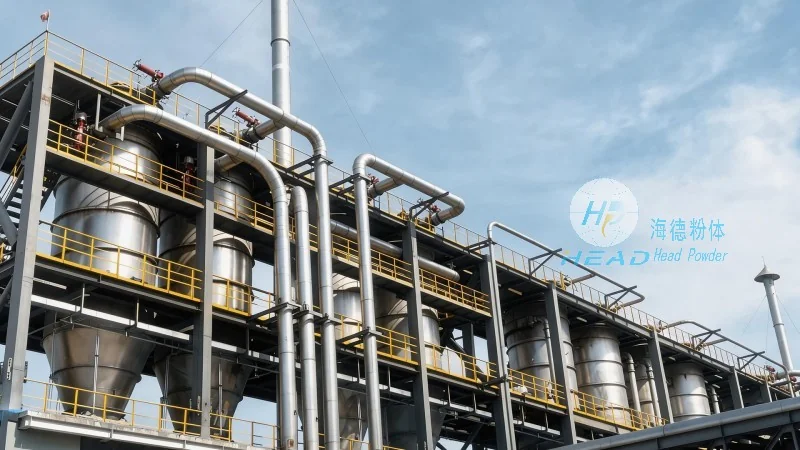
4. Dust Collection Unit: An integrated filtration system captures any particles that may escape during operation. This unit typically includes a filter bag or cartridge that can be cleaned or replaced to maintain efficiency.
Operational Benefits and Applications
Implementing dust-free and airtight powder handling equipment offers several advantages, including:
- Improved product quality by reducing contamination and ensuring consistent material properties.
- Enhanced workplace safety by minimizing exposure to airborne particles and preventing dust explosions.
- Increased operational efficiency through automated control and reduced downtime for cleaning or maintenance.
- Compliance with stringent environmental and regulatory standards, particularly in industries like pharmaceuticals and food processing.
These systems are widely used in applications such as bulk material storage, processing, and packaging, where maintaining a clean and controlled environment is paramount.
About Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., operating under the brand name headpowder, is a leading manufacturer specializing in advanced powder handling solutions. With a focus on innovation and quality, the company provides customized equipment tailored to the specific needs of various industries. HeadPowder’s products are designed to meet international standards and are known for their durability, efficiency, and reliability.
HeadPowder’s commitment to research and development ensures that their equipment incorporates the latest technologies in dust-free and airtight powder handling. The company’s facilities are located in Shandong, China, where they leverage local expertise and resources to deliver high-quality solutions to global markets.




