Shandong HeadPowder Engineering Co., Ltd., a leading manufacturer in the chemical processing industry, specializes in the design and supply of advanced pneumatic conveying systems for caustic soda. This article provides a detailed overview of the design considerations, technical specifications, and operational advantages of our caustic soda pneumatic conveying equipment. Our company, known as headpowder, is committed to delivering high-efficiency, reliable solutions tailored to meet the specific needs of clients in various industrial applications.
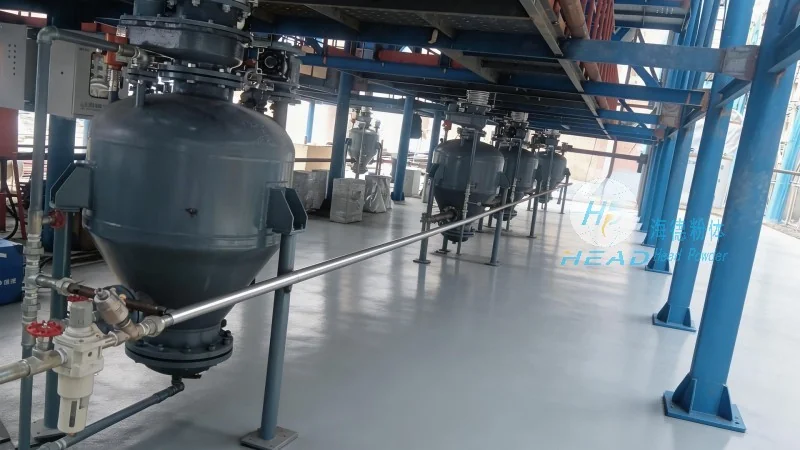
Key Design Elements for Efficient Caustic Soda Handling
The design of a caustic soda pneumatic conveying system involves several critical components that ensure safe, efficient, and cost-effective material transport. At headpowder, we focus on integrating robust engineering principles with state-of-the-art technology to optimize performance. The system typically includes a hopper for material storage, a rotary valve for controlled discharge, a conveying pipeline network, and a dust collection system. Each component is carefully selected and sized based on the material characteristics of caustic soda, such as its density, flowability, and reactivity. For instance, caustic soda is highly corrosive, so all contact parts are made from materials like stainless steel or specialized alloys to prevent degradation and ensure longevity.
Advantages of Pneumatic Conveying for Caustic Soda
Compared to traditional bulk handling methods like belt conveyors or screw conveyors, pneumatic conveying offers significant advantages for caustic soda transport. One of the primary benefits is the ability to handle abrasive and corrosive materials without the risk of mechanical wear or contamination. The system operates in a closed loop, minimizing dust emissions and environmental impact, which is crucial for compliance with industrial regulations. Additionally, pneumatic conveying systems can be designed for vertical or horizontal transport, providing flexibility in plant layout and space utilization. This adaptability makes them ideal for facilities with limited floor space or complex process flows. Furthermore, the system's ability to handle varying material flow rates and concentrations enhances operational efficiency, reducing downtime and maintenance costs.
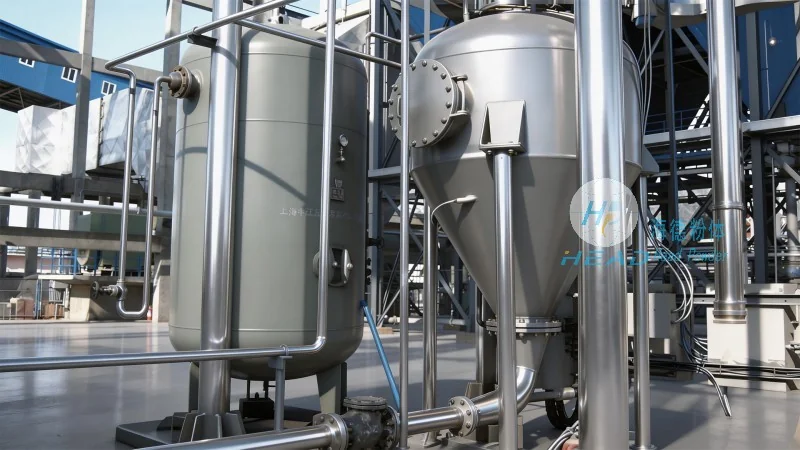
Technical Specifications and Performance Metrics
Our caustic soda pneumatic conveying equipment is engineered to meet stringent performance standards. Key technical specifications include a conveying capacity ranging from 5 to 200 tons per hour, depending on the system configuration. The system operates at pressures between 0.5 to 1.5 bar, with air consumption rates optimized to balance efficiency and energy usage. The design incorporates advanced control systems that monitor pressure, flow, and temperature in real-time, ensuring safe and stable operation. These controls also enable automatic start-up and shutdown sequences, enhancing safety and reducing human intervention. The equipment is equipped with high-efficiency dust filters and cyclone separators to maintain air quality and prevent material buildup in the system. Regular maintenance intervals are scheduled to ensure optimal performance, with replacement parts readily available from our company.
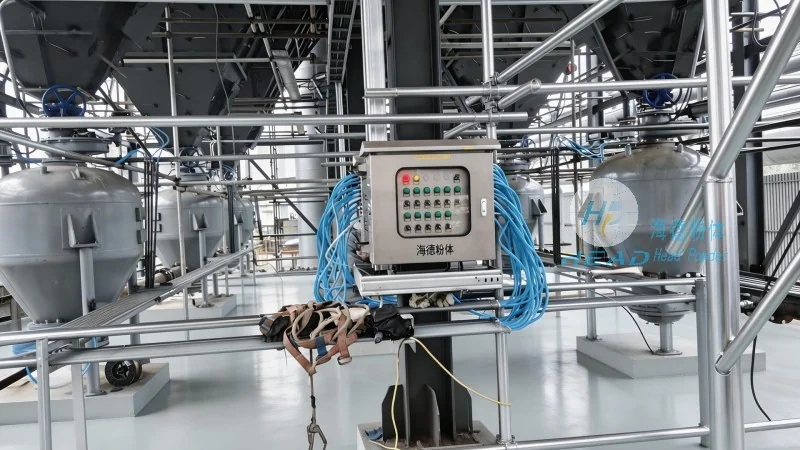
Application Scenarios and Industry Use Cases
The caustic soda pneumatic conveying system is widely used in various industrial sectors, including chemical manufacturing, pulp and paper production, and water treatment. In chemical plants, it facilitates the transport of caustic soda from storage tanks to reactors or processing units, ensuring a continuous and controlled supply. In the pulp and paper industry, the system is essential for delivering caustic soda to digesters and bleaching processes, where precise material control is critical for product quality. Water treatment facilities also benefit from this technology, as it enables the efficient distribution of caustic soda for pH adjustment and sludge treatment. The system's adaptability allows it to be integrated into existing plant infrastructure with minimal disruption, making it a cost-effective upgrade for many operations.
Customization and After-Sales Support
At headpowder, we understand that each client has unique operational requirements. Therefore, our caustic soda pneumatic conveying systems are customizable to meet specific needs. We offer a range of options, including different material handling capacities, conveying distances, and integration with existing process control systems. Our engineering team works closely with clients to assess their requirements and develop tailored solutions. After the system is installed, we provide comprehensive after-sales support, including training for operators, regular maintenance services, and technical assistance. This commitment to customer support ensures that our clients can maximize the performance and lifespan of their equipment. Our company is located in Shandong, China, and serves clients globally with a focus on quality and reliability.




