For companies operating in the sugar industry, the efficient and reliable transportation of raw and processed sugar is a critical aspect of their production processes. Pneumatic conveying systems have emerged as a preferred solution for handling sugar, offering advantages that traditional methods cannot match. This article explores the role of pneumatic conveying in sugar transportation, highlighting its benefits and applications within the industry.
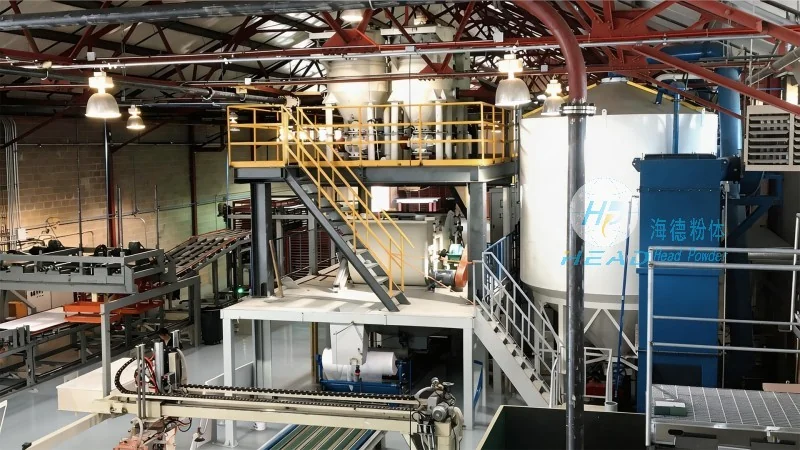
About Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., based in Shandong, China, is a leading provider of advanced material handling solutions, including specialized pneumatic conveying systems for the sugar sector. With years of experience in engineering and manufacturing, the company focuses on delivering high-quality equipment tailored to the unique demands of sugar processing facilities. HeadPowder's commitment to innovation and customer satisfaction has established it as a trusted partner for sugar producers seeking efficient and reliable transportation solutions.
Pneumatic Conveying Systems for Sugar Handling
Pneumatic conveying systems utilize air or gas to transport bulk materials like sugar through a network of pipes. These systems are available in various configurations, such as positive pressure, negative pressure, and hybrid designs, allowing for flexibility in different operational scenarios. For sugar handling, positive pressure systems are commonly used, where air is forced through the pipeline to move the sugar, ensuring consistent flow and minimal product degradation. The systems are equipped with specialized components, including rotary valves, airlocks, and filters, which help maintain product quality and prevent contamination.
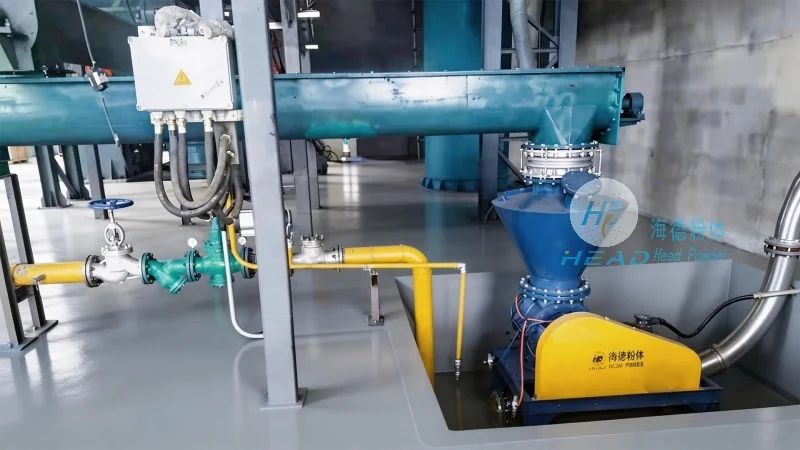
Efficient Sugar Transportation Solutions
In sugar processing plants, pneumatic conveying systems play a vital role in moving sugar from storage silos to processing units, or from processing stages to packaging areas. The systems enable seamless integration into existing production lines, reducing the need for manual handling and minimizing the risk of product spillage or loss. By automating the transportation process, sugar manufacturers can improve operational efficiency, reduce labor costs, and enhance overall productivity. The systems are designed to handle different sugar types, including raw cane sugar, refined white sugar, and specialty sugars, ensuring compatibility with various production requirements.
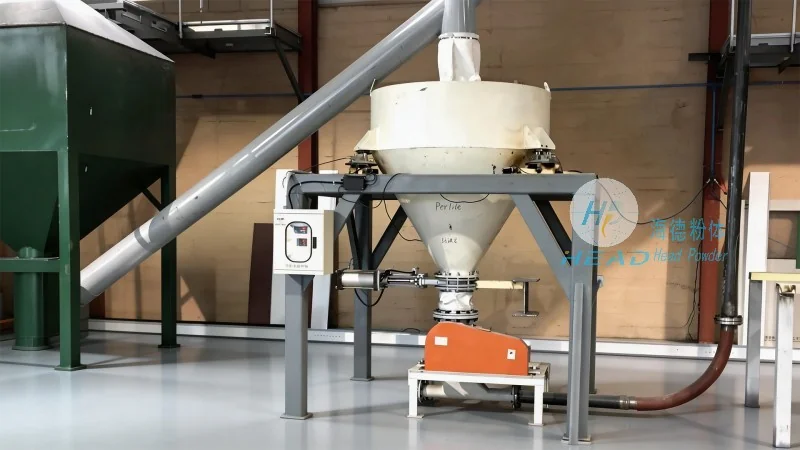
Technical Advantages of Pneumatic Conveying in Sugar Handling
One of the key advantages of pneumatic conveying for sugar transportation is its ability to maintain product integrity. Unlike mechanical conveyors, which can cause abrasion or breakage, pneumatic systems use air to gently move sugar, preserving its granular structure and preventing caking or clumping. This is particularly important for high-value sugars, where product quality directly impacts market value. Additionally, pneumatic conveying reduces the risk of dust generation, which is a common issue in traditional sugar handling methods. By containing the material within a sealed system, the risk of dust inhalation and environmental contamination is minimized, enhancing workplace safety and compliance with regulatory standards.
Reliable and Efficient Sugar Handling with HeadPowder
Shandong HeadPowder Engineering Co., Ltd. offers comprehensive pneumatic conveying solutions tailored to the specific needs of sugar producers. The company's engineers work closely with clients to design and implement systems that optimize material flow, reduce downtime, and improve overall operational performance. By leveraging advanced technology and industry expertise, HeadPowder ensures that its systems are durable, energy-efficient, and easy to maintain. The company's commitment to quality and customer support has made it a preferred choice for sugar manufacturers seeking reliable and efficient transportation solutions. Whether for new installations or system upgrades, HeadPowder provides the expertise and equipment needed to enhance sugar handling processes and improve business outcomes.




