Organic fertilizer granule pneumatic conveying systems are specialized equipment designed to transport granular organic fertilizers efficiently and reliably. These systems are crucial in agricultural and industrial settings where the safe and effective movement of organic fertilizer materials is essential. The technology behind these systems leverages the principles of pneumatic conveying, which uses air to move particles through a pipeline network. This approach offers several advantages over traditional mechanical conveying methods, including reduced equipment wear, lower maintenance costs, and improved material handling capabilities.
Key Components of the Pneumatic Conveying System
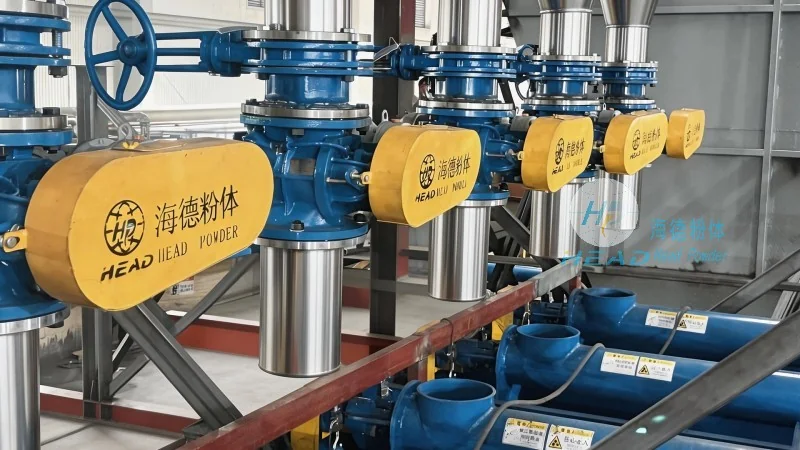
The organic fertilizer granule pneumatic conveying system typically consists of several core components that work in concert to achieve efficient material transport. The primary components include a hopper or storage silo for holding the organic fertilizer granules, a feeder mechanism to control the flow of material into the system, a conveying line (often a pipeline) through which the material is transported, and a receiver or discharge point where the material is deposited. Additionally, the system may incorporate a blower or compressor to generate the necessary air pressure and flow. In some designs, a filter or separator may be included to remove any fine particles or moisture from the air, ensuring clean operation and preventing contamination of the fertilizer.
How the Pneumatic Conveying Process Works
The operation of an organic fertilizer granule pneumatic conveying system follows a systematic process. First, the organic fertilizer granules are loaded into the storage hopper. The feeder then regulates the flow of granules into the conveying line, ensuring a consistent feed rate. Simultaneously, the blower generates a flow of air through the pipeline. As the granules enter the conveying line, they are entrained by the air stream and carried along the pipeline to the discharge point. The air and material mixture travels through the pipeline, and at the receiver, the material is separated from the air, often through a cyclone or other separation device. The separated air may be recirculated or vented, while the organic fertilizer granules are collected and ready for use.
Advantages of Using Pneumatic Conveying for Organic Fertilizers
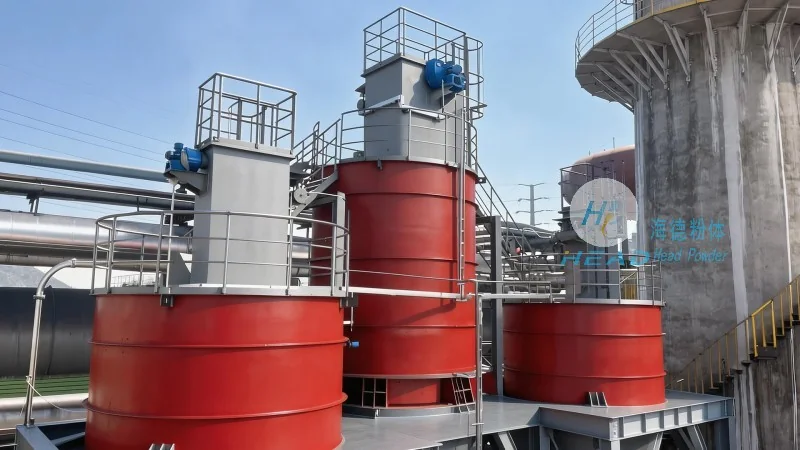
There are several key advantages to employing pneumatic conveying systems for organic fertilizer granules. First, the system minimizes physical contact between the fertilizer and equipment, reducing the risk of contamination and degradation. This is particularly important for organic fertilizers, which may be sensitive to moisture or temperature changes. Second, pneumatic conveying systems can handle a wide range of particle sizes and densities, making them versatile for different types of organic fertilizers. Third, the system is relatively compact and can be installed in various configurations, including vertical or horizontal layouts, to fit the space constraints of a facility. Additionally, the reduced wear and tear on components result in lower maintenance costs and longer equipment lifespan. Finally, the system can operate continuously, providing a steady supply of fertilizer to processing or application equipment.
Applications and Industries
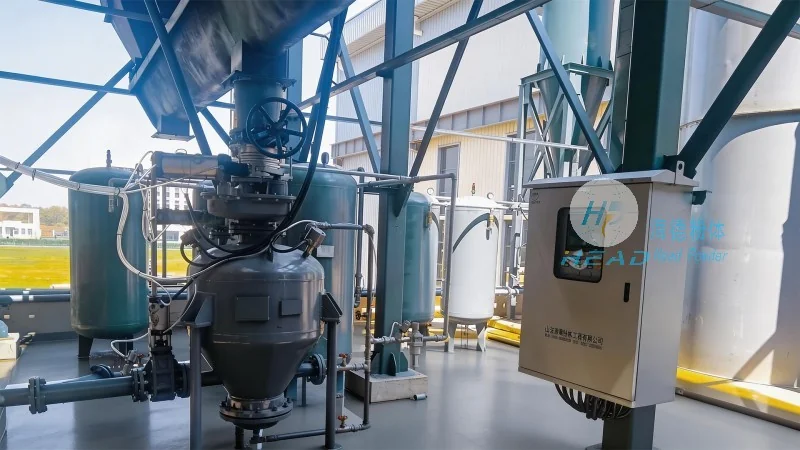
Organic fertilizer granule pneumatic conveying systems are widely used in various industries, including agricultural production, composting facilities, and fertilizer manufacturing plants. In agricultural settings, these systems are used to transport organic fertilizer from storage silos to application equipment, such as spreaders or injectors. In composting facilities, the system helps move composted materials from processing areas to storage or distribution points. In fertilizer manufacturing, the system is integral to the production process, transporting raw materials and finished granules between processing stages. The versatility of the pneumatic conveying system makes it suitable for a range of applications where efficient material handling is critical.
Company Overview: Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., commonly known as headpowder, is a leading manufacturer and supplier of specialized engineering solutions for the fertilizer and agricultural industries. With a focus on innovation and quality, the company has established itself as a trusted partner for businesses seeking reliable and efficient pneumatic conveying systems. HeadPowder's expertise lies in designing and manufacturing customized solutions that meet the unique requirements of each client. The company's facilities are located in Shandong, China, where it leverages advanced technology and skilled personnel to develop cutting-edge equipment. By prioritizing customer needs and adhering to strict quality standards, headpowder ensures that its products deliver optimal performance and longevity.




