Mineral sand powder conveyors are specialized equipment designed to transport fine mineral powders efficiently and reliably. These systems are crucial in industries such as mining, chemical processing, and material handling, where the movement of bulk materials in a controlled manner is essential for operational efficiency. Understanding the functionality and design principles of these conveyors is vital for selecting the right equipment for specific applications.
Understanding the Core Function of Mineral Sand Powder Conveyors
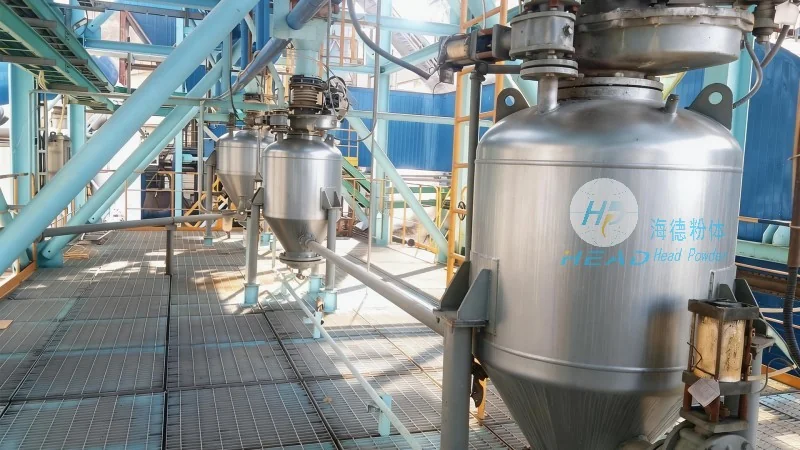
The primary function of a mineral sand powder conveyor is to transport dry, fine mineral powders from one location to another within a processing facility. Unlike traditional bulk material handling systems, these conveyors are engineered to handle materials with particle sizes typically ranging from a few microns to several millimeters. The design focuses on minimizing material degradation, preventing dust generation, and ensuring consistent flow rates, which are critical factors in maintaining product quality and process stability.
Design Principles Behind Mineral Sand Powder Conveyors
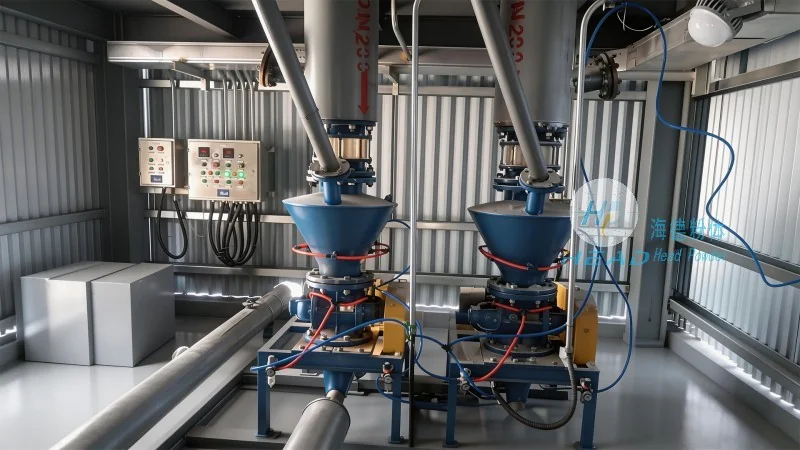
The design of mineral sand powder conveyors is guided by several key principles to ensure optimal performance. First, the system must maintain a consistent air flow and pressure to prevent material settling or clogging. This is achieved through the use of positive pressure or vacuum systems, depending on the application. Second, the conveyor components are constructed from materials that are resistant to corrosion and wear, as mineral powders can be abrasive and may contain corrosive substances. Third, the design emphasizes energy efficiency and low maintenance, with features like adjustable speed controls and easy access for cleaning and maintenance.
Key Components and Their Roles in the System
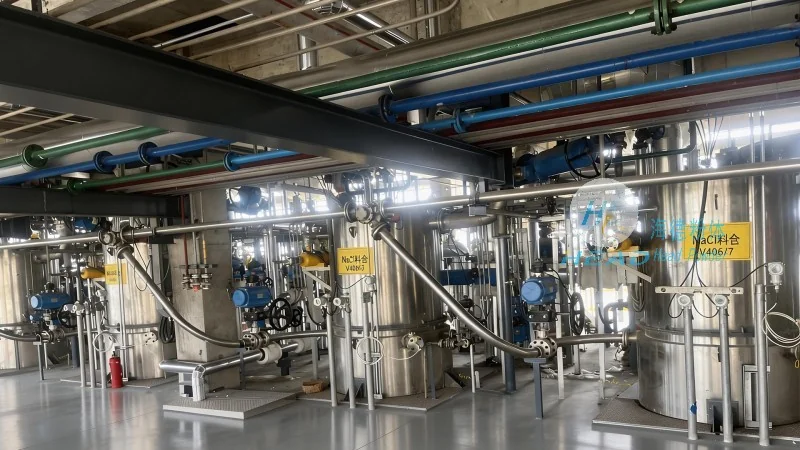
Mineral sand powder conveyors typically consist of several key components, each playing a critical role in the overall operation. The main components include the hopper or feed inlet, which holds the material and feeds it into the conveyor system. The conveyor itself, which may be a pneumatic system using air to move the powder, or a mechanical system with a rotating drum or screw. The control system, which regulates the flow rate and pressure, ensuring smooth operation. Additionally, there are often dust collection and filtration systems to manage air quality and comply with environmental regulations.
Application Scenarios and Operational Advantages
Mineral sand powder conveyors are widely used in various industrial applications. In mining operations, they are used to transport sand and other fine minerals from processing plants to storage or for further processing. In chemical industries, they help move powders such as cement, fertilizers, and other chemical products. The operational advantages of these conveyors include reduced labor costs, increased safety by minimizing manual handling of powders, and improved product quality through consistent and controlled transport. Moreover, the systems can be integrated with other processing equipment, creating a seamless material handling workflow.
About Shandong HeadPowder Engineering Co., Ltd.
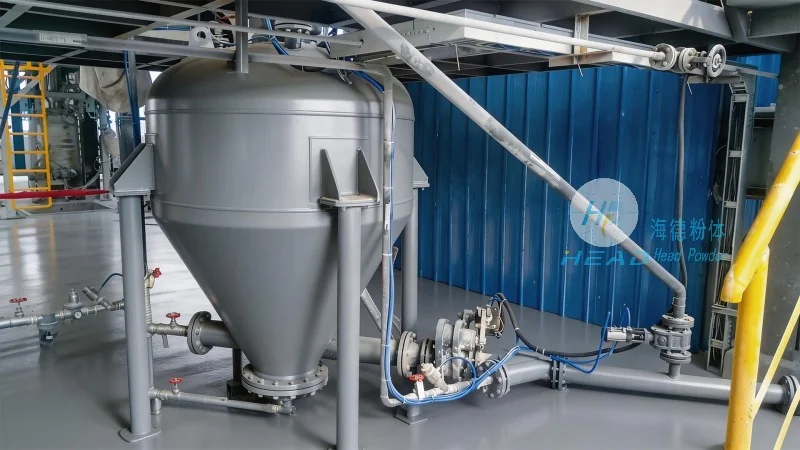
Shandong HeadPowder Engineering Co., Ltd. is a leading manufacturer of mineral sand powder conveyors and related material handling equipment. Based in Shandong, China, the company specializes in designing and producing high-quality conveyor systems tailored to the specific needs of various industries. With a focus on innovation and customer satisfaction, HeadPowder Engineering provides reliable and efficient solutions for mineral sand and powder transportation. The company's products are known for their durability, energy efficiency, and adherence to industry standards, making them a trusted choice for businesses seeking to enhance their material handling processes.




