Sodium hexafluorophosphate (SHFP) is a critical chemical compound widely used in various industrial applications, including pharmaceuticals, electronics, and chemical synthesis. The efficient and safe handling of this powder is paramount to ensure operational efficiency and maintain product integrity. A specialized piece of equipment designed for this purpose is the sodium hexafluorophosphate powder conveyor, which is engineered to transport SHFP with precision and reliability. This article delves into what such a conveyor is and explores the fundamental design principles that underpin its functionality.
Introduction to Sodium Hexafluorophosphate Powder Conveyors
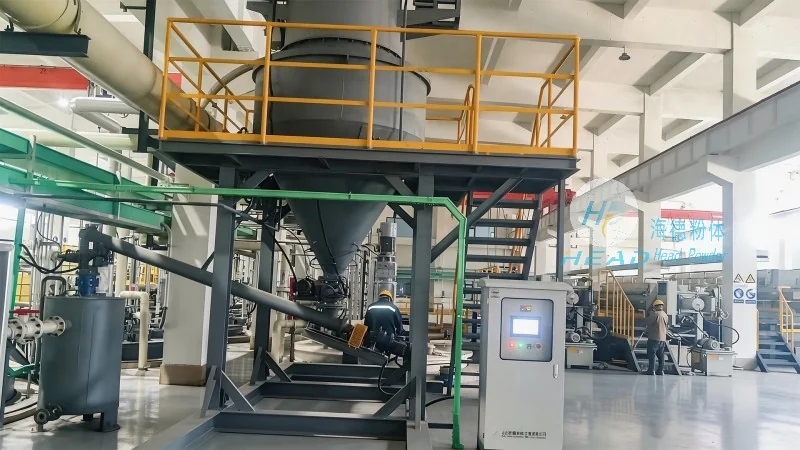
HeadPowder, a leading manufacturer based in Shandong, China, specializes in the design and production of advanced powder handling systems. The sodium hexafluorophosphate powder conveyor is a tailored solution that addresses the unique challenges associated with transporting this specific chemical. Unlike conventional conveyors, this equipment is built to withstand the corrosive and reactive nature of SHFP, ensuring minimal risk of contamination or equipment damage. The conveyor system is designed to maintain a closed environment, preventing dust emissions and protecting both personnel and the environment from exposure to the chemical.
Key Design Principles of the Conveyor System
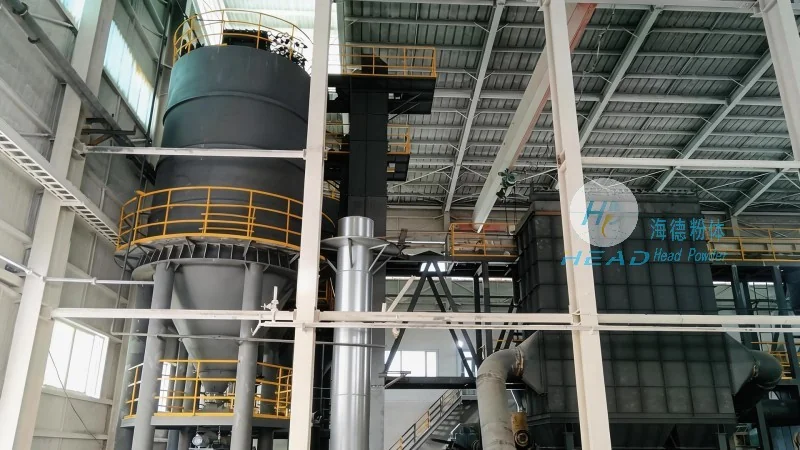
The design of a sodium hexafluorophosphate powder conveyor incorporates several critical principles to ensure optimal performance and safety. First, the material selection is paramount. The conveyor components, including hoppers, chutes, and drive mechanisms, are constructed from corrosion-resistant materials such as stainless steel or specialized alloys. This choice prevents chemical degradation and extends the equipment's lifespan. Second, the system employs a robust sealing mechanism to eliminate any potential for powder leakage. Sealed hoppers and airtight connections are standard features, ensuring that the powder remains contained throughout the transport process. Third, the conveyor is equipped with advanced control systems that allow for precise regulation of flow rates and speed. This control is essential for maintaining consistent product quality and preventing overloading or underloading of the system.
Operational Advantages and Safety Features
Implementing a sodium hexafluorophosphate powder conveyor offers numerous operational advantages. The closed-loop design minimizes dust generation, which not only improves workplace safety but also reduces the risk of product contamination. Additionally, the system's ability to maintain a consistent flow rate enhances process efficiency, leading to higher productivity and lower operational costs. Safety is a top priority in the design, with features like emergency stop buttons, overfill protection, and regular maintenance reminders integrated into the system. These measures ensure that the equipment operates within safe parameters at all times, protecting both operators and the surrounding environment.
Conclusion and Company Information
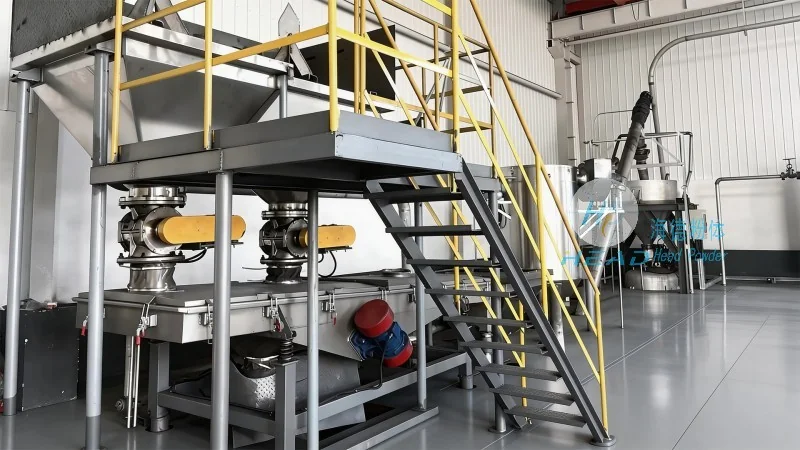
For industries dealing with sodium hexafluorophosphate, investing in a specialized powder conveyor is a strategic decision that enhances operational efficiency and ensures compliance with safety regulations. HeadPowder Engineering Co., Ltd., located in Shandong, China, is a trusted provider of such advanced equipment. Their expertise in powder handling technology, combined with a commitment to quality and safety, makes them a reliable partner for businesses seeking to optimize their SHFP processing operations. By adhering to the design principles outlined above, these conveyors provide a reliable solution for the safe and efficient transport of sodium hexafluorophosphate, supporting the smooth operation of industrial processes.




