When it comes to industrial material handling, the gray bin powder conveying system equipment plays a crucial role in efficiently transporting bulk materials. This equipment is specifically designed to handle powders and granules, ensuring smooth and reliable material movement within various industrial processes. The following article will delve into the specifics of this equipment, including its components, operational principles, and the underlying design philosophies that make it effective for industrial applications.
Introduction to Gray Bin Powder Conveying Systems
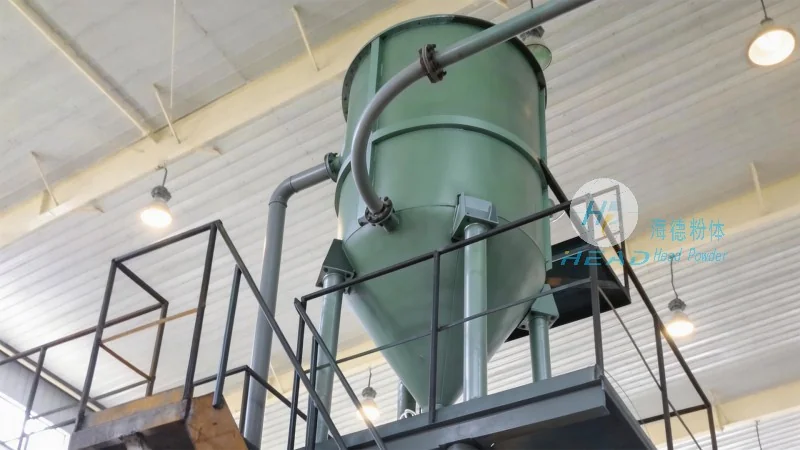
A gray bin powder conveying system is a specialized piece of industrial equipment used to transport bulk powders and granular materials from one location to another. The system typically incorporates a storage bin, often referred to as a gray bin, which serves as the primary container for the material. This bin is designed to hold a substantial quantity of the powder, allowing for continuous or intermittent feeding into the conveying mechanism. The equipment is commonly used in industries such as pharmaceuticals, food processing, chemicals, and mining, where the handling of fine powders is essential for production and processing.
Key Components of the Gray Bin Powder Conveying System
The gray bin powder conveying system consists of several critical components that work in tandem to achieve efficient material transport. The primary components include the gray storage bin, a feeding mechanism, a conveying device, and a control system. The gray bin is constructed from durable materials, such as stainless steel or high-density plastic, to ensure resistance to corrosion and wear from the powders being handled. It is equipped with a hopper or outlet at the bottom, which allows the material to be discharged into the feeding mechanism. The feeding mechanism, often a rotary valve or a screw feeder, regulates the flow of material from the bin into the conveying system, preventing overfeeding and ensuring a consistent flow rate. The conveying device, which can be a pneumatic or mechanical system, transports the material through a pipeline or conveyor belt to the destination point. The control system manages the operation of all components, including the feeding rate, conveying speed, and safety features, ensuring optimal performance and preventing accidents.
Design Principles Behind the Gray Bin Powder Conveying System
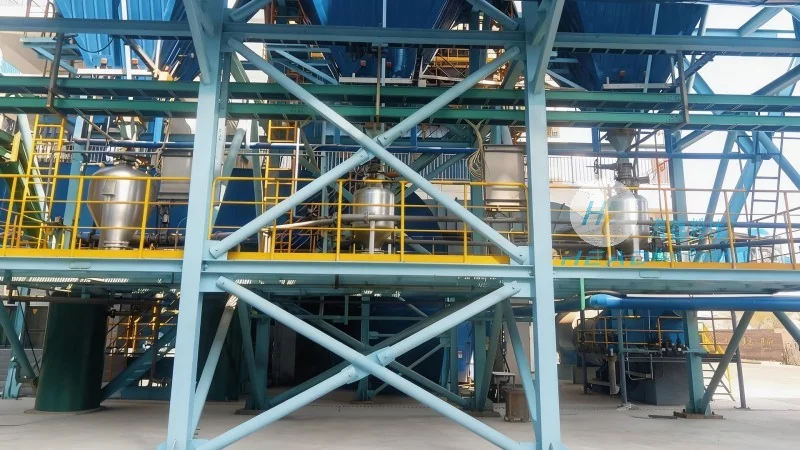
The design of the gray bin powder conveying system is guided by several key principles aimed at maximizing efficiency, reliability, and safety. One of the primary design considerations is the prevention of material buildup and blockages, which can occur due to the nature of powders. The system incorporates features such as smooth internal surfaces and angled hopper designs to minimize the risk of clogging. Additionally, the equipment is designed to handle a wide range of powder properties, including different particle sizes, densities, and flow characteristics. This adaptability is achieved through adjustable feeding mechanisms and variable-speed conveying systems. Another important design principle is the maintenance of material integrity and purity. The system is constructed from materials that are non-reactive with the powders being handled, and it includes features such as dust collection and filtration to prevent contamination. The control system is also designed to minimize human intervention, reducing the risk of errors and ensuring consistent operation. Furthermore, the design prioritizes safety by incorporating features such as emergency stop buttons, overload protection, and interlocks to prevent accidents and ensure compliance with safety regulations.
Operational Mechanisms and Efficiency
The operational mechanisms of the gray bin powder conveying system are designed to provide consistent and reliable material transport. The system typically operates by first filling the gray bin with the powder, which is then fed into the conveying device at a controlled rate. The conveying device then transports the material through the pipeline or conveyor to the destination, such as a processing unit or storage area. The speed of the conveying device can be adjusted to match the production requirements, allowing for flexibility in operation. The system is equipped with sensors and monitoring devices that track the level of material in the bin and the flow rate, providing real-time data for process control. This data helps operators to optimize the system's performance, reduce downtime, and improve overall efficiency. The design of the system also considers energy efficiency, with features such as variable-speed drives that adjust the power consumption based on the load. This not only reduces operational costs but also contributes to environmental sustainability.
Applications and Benefits in Industrial Settings
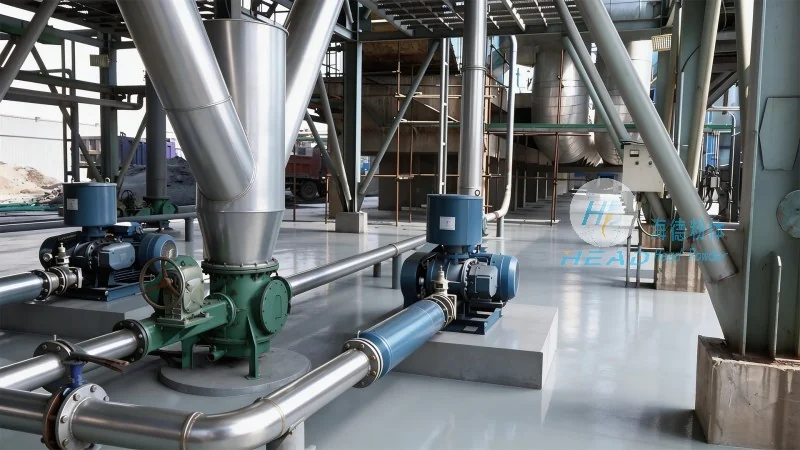
The gray bin powder conveying system is widely used in various industrial settings due to its versatility and efficiency. In the pharmaceutical industry, for example, the system is used to transport active pharmaceutical ingredients (APIs) and excipients, ensuring that the materials are handled in a sterile and controlled environment. The equipment's design allows for easy cleaning and maintenance, which is crucial in pharmaceutical manufacturing to prevent contamination. In the food processing industry, the system is used to transport ingredients such as flour, sugar, and spices, maintaining the quality and safety of the products. The system's ability to handle fine powders without causing segregation or degradation is particularly beneficial in food applications. In the chemical industry, the system is used to transport various chemicals, including powders and granules, ensuring safe and efficient handling. The system's design also allows for the handling of hazardous materials, with features such as explosion-proof components and dust suppression systems to prevent accidents. The benefits of using the gray bin powder conveying system include increased productivity, reduced labor costs, improved material quality, and enhanced safety in industrial operations.
Conclusion
In conclusion, the gray bin powder conveying system equipment is a vital component in modern industrial material handling. Its design, incorporating durable materials, efficient feeding mechanisms, and reliable conveying systems, ensures that powders and granular materials are transported safely and efficiently. The system's adaptability to various powder properties and its focus on safety and maintenance make it an ideal choice for a wide range of industrial applications. As industries continue to evolve and demand higher efficiency and quality in material handling, the gray bin powder conveying system remains a key technology in ensuring smooth and reliable operations. With its robust design and operational capabilities, this equipment continues to play a crucial role in supporting industrial production and processing.




