

Ammonium Bicarbonate Material Handling System Equipment: What It Is and Its Design Principles
Ammonium bicarbonate, a widely used chemical in various industrial applications, often requires efficient and reliable material handling systems to ensure safe and effective processing. The Ammonium Bicarbonate Material Handling System Equipment, developed by Shandong HeadPowder Engineering Co., Ltd., is a specialized solution designed to address the unique challenges associated with transporting this compound. This equipment is engineered to meet the stringent safety and operational standards required in chemical processing environments, providing a robust and efficient means of moving ammonium bicarbonate from storage to processing units or other destinations within a facility.
Understanding the Ammonium Bicarbonate Material Handling System Equipment
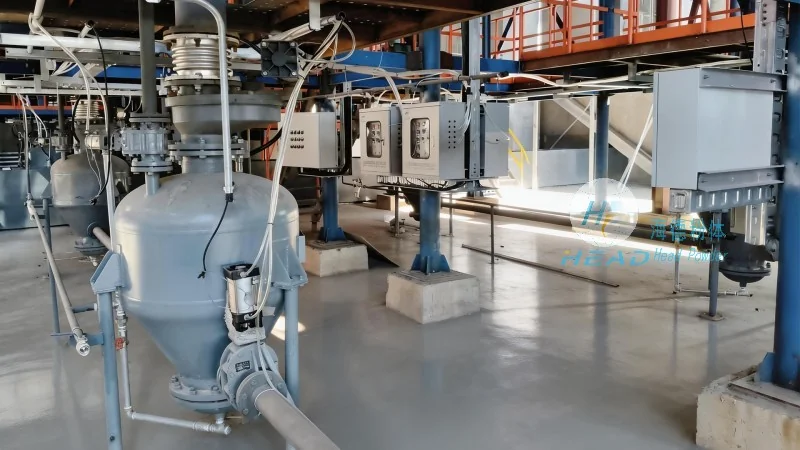
The Ammonium Bicarbonate Material Handling System Equipment is a comprehensive setup that integrates various components to facilitate the safe and efficient movement of ammonium bicarbonate. At its core, this system is designed to handle the material's physical properties, such as its granular or powder form, and the need for controlled temperature and pressure conditions during transport. The equipment typically includes components like conveyor systems, storage tanks, and specialized valves or pumps that are constructed from materials resistant to the chemical's corrosive nature. These components work in tandem to ensure that the material is moved without degradation or contamination, maintaining its quality throughout the process.
Key Design Principles of the Ammonium Bicarbonate Material Handling System
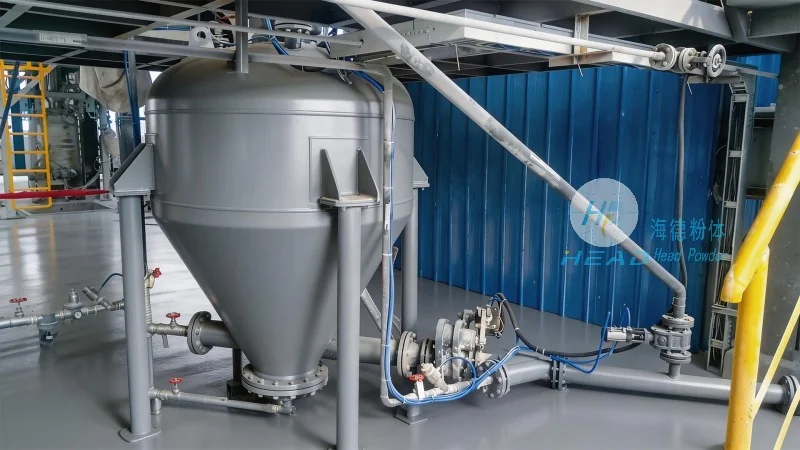
The design of the Ammonium Bicarbonate Material Handling System Equipment adheres to several critical principles to ensure optimal performance and safety. One of the primary principles is the use of corrosion-resistant materials for all contact surfaces. Since ammonium bicarbonate can be slightly acidic or reactive under certain conditions, the equipment is built with materials like stainless steel or specialized alloys that can withstand exposure without degradation. This not only prolongs the equipment's lifespan but also prevents contamination of the material being handled. Another key principle is the implementation of airtight and sealed systems to minimize the risk of dust generation and exposure to the environment. Ammonium bicarbonate is a fine powder that can become airborne, posing health risks and affecting the material's quality if not properly contained. The system incorporates dust collection and filtration mechanisms to capture any particles, ensuring a clean and safe working environment. Additionally, the design emphasizes energy efficiency and operational reliability. The equipment is engineered to operate with minimal energy consumption while maintaining consistent performance, reducing operational costs for the end-user. The use of advanced control systems allows for precise monitoring and adjustment of the material flow, ensuring that the system operates within optimal parameters at all times.
Components and Functionality of the Material Handling System
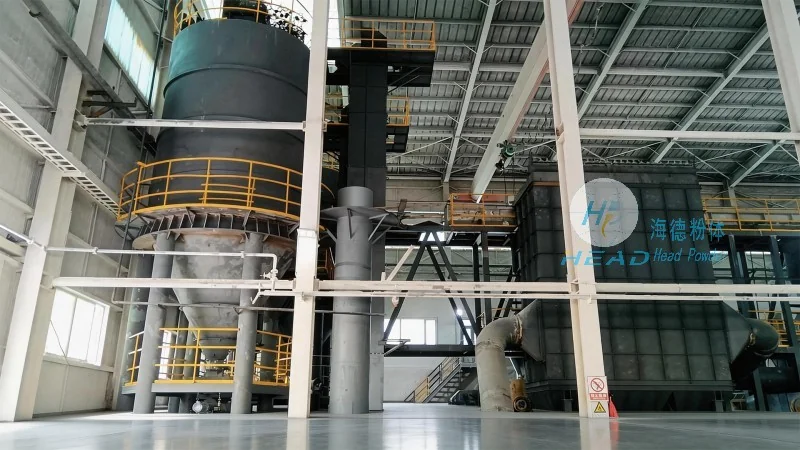
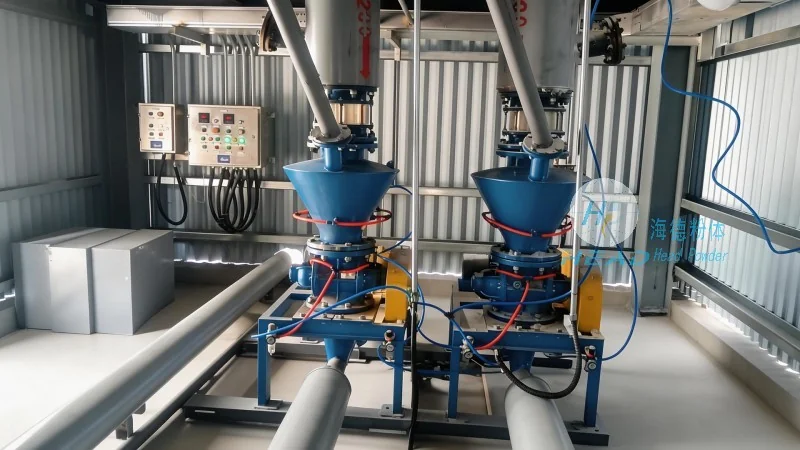
The Ammonium Bicarbonate Material Handling System Equipment consists of several key components, each playing a vital role in the overall operation. The primary component is the storage tank, which is designed to hold the ammonium bicarbonate in a controlled environment. These tanks are equipped with temperature and pressure monitoring systems to ensure that the material remains within safe operating limits. The storage tank is connected to a conveyor system, which can be either a belt conveyor or a screw conveyor, depending on the specific application requirements. The conveyor system is responsible for transporting the material from the storage tank to the processing area or other parts of the facility. The system may also include a dosing or feeding mechanism, which allows for precise control over the amount of ammonium bicarbonate being moved. This is particularly important in applications where the material is used in precise formulations or reactions. The equipment also includes safety features such as pressure relief valves and emergency shut-off systems to prevent accidents and ensure the safety of personnel and equipment. These features are designed to comply with industry standards and regulations, providing an additional layer of protection in the event of unexpected situations.
Applications and Benefits of the System
The Ammonium Bicarbonate Material Handling System Equipment is used in a variety of industrial applications where ammonium bicarbonate is a key component. These applications include the production of fertilizers, food additives, and pharmaceuticals. In the fertilizer industry, the system is used to transport ammonium bicarbonate to mixing and granulation units, ensuring that the material is evenly distributed and processed efficiently. In the food industry, the system is used to move the compound to production lines where it is incorporated into various food products, such as baking powders or leavening agents. The system's ability to handle the material safely and efficiently makes it an essential part of these production processes. The benefits of using this equipment extend beyond just efficient material handling. The system reduces the risk of accidents and exposure to the material, improving workplace safety. It also minimizes material loss and contamination, which can lead to cost savings and improved product quality. Additionally, the system's energy efficiency helps to reduce operational costs, making it a cost-effective solution for industrial users. The reliability of the equipment ensures consistent performance, reducing downtime and maintenance costs over time.
Conclusion and Company Information
The Ammonium Bicarbonate Material Handling System Equipment, developed by Shandong HeadPowder Engineering Co., Ltd., represents a sophisticated and reliable solution for the safe and efficient handling of ammonium bicarbonate. The system's design, based on principles of corrosion resistance, airtight containment, and energy efficiency, ensures that it meets the demanding requirements of modern industrial applications. By integrating advanced components and safety features, the equipment provides a robust and dependable means of transporting ammonium bicarbonate, supporting the smooth operation of various production processes. Shandong HeadPowder Engineering Co., Ltd., with its headquarters in China, specializes in engineering solutions for chemical material handling, providing tailored systems that address the unique needs of each client. The company's commitment to quality and safety is reflected in the design and construction of its equipment, making it a trusted partner for industries relying on ammonium bicarbonate in their operations.