

What is a Fine Sand and Gravel Material Pneumatic Conveyor? Understanding Its Design Principles
Fine sand and gravel material pneumatic conveyors are specialized systems engineered to transport granular materials such as fine sand, gravel, and similar particulate substances through a pipeline using compressed air. These systems are widely utilized across various industries, including construction, mining, and material processing, where efficient and dust-free material handling is essential. The primary function of such conveyors is to move bulk materials from one location to another without relying on mechanical components like belts or buckets, instead leveraging the force of air to propel the material through the system.
Core Design Principles of Pneumatic Conveyors for Fine Materials
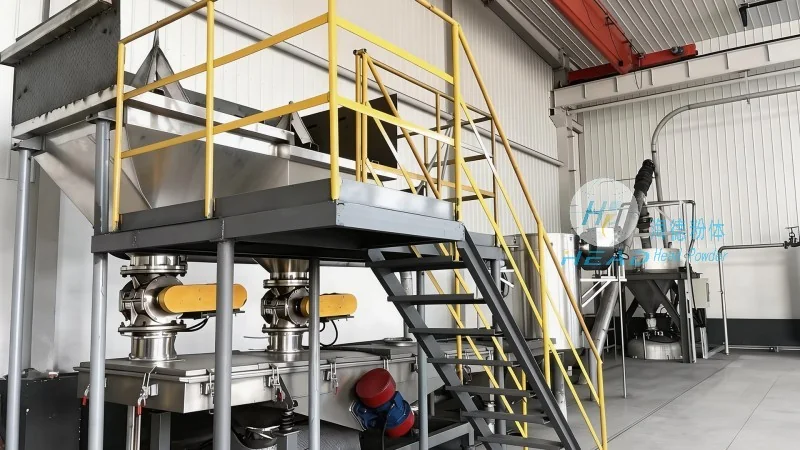
The design of a fine sand and gravel material pneumatic conveyor is built upon several fundamental principles that ensure efficient operation and material handling. At the heart of the system is an air compressor or fan that generates the necessary pressure to move the material. The pipeline network, typically constructed from stainless steel or other corrosion-resistant materials, forms the path through which the material travels. Material feeders, often equipped with valves or screw mechanisms, control the flow rate of the granular material into the system. The air flow is carefully managed to maintain a consistent velocity, preventing material settling or blockages. Key design considerations include the air-to-material ratio, which balances the amount of air used to the quantity of material being conveyed, and the system's pressure and velocity parameters, which are tailored to the specific characteristics of the fine sand or gravel being handled.
About Shandong HeadPowder Engineering Co., Ltd.
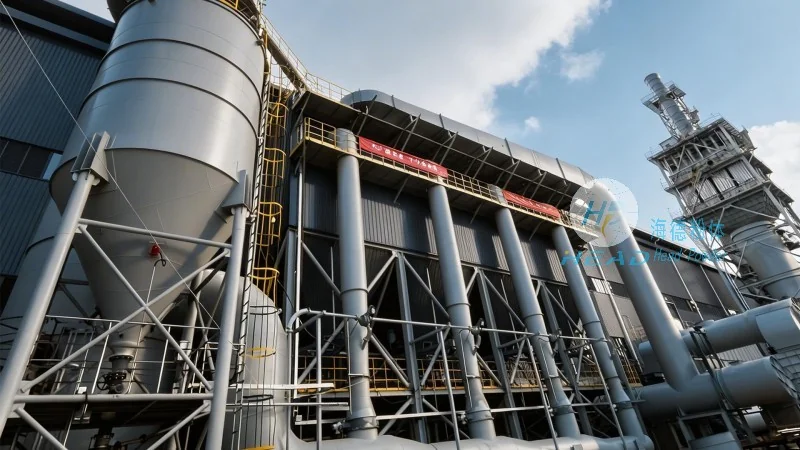
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a leading manufacturer specializing in the design and production of pneumatic conveying equipment for diverse industrial applications. With a strong focus on engineering excellence and customer satisfaction, HeadPowder has established itself as a trusted provider of high-quality fine sand and gravel material pneumatic conveyors. The company's expertise lies in integrating advanced design principles with practical application needs, ensuring that their systems meet the rigorous demands of modern material handling operations. HeadPowder's commitment to innovation and quality control has positioned them as a key player in the industry, delivering reliable and efficient solutions for clients worldwide.
Technical Components and Operational Mechanics
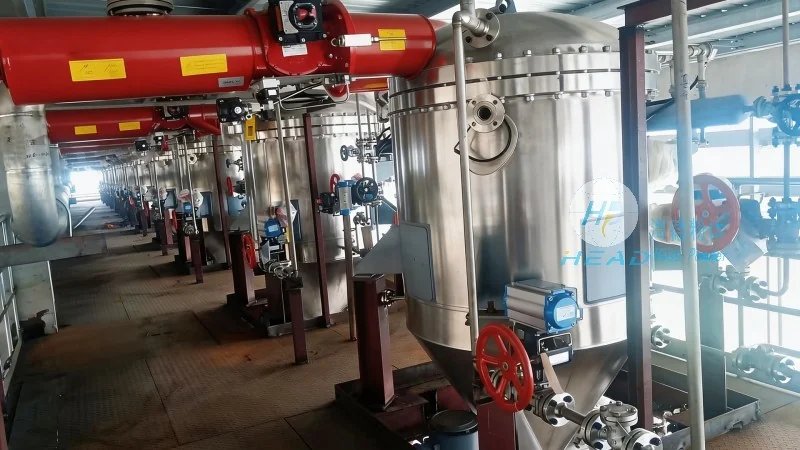
The operational mechanics of a fine sand and gravel material pneumatic conveyor involve a coordinated interaction between air and material. When the material is introduced into the system, it is suspended in the air stream created by the compressor. The air flow, controlled by the fan's speed and the system's pressure settings, propels the material through the pipeline. The design of the pipeline, including bends and transitions, is critical to maintaining the air flow and preventing material deposition. Material feeders are designed to introduce the granular material at a controlled rate, ensuring a steady flow into the system. The air-to-material ratio is a crucial parameter, as an optimal ratio ensures efficient conveying without excessive energy consumption. HeadPowder's systems are engineered to maintain this balance, using advanced control systems to adjust air flow and material feed rates as needed.
Applications and Benefits in Industrial Settings
Fine sand and gravel material pneumatic conveyors are employed in a variety of industrial settings where traditional conveying methods may be less effective or practical. In construction sites, these systems are used to transport sand and gravel to different locations on-site, reducing the need for manual handling and improving safety. In mining operations, they facilitate the transport of fine materials from processing plants to storage or processing facilities. The benefits of using pneumatic conveyors for fine materials include dust reduction, as the material is contained within the pipeline, and the ability to handle materials in a closed system, minimizing environmental impact. Additionally, these systems offer flexibility in layout, as the pipeline can be installed in various configurations to suit the site's layout. HeadPowder's fine sand and gravel material pneumatic conveyors are designed to deliver these benefits while providing reliable performance and low maintenance requirements.
Engineering Considerations and Maintenance
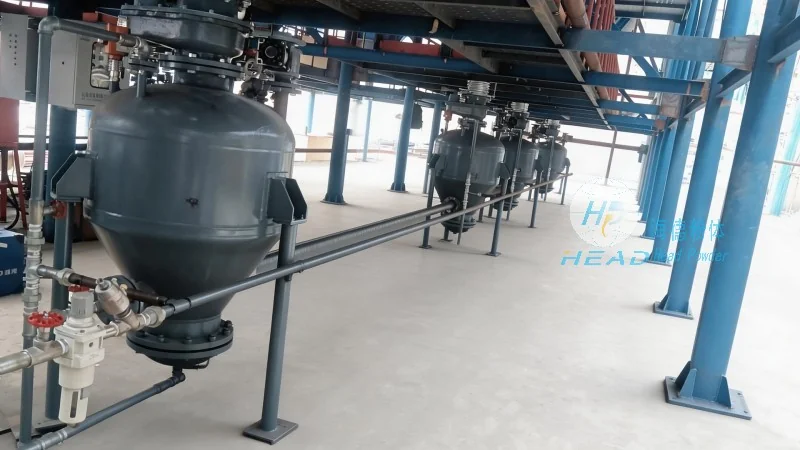
Designing and operating a fine sand and gravel material pneumatic conveyor requires careful consideration of several engineering factors. Material properties, such as particle size, density, and moisture content, influence the system's design and operation. For example, finer particles may require higher air velocities to prevent settling, while larger particles may need different pipeline diameters and pressure settings. The system's components, including the air compressor, pipelines, and feeders, must be selected to withstand the specific conditions of the material being handled. Maintenance is also an important aspect of pneumatic conveyor operation, as regular checks of air pressure, material flow, and component wear are necessary to ensure continuous and efficient operation. HeadPowder's equipment is designed with durability and ease of maintenance in mind, featuring accessible components and clear operational indicators that help in monitoring and upkeep.