

Working Principle and Features of a Potassium Carbonate Fertilizer Pneumatic Conveying System
At Shandong HeadPowder Engineering Co., Ltd., we specialize in providing advanced solutions for the efficient handling and transportation of potassium carbonate fertilizer. Our pneumatic conveying systems are designed to meet the demanding requirements of modern agricultural and industrial applications, ensuring reliable and cost-effective material transport. This article explores the working principle and key features of our potassium carbonate fertilizer pneumatic conveying systems, highlighting how they enhance operational efficiency and safety in fertilizer processing.
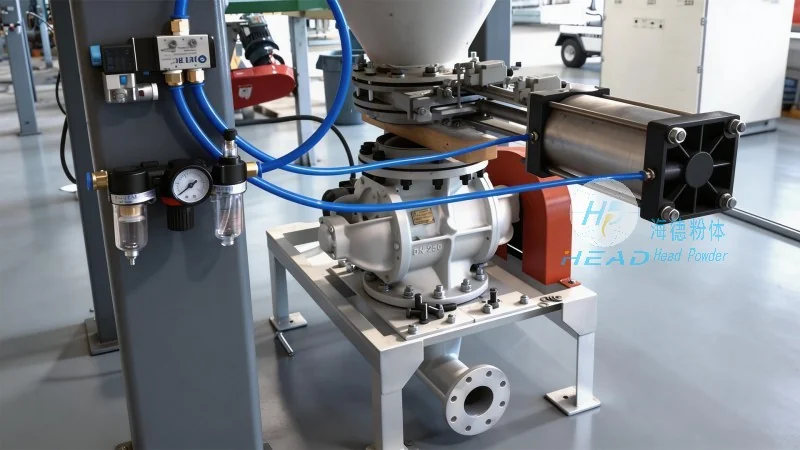
The Working Principle of the Pneumatic Conveying System
Our potassium carbonate fertilizer pneumatic conveying system operates on the principle of air-based material transport. The system utilizes a combination of positive and negative pressure to move the fertilizer from the storage silo or hopper to the discharge point. The process begins with the material being fed into the system via a hopper or feeder. An air compressor generates the necessary air pressure, which is then directed into the conveying line. As the air flows through the pipeline, it creates a flow that lifts and transports the fertilizer particles. The system typically includes components such as a blower, filter, and control valves to regulate the air flow and ensure consistent material movement. The design minimizes the need for mechanical components, reducing maintenance and operational costs while maintaining high material transfer efficiency. The system's ability to handle the specific characteristics of potassium carbonate, including its granular size and moisture content, ensures optimal performance and prevents material degradation during transport.
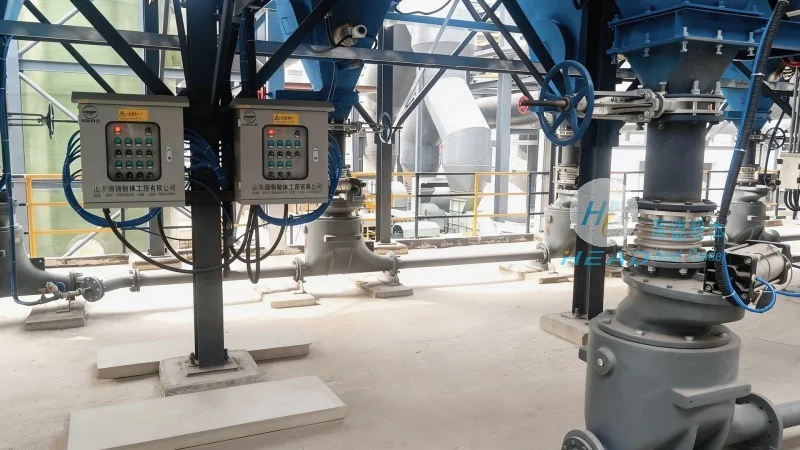
Key Features of the Potassium Carbonate Fertilizer Pneumatic Conveying System
Our pneumatic conveying system for potassium carbonate fertilizer offers several distinct advantages that set it apart from traditional mechanical conveying methods. Firstly, it provides a dust-free and hygienic environment, which is crucial for maintaining the quality of the fertilizer and ensuring compliance with industry standards. The system is also highly flexible, allowing for easy integration into existing production lines and adaptation to different operational conditions. Another notable feature is its energy efficiency, as it minimizes energy consumption compared to other transport methods, leading to lower operational costs. Additionally, the system is designed for low maintenance, with components that are easy to access and replace, reducing downtime and enhancing overall productivity. The system's ability to handle varying particle sizes and moisture content of potassium carbonate fertilizer makes it a versatile solution for different applications, from small-scale to large industrial operations. Furthermore, the system incorporates advanced control technology, enabling precise regulation of air pressure and flow rates, which ensures consistent and reliable material transport. This technology also allows for real-time monitoring of the system's performance, facilitating quick adjustments and troubleshooting to maintain optimal operation.
Benefits and Applications
The implementation of our potassium carbonate fertilizer pneumatic conveying system brings numerous benefits to fertilizer manufacturers and agricultural operations. By reducing the reliance on manual handling and mechanical conveyors, the system enhances workplace safety by minimizing the risk of dust exposure and physical strain on workers. The efficient transport of fertilizer also improves production throughput, as the system can handle high volumes of material with minimal downtime. In agricultural settings, the system ensures that potassium carbonate fertilizer is delivered to fields in a uniform and consistent manner, promoting better crop yields and soil health. The system's adaptability to different fertilizer types and processing requirements makes it a valuable asset for both new and existing fertilizer production facilities. Overall, the combination of efficiency, safety, and cost-effectiveness makes our pneumatic conveying system an ideal choice for businesses looking to optimize their fertilizer handling processes.
Conclusion
Shandong HeadPowder Engineering Co., Ltd. offers a comprehensive range of potassium carbonate fertilizer pneumatic conveying systems that are engineered to deliver superior performance and reliability. By understanding the working principle and key features of these systems, users can make informed decisions about integrating advanced material handling solutions into their operations. The systems are designed to meet the specific needs of the fertilizer industry, providing a sustainable and efficient approach to transporting potassium carbonate fertilizer. With our commitment to quality and innovation, we continue to provide solutions that enhance operational efficiency and support the growth of the agricultural sector. Based in China, our company serves clients globally, delivering tailored pneumatic conveying systems that meet international standards and regulatory requirements.