

Working Principle and Features of Nanometer Calcium Carbonate Pneumatic Conveying System
Understanding the working principle and features of a nanometer calcium carbonate pneumatic conveying system is crucial for industries that rely on efficient material handling. This article provides a detailed overview of how such systems operate and the key characteristics that make them effective in transporting nanometer calcium carbonate.
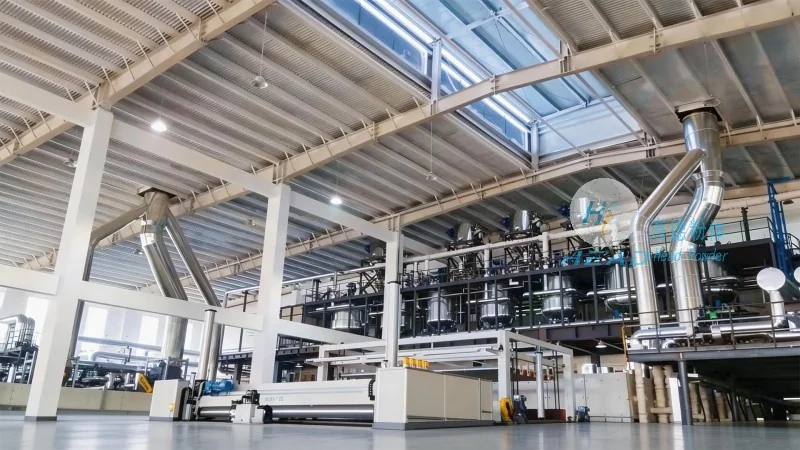
Working Principle of Nanometer Calcium Carbonate Pneumatic Conveying System
The core mechanism of a nanometer calcium carbonate pneumatic conveying system involves the use of air or gas to transport the material from the source to the destination. The system typically consists of a hopper, a blower or compressor, a pipeline network, and a receiver. The process begins when the nanometer calcium carbonate is fed into the hopper. The blower then generates a flow of air, which draws the material into the pipeline through a venturi or a rotary valve. As the air flows through the pipeline, it carries the fine particles of calcium carbonate, ensuring a consistent and controlled flow. The receiver at the end of the pipeline collects the material, separating it from the air using a filter or cyclone. This method eliminates the need for mechanical components like belts or buckets, reducing maintenance and increasing operational efficiency.
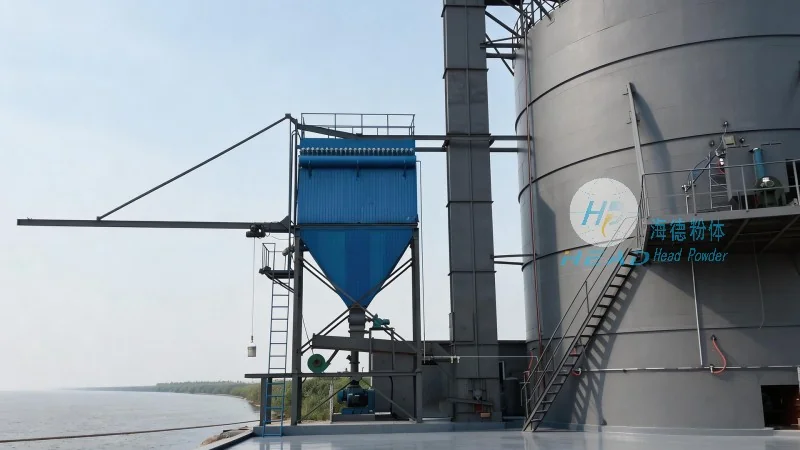
Key Features of the Nanometer Calcium Carbonate Pneumatic Conveying System
Several notable features distinguish the nanometer calcium carbonate pneumatic conveying system from traditional methods. Firstly, it offers a high degree of cleanliness and hygiene, which is essential for industries where contamination must be minimized, such as food processing or pharmaceuticals. The enclosed system prevents dust and particles from escaping into the environment, maintaining a safe and controlled workspace. Secondly, the system provides excellent flexibility in terms of layout and installation. The pipeline can be easily routed around obstacles, and the system can be scaled up or down to accommodate varying production needs. This adaptability makes it suitable for both small-scale and large-scale operations. Thirdly, the system is highly efficient in terms of energy consumption. By using air as the conveying medium, it reduces the need for heavy machinery and reduces energy costs compared to traditional mechanical conveyors. Additionally, the system offers a low maintenance requirement, as there are fewer moving parts involved, which translates to lower operational costs and increased uptime. Finally, the system ensures consistent material flow and quality control. The controlled air flow and particle size distribution result in a uniform product delivery, which is critical for maintaining product quality and meeting customer specifications.
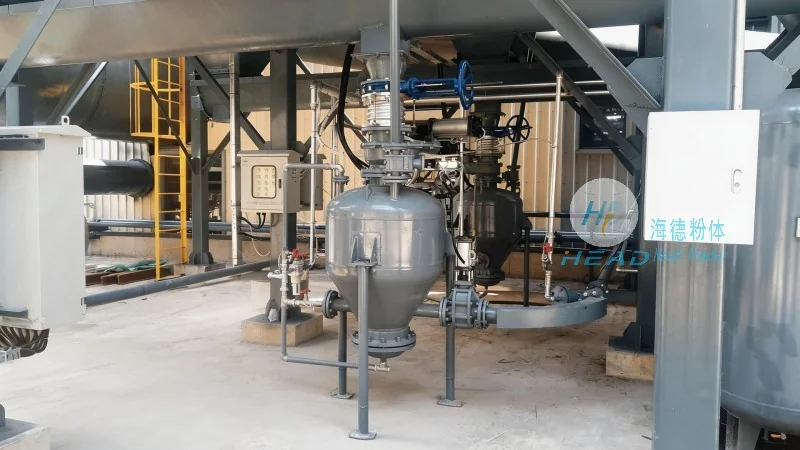
Application and Benefits in Industrial Settings
The nanometer calcium carbonate pneumatic conveying system is widely used in various industrial applications where the handling of fine powders is required. For instance, in the manufacturing of plastics, rubber, and coatings, the system efficiently transports the calcium carbonate filler to the processing equipment. In the paper industry, it is used to add calcium carbonate to the pulp, improving the paper's whiteness and strength. The system's ability to handle nanometer-sized particles is particularly advantageous, as these particles are often difficult to transport using conventional methods due to their tendency to agglomerate or clog equipment. The system's features, such as the enclosed design and low maintenance, make it an ideal choice for industries that prioritize product quality and operational efficiency. By leveraging the advantages of pneumatic conveying, companies can enhance their production processes, reduce costs, and improve overall productivity.
About Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., operating under the brand name headpowder, is a leading provider of advanced material handling solutions. With a focus on innovation and quality, the company specializes in designing and manufacturing pneumatic conveying systems tailored to the specific needs of various industries. Headpowder's expertise lies in understanding the unique challenges of transporting fine powders like nanometer calcium carbonate and developing solutions that address these challenges effectively. The company's commitment to customer satisfaction and technological advancement has made it a trusted partner for businesses seeking reliable and efficient material handling systems. Headpowder's systems are engineered to meet the highest standards of performance, safety, and durability, ensuring long-term operational success for its clients. Based in Shandong, China, the company leverages its local resources and industry knowledge to deliver cutting-edge solutions that drive industrial progress.