Understanding the working principle and features of nitrile rubber powder conveying systems is crucial for industries that handle this specialized material. Nitrile rubber, known for its excellent resistance to oil, fuel, and chemicals, is widely used in automotive, aerospace, and industrial applications. The efficient and safe transportation of nitrile rubber powder from storage to processing units is essential to maintain product quality and operational efficiency.
Working Principle of Nitrile Rubber Powder Conveying Systems
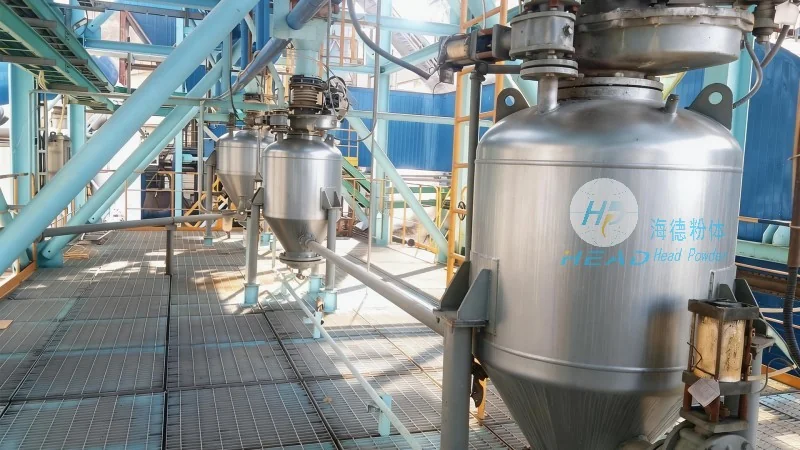
The working principle of nitrile rubber powder conveying systems revolves around the efficient transfer of fine or granular nitrile rubber particles from a storage hopper to processing equipment. These systems are engineered to handle the unique challenges posed by nitrile rubber, including its tendency to stick to surfaces and its sensitivity to moisture. The process typically begins with the nitrile rubber powder being loaded into a hopper, which is equipped with a level indicator to monitor the material volume. A feeder, such as a rotary valve or a vibratory feeder, then regulates the flow rate of the powder into the conveyor system. The conveyor, which can be either pneumatic or mechanical, transports the powder through a network of pipelines or troughs. Pneumatic conveying systems use compressed air to create a pressure differential that moves the powder, while mechanical systems rely on rotating screws or belts to push the material forward. The control unit, often a programmable logic controller (PLC), monitors key parameters such as pressure, flow rate, and temperature, and adjusts the system settings in real-time to maintain optimal performance. This closed-loop control ensures that the nitrile rubber powder is conveyed smoothly without blockages or uneven flow. The system also includes safety features like pressure relief valves and overfill protection to prevent accidents and protect the equipment.
Key Features of Nitrile Rubber Powder Conveying Systems
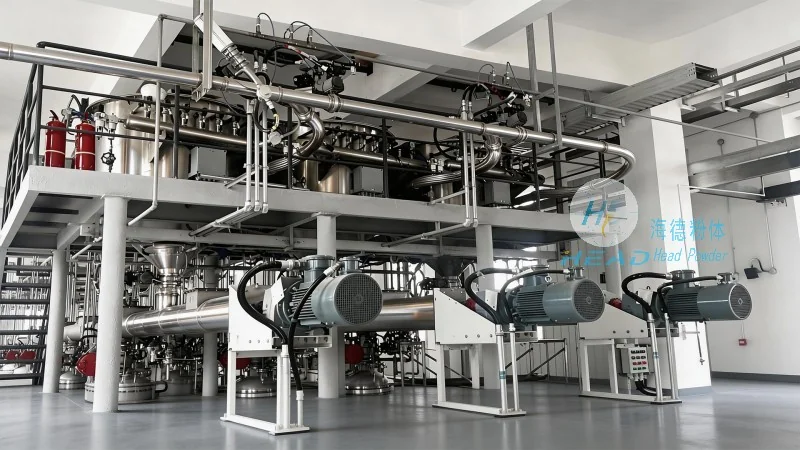
HeadPowder Engineering Co., Ltd., a leading manufacturer based in Shandong, China, offers advanced nitrile rubber powder conveying systems with several key features that enhance performance and reliability. The company's systems are characterized by robust and corrosion-resistant construction, made from high-quality stainless steel and other materials that can withstand the abrasive and chemical properties of nitrile rubber powder, ensuring long-term durability and minimal maintenance. The advanced control technology, based on PLC systems, provides precise and real-time monitoring of the conveying process. Operators can adjust parameters such as flow rate, pressure, and speed to optimize the system for different powder types and production requirements, improving efficiency and reducing downtime. Integrated safety features, including dust suppression mechanisms and overload protection, minimize risks and ensure compliance with industrial safety standards. The modular design allows for easy integration with existing production lines, reducing installation time and costs. These features collectively make HeadPowder's systems a preferred choice for industries demanding high performance and reliability.
Benefits of Using Nitrile Rubber Powder Conveying Systems
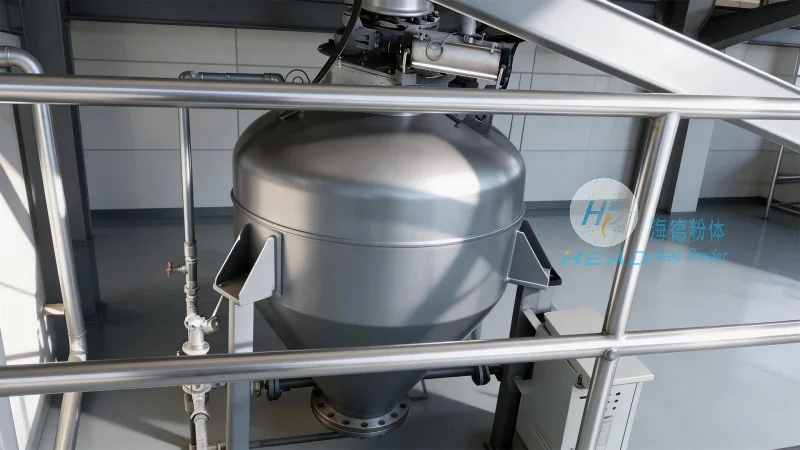
Implementing nitrile rubber powder conveying systems brings numerous benefits to industrial operations. Firstly, these systems significantly improve material handling efficiency by reducing manual labor and minimizing downtime. The automated feeding and conveying processes ensure a consistent and continuous flow of nitrile rubber powder, which is critical for maintaining production schedules, especially in high-volume manufacturing environments. Secondly, the systems enhance product quality by preventing contamination and maintaining the purity of the nitrile rubber powder. This is particularly important in applications where the material is used in high-value products, such as automotive seals, aerospace components, or industrial gaskets, where even minor impurities can affect performance and safety. Thirdly, the advanced control features help reduce energy consumption and operating costs. By optimizing the flow rate and pressure, the systems minimize energy waste and lower the overall operational expenses. This is especially beneficial in industries where energy costs are a significant portion of the total production cost. Finally, the safety features integrated into the design protect operators from potential hazards, such as dust explosions or material spills, creating a safer working environment. These benefits collectively contribute to increased productivity, reduced costs, and improved overall operational performance, making nitrile rubber powder conveying systems a valuable investment for any industrial facility.




