Understanding the working principle and features of tote bag packing powder handling equipment is crucial for industries dealing with bulk powders. This equipment is designed to efficiently transport, store, and dispense powder materials in large quantities, typically using tote bags as the primary container. The following sections will delve into the core mechanisms and key characteristics that define this technology.
Working Principle of Tote Bag Packing Powder Handling Equipment
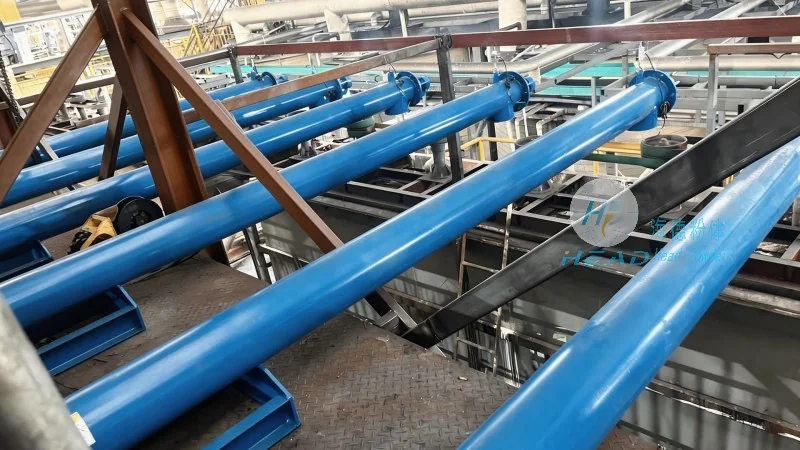
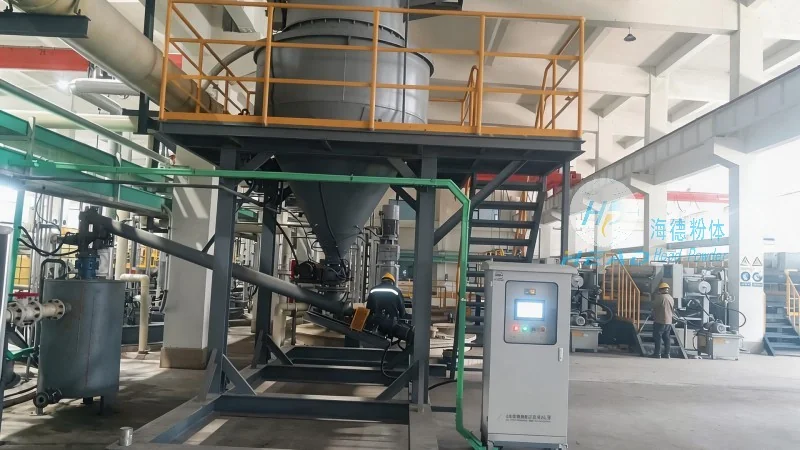
The working principle of tote bag packing powder handling equipment revolves around a systematic process that ensures safe and efficient handling of bulk powders. The equipment typically includes several key components: a hopper for material feeding, a conveyor system for transporting the powder, and a tote bag filling mechanism. The process begins when the powder is fed from a storage silo or hopper into the equipment. The powder then moves through a conveyor, which may be a screw conveyor or a belt conveyor, to the filling station. At the filling station, the tote bag is positioned under a filling head, and the powder is discharged into the bag under controlled pressure and flow rate. This controlled filling process minimizes dust generation and ensures accurate weight measurement, which is critical for maintaining product quality and compliance with industry standards. After filling, the tote bag is sealed and prepared for transport or storage. The entire process is often automated, with sensors and controls monitoring the flow rate, pressure, and bag position to ensure consistent performance. This automation not only enhances efficiency but also reduces the risk of human error, making it suitable for high-volume production environments.
Key Features of Tote Bag Packing Powder Handling Equipment
Tote bag packing powder handling equipment offers several notable features that make it an ideal solution for bulk powder handling applications. One of the primary features is its ability to handle a wide range of powder types, from fine powders to bulkier granules, without causing segregation or degradation. The equipment is designed with dust-tight enclosures and sealed conveyor systems to prevent powder spillage and contamination, which is essential for maintaining product purity and safety. Another key feature is the precision filling capability, which allows for accurate weight control, often with a tolerance of ±0.5% or better. This precision is achieved through advanced flow control technology, such as variable speed drives and pressure regulators, that adjust the flow rate based on the powder characteristics and bag size. The equipment also includes safety features, such as emergency stop buttons, interlocked access panels, and dust extraction systems, to protect operators and the environment. Additionally, many models are equipped with data logging and reporting capabilities, enabling users to track production metrics, maintenance schedules, and material usage. This data-driven approach helps in optimizing operations and reducing downtime. The modular design of the equipment allows for easy integration with existing production lines and future expansion, providing flexibility for growing businesses. Furthermore, the use of high-quality materials, such as stainless steel and food-grade components, ensures durability and compliance with hygiene standards, making it suitable for industries like food, pharmaceuticals, and chemicals.
Application and Benefits in Industrial Settings
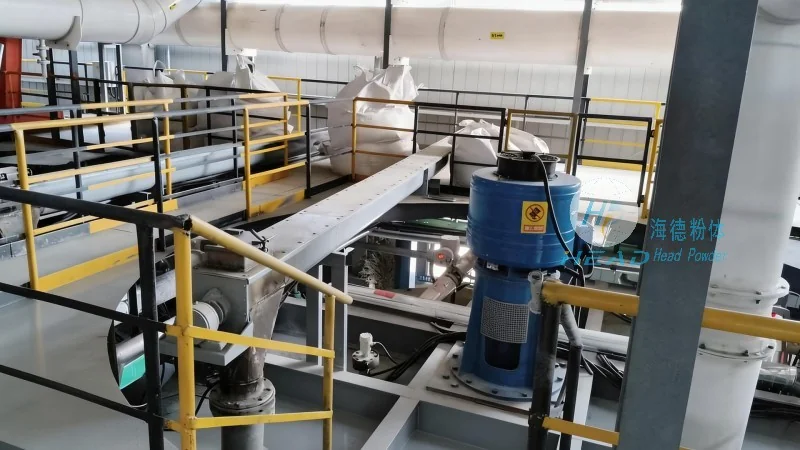
The tote bag packing powder handling equipment is widely used in various industrial sectors due to its versatility and efficiency. In the food industry, it is used for handling ingredients like flour, sugar, and spices, where maintaining product quality and preventing contamination is paramount. The pharmaceutical industry relies on this equipment for handling active pharmaceutical ingredients (APIs) and excipients, where precision and cleanliness are critical to ensure product safety and efficacy. The chemical industry uses it for transporting bulk chemicals, such as fertilizers and pigments, where accurate dosing and dust control are essential. The benefits of using this equipment include increased productivity through automated processes, reduced labor costs due to minimal manual intervention, and improved product quality through precise filling and dust control. Additionally, the equipment helps in reducing material waste by minimizing overfilling and spillage, which can lead to significant cost savings over time. The compact design of many models allows for installation in limited spaces, making it suitable for facilities with space constraints. The durability of the equipment, with components designed to withstand heavy usage and harsh environments, ensures long-term reliability and low maintenance costs. Overall, the tote bag packing powder handling equipment provides a reliable and efficient solution for bulk powder handling, contributing to improved operational efficiency and product quality in various industrial applications.




