For industrial facilities dealing with bulk materials, efficient material handling is crucial for operational efficiency and productivity. Floor hopper conveying systems represent a specialized solution designed to address the challenges of transporting materials from storage areas to processing or packaging stages. These systems are integral to modern material handling operations, offering a reliable and cost-effective method for moving large volumes of bulk materials.
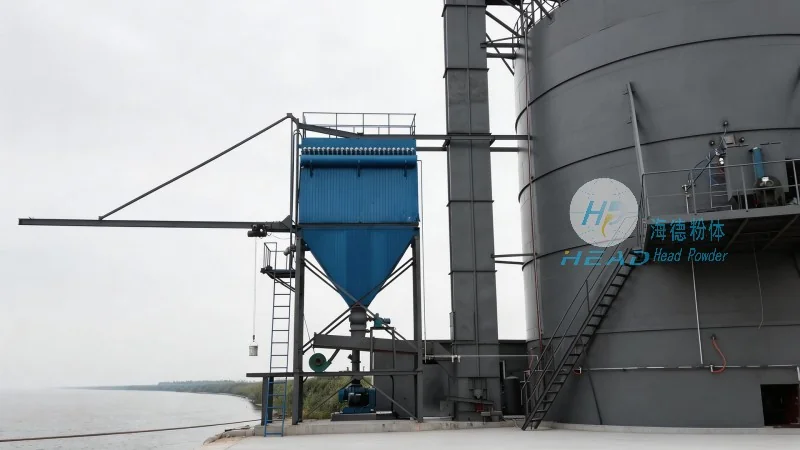
Working Principle of Floor Hopper Conveying Systems
The core operation of a floor hopper conveying system involves several key components and processes. At its foundation, the system typically includes a hopper, which serves as the storage and feeding unit for bulk materials. The hopper is strategically positioned at the bottom of a vertical or inclined section, allowing materials to flow under gravity or with minimal mechanical assistance. As materials enter the hopper, they accumulate and are then discharged through a controlled outlet, often via a conveyor or chute that directs the flow to the next stage of the process. The system may incorporate mechanisms such as vibrators or feeders to regulate the flow rate, ensuring consistent and controlled material delivery. This controlled discharge minimizes material spillage and optimizes the transfer efficiency, making it suitable for a wide range of industrial applications.
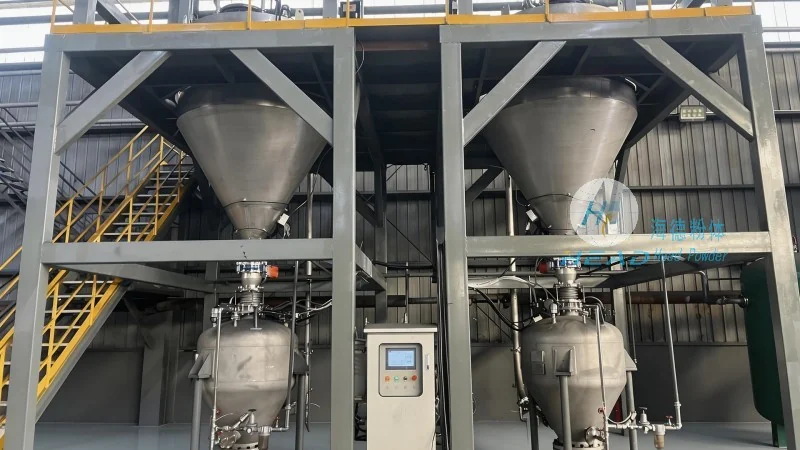
Key Features of Floor Hopper Conveying Systems
HeadPowder Engineering Co., Ltd. specializes in the design, manufacturing, and installation of advanced floor hopper conveying systems, tailored to meet the specific needs of various industries. The key features of these systems include: 1. **Space Efficiency**: By utilizing the floor space effectively, these systems minimize the footprint required for material handling, making them ideal for facilities with limited vertical or horizontal space. 2. **Low Maintenance Requirements**: The robust construction and simple mechanical design reduce the need for frequent maintenance, leading to lower operational costs and increased system reliability. 3. **Versatility in Material Handling**: The systems are adaptable to handle a wide variety of bulk materials, including powders, granules, and small particles, with customizable hopper designs to accommodate different material characteristics. 4. **Energy Efficiency**: The use of gravity-assisted flow and minimal mechanical components contributes to lower energy consumption compared to traditional conveyor systems, enhancing overall operational efficiency. 5. **Safety and Compliance**: The design adheres to industrial safety standards, ensuring safe material handling and compliance with regulatory requirements. These features collectively make floor hopper conveying systems a preferred choice for industries seeking reliable, efficient, and cost-effective material transfer solutions.
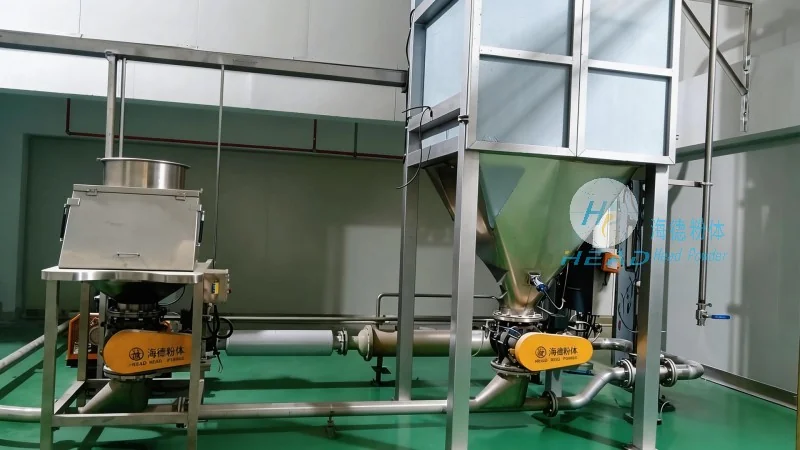
Applications and Benefits in Industrial Settings
Floor hopper conveying systems are widely used across various industrial sectors, including food processing, pharmaceuticals, chemicals, and mining. In food processing facilities, they are employed to transfer raw ingredients or finished products from storage to production lines, ensuring hygienic and efficient material flow. In the pharmaceutical industry, the systems are crucial for handling active pharmaceutical ingredients (APIs) and other sensitive materials, where contamination control and precise dosing are paramount. The chemical industry utilizes these systems for transporting bulk chemicals, powders, and reagents, while the mining sector benefits from their ability to handle abrasive and heavy materials. The benefits of these systems extend beyond material handling, as they contribute to improved production throughput, reduced labor costs, and enhanced safety in the workplace. By integrating floor hopper conveying systems into their operations, companies can achieve significant improvements in operational efficiency and overall productivity.




