For industrial operations that require efficient and reliable material handling, the silo-based bulk powder pneumatic conveying system stands out as a critical solution. This technology is designed to transport dry powders and granular materials from storage silos to processing units, ensuring smooth and controlled material flow. Understanding the working principle and key features of such systems is essential for optimizing production processes and enhancing operational efficiency.
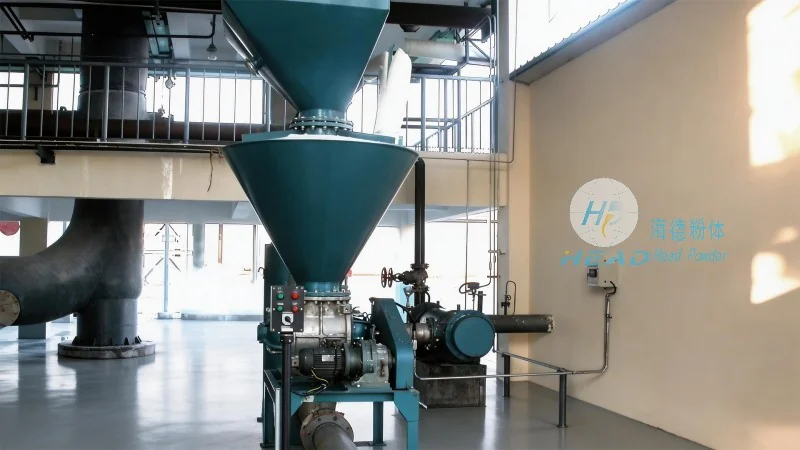
Overview of Silo Bulk Powder Pneumatic Conveying Systems
The silo bulk powder pneumatic conveying system is a specialized equipment setup that integrates storage silos with pneumatic conveying technology. It typically consists of a silo for material storage, a conveying line (often using air or other gases as the conveying medium), and control systems to regulate the flow of materials. The system is engineered to handle various types of powders, including fine powders, bulk powders, and granules, with minimal loss and contamination. This setup is widely used in industries like pharmaceuticals, food processing, chemicals, and mining, where precise material handling is paramount.
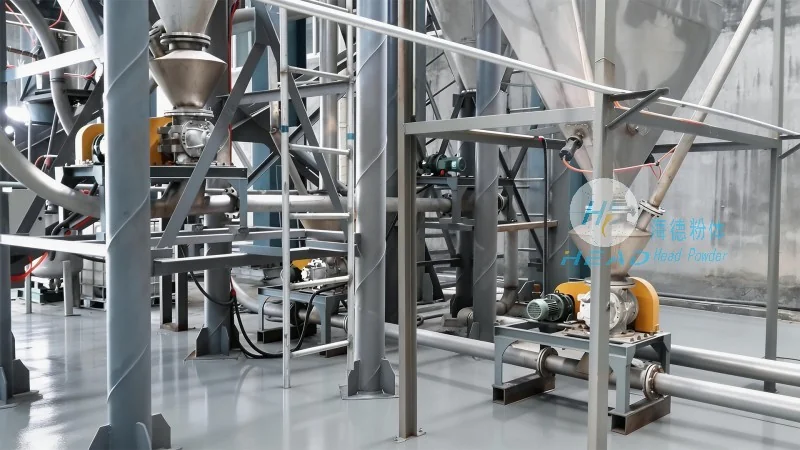
The Working Principle of the System
The core of the silo bulk powder pneumatic conveying system lies in its pneumatic conveying mechanism. The process begins with the material being drawn from the silo through a hopper or a feeder. A vacuum or pressure is then applied to the conveying line, creating a flow of air that carries the powder particles along the pipeline. The system utilizes either positive pressure (where air is forced into the line) or negative pressure (where air is drawn out), depending on the specific application and material characteristics. The conveying line is equipped with components like filters, cyclones, and separators to ensure that the material is transported efficiently while preventing dust and air from escaping into the environment. The control system monitors the pressure, flow rate, and material level in real-time, allowing for adjustments to maintain optimal performance.
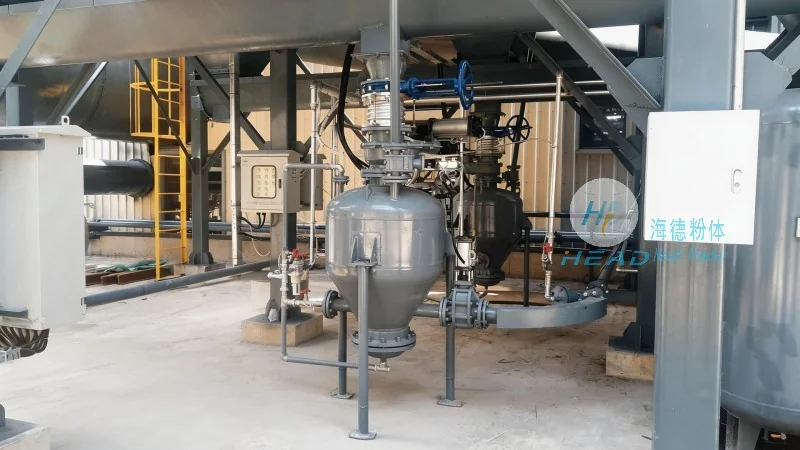
Key Features and Advantages
Several distinct features make the silo bulk powder pneumatic conveying system a preferred choice for industrial material handling. Firstly, it offers a closed system, which minimizes dust emissions and ensures environmental compliance. This is particularly important in industries where air quality regulations are strict. Secondly, the system provides high flexibility in terms of material transport, as it can handle materials with varying particle sizes and moisture content. The ability to transport materials over long distances without the need for mechanical components like conveyors or elevators reduces maintenance costs and operational downtime. Additionally, the system is designed for scalability, allowing it to be customized to meet the specific needs of different production capacities. The integration of advanced control systems enables precise control over the conveying process, ensuring consistent material delivery to downstream processes. Another notable feature is the system's ability to handle abrasive materials without significant wear and tear, thanks to the use of durable materials in the construction of the conveying line and components.
Applications and Operational Benefits
The silo bulk powder pneumatic conveying system is applied in a wide range of industrial processes where efficient powder handling is critical. In the pharmaceutical industry, it is used to transport active pharmaceutical ingredients (APIs) and excipients from storage silos to mixing and packaging units, ensuring that the materials remain sterile and free from contamination. In food processing, the system is employed to handle ingredients like flour, sugar, and spices, maintaining product quality and safety standards. The chemical industry utilizes this technology for transporting raw materials and intermediates, while the mining sector applies it to move ore and other bulk materials from storage to processing facilities. The operational benefits of this system include improved safety due to the closed system, reduced labor costs as it automates the material handling process, and enhanced product quality through consistent material flow and minimal contamination. Furthermore, the system's energy efficiency, as it uses air as the primary conveying medium, contributes to lower operational costs over time.
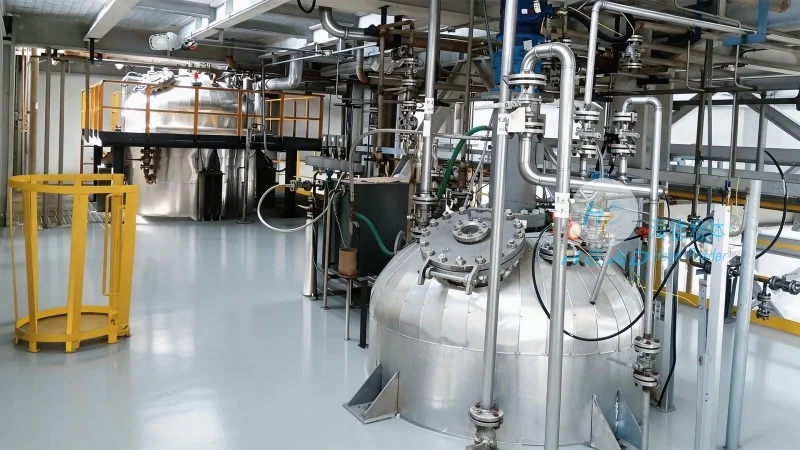
Customization and Integration with HeadPowder Engineering
Shandong HeadPowder Engineering Co., Ltd. specializes in designing and manufacturing customized silo bulk powder pneumatic conveying systems tailored to the unique requirements of each client. With a focus on innovation and quality, HeadPowder offers comprehensive solutions that integrate seamlessly with existing industrial setups. The company's engineers work closely with clients to understand their specific material handling challenges and develop systems that optimize performance and efficiency. The customization process includes selecting the appropriate silo size and material, designing the conveying line with suitable components like filters and separators, and integrating advanced control systems for real-time monitoring. HeadPowder's commitment to using high-quality materials and adhering to international standards ensures that their systems are durable, reliable, and meet the stringent requirements of various industries. The company's location in Shandong, China, provides a strategic advantage in terms of access to manufacturing resources and expertise, enabling them to deliver efficient and cost-effective solutions to clients worldwide.




