For industrial applications requiring the efficient and reliable transport of magnesium sulfate heptahydrate powder, the pneumatic conveying system offers a sophisticated solution. This article explores the working principle and key features of such a system, highlighting its advantages and operational efficiency.
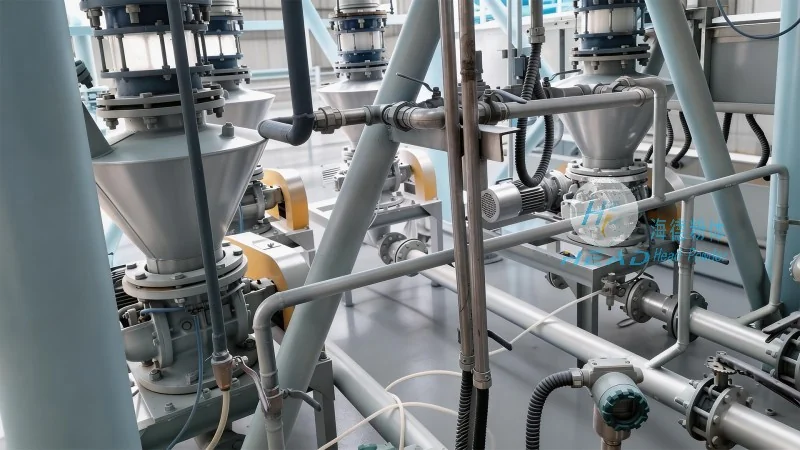
Overview of the Magnesium Sulfate Heptahydrate Powder Pneumatic Conveying System
The magnesium sulfate heptahydrate powder pneumatic conveying system is designed to handle the transportation of this specific chemical powder from a storage or processing point to a destination, such as a processing unit or storage silo. The system operates by using compressed air or other gas to move the powder through a pipeline network, eliminating the need for mechanical components like conveyors or buckets that might cause contamination or wear.
Working Principle of the Pneumatic Conveying System
The core mechanism of the pneumatic conveying system involves the creation of a pressure differential within the pipeline. Compressed air is introduced into the system, typically at the inlet where the powder is fed. This air flow generates sufficient velocity to entrain the powder particles, lifting them from the hopper or feeder and propelling them through the pipeline. The system may employ different conveying modes, including dilute-phase and dense-phase, depending on the material characteristics and required transport distance.
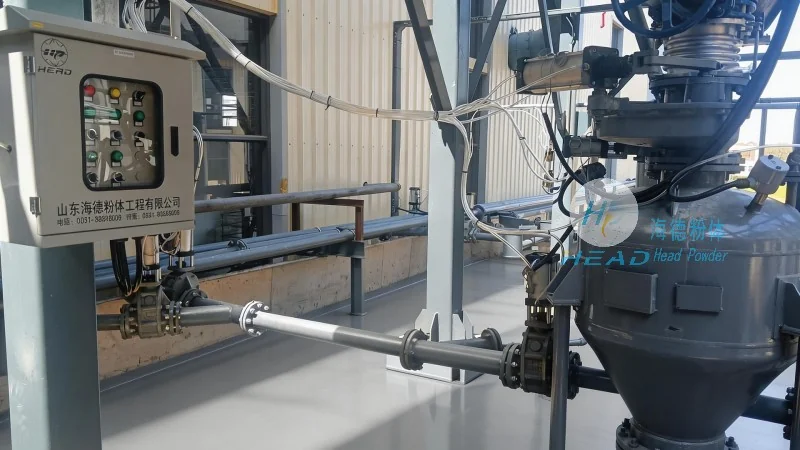
In the dilute-phase mode, the air-to-powder ratio is high, and the particles are suspended in the air stream, moving at high velocity. This mode is suitable for short to medium distances and low to moderate powder loads. In contrast, the dense-phase mode uses a lower air flow rate, resulting in a higher powder concentration in the pipeline. This mode is ideal for longer distances or when handling materials that are prone to bridging or segregation.
Key Features and Advantages
The magnesium sulfate heptahydrate powder pneumatic conveying system from Shandong HeadPowder Engineering Co., Ltd. (commonly known as headpowder) incorporates several key features that enhance performance and reliability:
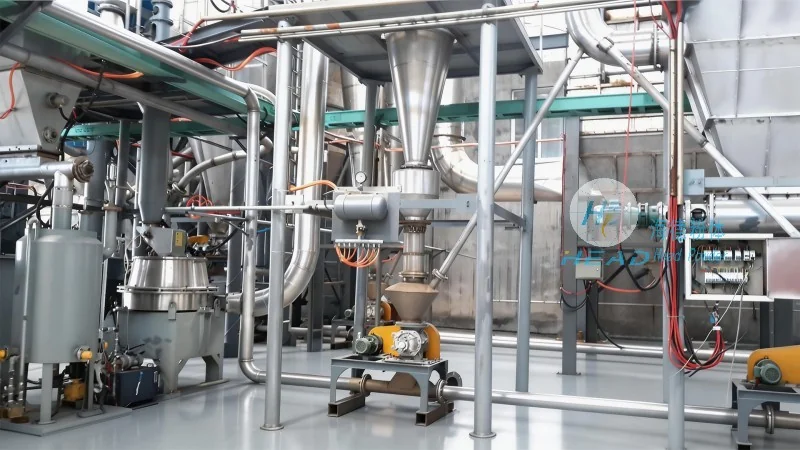
- Hygienic and Clean Design: The system is constructed with materials that meet sanitary standards, ensuring that the powder remains free from contamination during transport. This is crucial for applications in the pharmaceutical or food industries where product purity is paramount.
- Energy Efficiency: By utilizing compressed air, the system minimizes energy consumption compared to traditional mechanical conveying methods. The design optimizes air usage, reducing operational costs while maintaining high transport efficiency.
- Flexibility in Pipeline Layout: The pneumatic conveying system can be configured with multiple branches and curves, allowing for complex pipeline layouts that adapt to the specific spatial constraints of a facility. This flexibility ensures that the system can be integrated seamlessly into existing or new plant layouts.
- Low Maintenance Requirements: With fewer moving parts compared to mechanical conveyors, the pneumatic system requires less maintenance, reducing downtime and maintenance costs over the system's lifecycle.
- Controlled Flow and Dosing: Advanced control systems enable precise regulation of the powder flow rate and pressure, ensuring consistent and accurate delivery of the magnesium sulfate heptahydrate powder to the destination. This is essential for processes that demand tight control over material input.
Application Considerations
When implementing a magnesium sulfate heptahydrate powder pneumatic conveying system, several factors should be considered to ensure optimal performance:
- Powder Properties: The particle size, density, and flowability of the magnesium sulfate heptahydrate powder influence the choice of conveying mode and system design. For example, fine powders may require higher air velocities to prevent clogging, while cohesive powders may benefit from the dense-phase mode to maintain flow.
- Transport Distance and Height: The distance and vertical height the powder needs to be conveyed affect the system's pressure requirements and air flow rate. Longer or higher lifts may necessitate additional boosters or higher pressure levels.
- Environmental and Safety Compliance: The system must comply with local regulations regarding dust control and air emissions. Proper filtration and ventilation are essential to maintain a safe working environment and prevent dust accumulation.
Conclusion
The magnesium sulfate heptahydrate powder pneumatic conveying system from Shandong HeadPowder Engineering Co., Ltd. represents a reliable and efficient solution for the transport of this chemical powder. By leveraging pneumatic technology, the system offers advantages such as hygienic operation, energy efficiency, and flexibility, making it suitable for a wide range of industrial applications. With its robust design and advanced features, the system ensures consistent performance and minimal maintenance, contributing to overall operational efficiency in processing facilities.




