For industrial applications involving the transport of bulk materials such as coal gangue and limestone, air-pneumatic conveying equipment offers an efficient and reliable solution. This article explores the working principle and key features of such equipment, providing insights into its functionality and benefits for material handling processes.
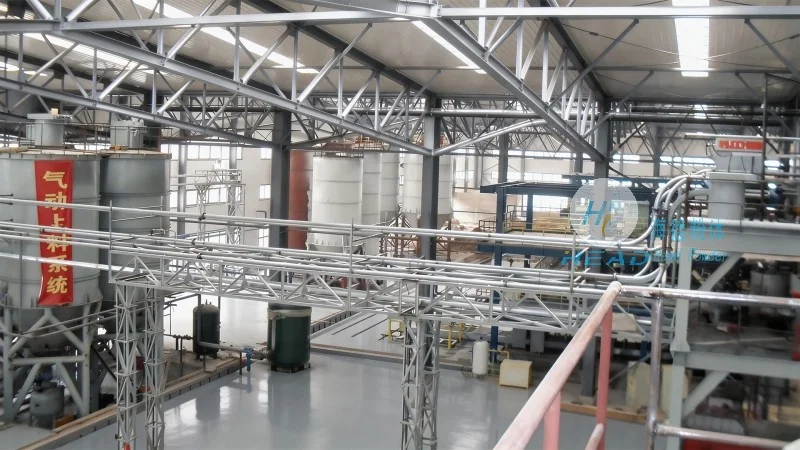
Company Profile: Shandong HeadPowder Engineering Co., Ltd.
HeadPowder, a leading manufacturer in the field of bulk material handling systems, specializes in designing and manufacturing air-pneumatic conveying equipment tailored to the needs of various industries. With a strong commitment to quality and innovation, the company has established itself as a trusted partner for clients seeking advanced solutions for material transport and processing. HeadPowder's headquarters is located in Shandong, China, where the company's research and development team continuously works on improving the performance and efficiency of its products.
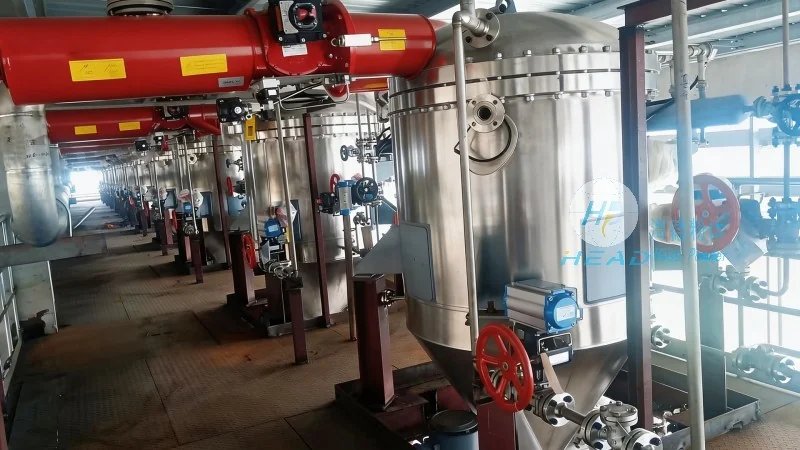
Working Principle of the Air-Pneumatic Conveying Equipment
The air-pneumatic conveying system operates by using compressed air to transport bulk materials through a pipeline network. The process begins with the material being fed into a hopper or feeder, where it is then drawn into the conveying line by the pressure differential created by the air flow. The compressed air, typically supplied by an air compressor, creates a flow that propels the material particles through the pipeline. The system can be configured in various modes, including positive pressure, negative pressure, or a combination of both, depending on the specific requirements of the material and the application. The design of the equipment ensures that the material is transported smoothly and efficiently, minimizing wear and tear on the components and reducing the risk of blockages or clogging.
Key Features of the Air-Pneumatic Conveying System
One of the primary features of the air-pneumatic conveying equipment is its ability to handle a wide range of materials, including coal gangue and limestone, which are often characterized by their abrasive and dusty nature. The system is designed with robust components that can withstand the harsh conditions associated with these materials, ensuring long-term reliability and minimal maintenance. Another key feature is the flexibility in system configuration, allowing for customized solutions that can adapt to different production scales and operational requirements. The equipment also offers high transport efficiency, with the ability to move large volumes of material over significant distances with minimal energy consumption. Additionally, the system provides a clean and safe working environment by containing dust and preventing material spillage, which is crucial for maintaining compliance with environmental regulations and ensuring workplace safety.
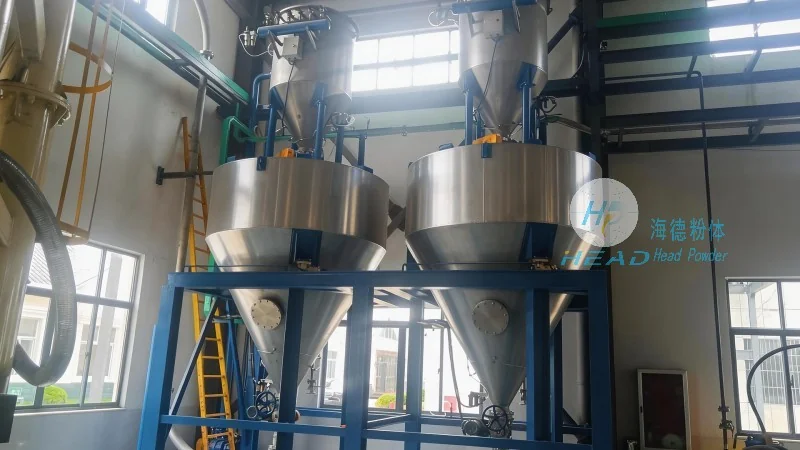
Technical Advantages in Material Handling
The air-pneumatic conveying system offers several technical advantages that make it an ideal choice for handling coal gangue and limestone. Firstly, the system provides a continuous and uniform flow of material, which helps in maintaining consistent production rates and reducing downtime. Secondly, the use of compressed air allows for the transport of materials in a closed system, preventing dust emissions and protecting the environment. This is particularly important for applications where dust control is a critical factor. Thirdly, the equipment is designed for easy integration with existing production lines, allowing for seamless incorporation into current operations without major modifications. The system also offers low maintenance requirements, with components that are easy to replace and service, reducing operational costs and increasing the overall productivity of the facility. Finally, the air-pneumatic conveying equipment provides precise control over the material flow, enabling operators to adjust the speed and volume of transport as needed to meet the specific demands of the process.




