For industries dealing with rare earth powders, efficient and reliable handling equipment is crucial for maintaining production efficiency and product quality. This article explores the principles and working scene characteristics of rare earth powder handling equipment, providing insights into how such systems operate and their applications in various industrial settings.
Introduction to Rare Earth Powder Handling Equipment
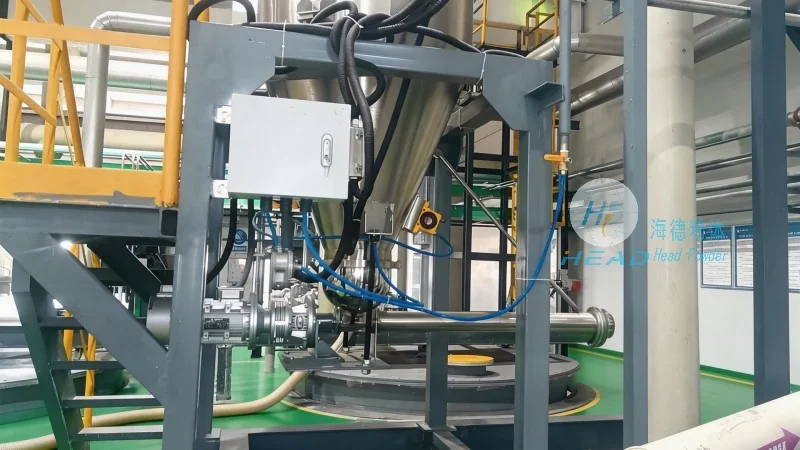
Rare earth powders are essential raw materials in modern manufacturing, used across sectors like electronics, aerospace, and renewable energy. The handling of these powders requires specialized equipment due to their unique properties, including fine particle size, high reactivity, and potential for dust generation. Proper handling not only ensures safety but also minimizes material loss and contamination, which are critical for maintaining product consistency and meeting regulatory standards. Companies like Shandong HeadPowder Engineering Co., Ltd. specialize in designing and manufacturing advanced powder handling solutions tailored to the specific needs of rare earth processing industries.
Principles of Rare Earth Powder Handling Equipment
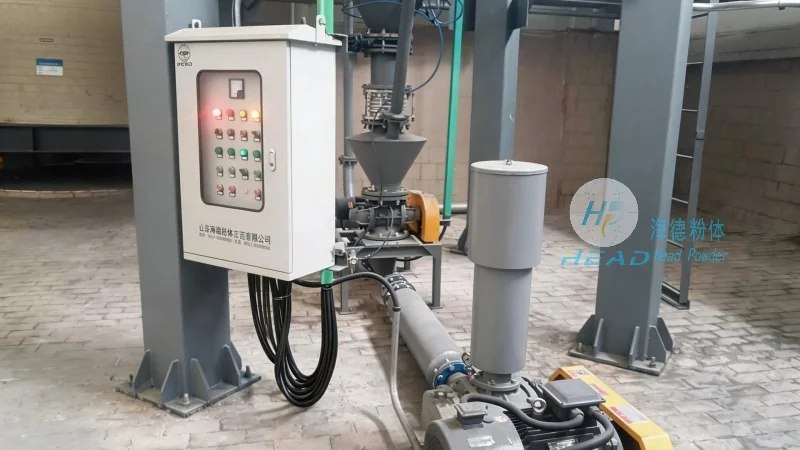
The core principle of rare earth powder handling equipment is to transport these materials in a controlled manner, minimizing agglomeration, segregation, and loss. Key components include feeders, conveyors, and storage systems, each designed to address the challenges posed by rare earth powders. For instance, screw feeders are commonly used to meter and feed powders into processing lines, while pneumatic conveying systems are employed for long-distance transport, especially in environments where dust control is paramount. The equipment must also be constructed from materials resistant to corrosion and wear, as rare earth powders can be abrasive and reactive with certain metals. Headpowder, as a leading manufacturer, integrates advanced technologies such as variable speed drives and intelligent control systems to optimize the handling process, ensuring consistent flow rates and preventing equipment downtime.
Working Scene Characteristics and Applications
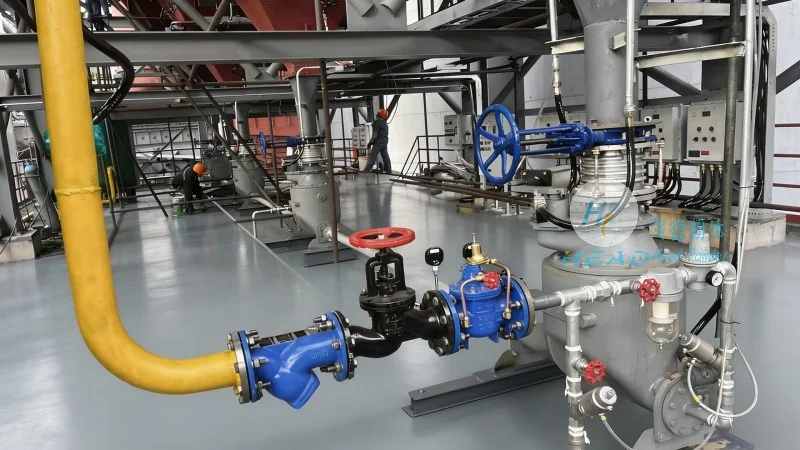
The working scene characteristics of rare earth powder handling equipment vary based on the specific industrial application. In mining and extraction facilities, the equipment is used to transport raw rare earth ores and intermediate products from crushing and grinding stages to subsequent processing units. Here, robust, high-capacity systems are essential to handle large volumes of material efficiently. In manufacturing plants, the focus shifts to precise dosing and feeding for downstream processes like sintering, smelting, or chemical processing. The equipment must be able to handle varying particle sizes and moisture content, which can affect flow properties. For example, in the production of rare earth magnets, the handling system must ensure uniform mixing and feeding of powders to maintain the magnetic properties of the final product. Additionally, in research and development laboratories, smaller-scale handling equipment is used for material testing and sample preparation, requiring high precision and minimal contamination. The versatility of rare earth powder handling equipment allows it to adapt to these diverse working scenes, from large-scale industrial production to laboratory-scale applications.
Key Features and Advantages
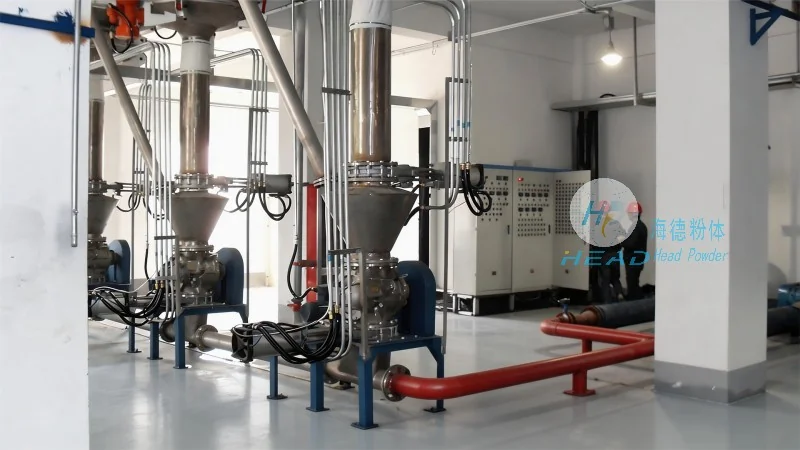
Modern rare earth powder handling equipment from companies like Shandong HeadPowder Engineering Co., Ltd. incorporates several key features that enhance performance and reliability. One of the primary advantages is the use of closed-loop systems, which minimize dust exposure and environmental impact, aligning with industrial safety and environmental regulations. The equipment is also designed for easy maintenance and cleaning, as rare earth powders can adhere to surfaces and require thorough sanitation to prevent cross-contamination. Advanced control systems, including sensors and automation, enable real-time monitoring of flow rates, pressure, and temperature, allowing operators to adjust settings dynamically and optimize the handling process. This not only improves efficiency but also reduces the risk of material degradation or equipment failure. Furthermore, the equipment is built with durability in mind, using high-quality materials and robust construction to withstand the harsh conditions associated with rare earth processing, such as high temperatures and abrasive particles. These features collectively contribute to the long-term reliability and cost-effectiveness of the handling systems, making them a valuable investment for any rare earth processing facility.
Conclusion
In conclusion, rare earth powder handling equipment plays a vital role in the efficient and safe processing of rare earth materials. By understanding the principles and working scene characteristics of these systems, industries can select and implement the most appropriate equipment to meet their specific needs. Companies like Shandong HeadPowder Engineering Co., Ltd. provide comprehensive solutions that address the unique challenges of rare earth powder handling, ensuring optimal performance, safety, and compliance. As the demand for rare earth materials continues to grow, the importance of reliable handling equipment will only increase, making it an essential component of modern manufacturing processes.




