For industries dealing with paper chips and similar bulk materials, efficient material handling is crucial for maintaining operational efficiency and product quality. The paper chip material conveying system, developed by Shandong HeadPowder Engineering Co., Ltd., addresses these needs through a combination of advanced engineering principles and practical application design. This article explores the core principles behind such systems and highlights key working scene characteristics that make them indispensable in modern material processing environments.
Core Principles of Paper Chip Material Conveying Systems
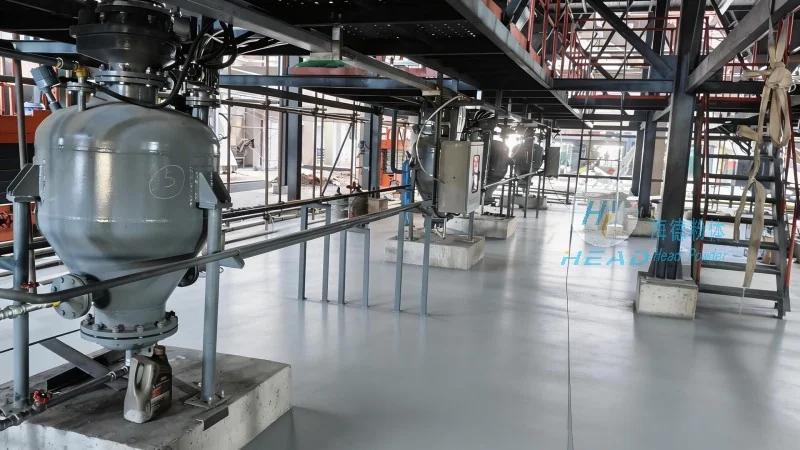
The fundamental principle of paper chip material conveying systems is to transport bulk materials, such as paper chips, efficiently from one location to another within a production facility. These systems typically utilize mechanical components like conveyor belts, rollers, or pneumatic mechanisms to move the material. The design focuses on minimizing material degradation, ensuring consistent flow rates, and optimizing energy consumption. By integrating precise control mechanisms, the system can adapt to varying material loads and environmental conditions, ensuring reliable operation. The engineering approach emphasizes durability and low maintenance, which are critical for continuous industrial operations.
Working Scene Characteristics and Applications
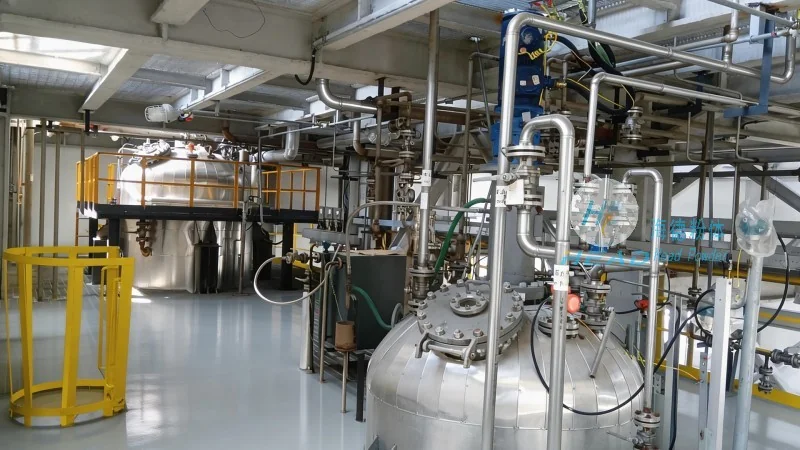
Paper chip material conveying systems are widely used in various industrial settings, including paper mills, recycling facilities, and manufacturing plants that process wood or paper-based products. The working scene characteristics vary based on the specific application, but common features include high-volume material handling, the need for gentle material handling to preserve product integrity, and integration with other production equipment. For example, in a paper mill, these systems may be used to transport raw paper chips from storage to processing machinery, ensuring a steady supply of material for paper production. In recycling facilities, they help move sorted paper chips to sorting or processing lines, supporting the recycling process. The adaptability of these systems allows them to be customized for different production scales and material types, making them versatile solutions for diverse industrial needs.
Key Features and Technical Advantages
Shandong HeadPowder Engineering Co., Ltd. designs paper chip material conveying systems with several key features that enhance performance and reliability. These include robust construction to withstand heavy loads and abrasive materials, advanced control systems for precise material flow regulation, and energy-efficient operation to reduce operational costs. The systems are also designed for easy maintenance, with accessible components that allow for quick repairs and replacements. Additionally, the integration of sensors and monitoring tools enables real-time tracking of material flow and system performance, allowing for proactive maintenance and optimization. The company’s expertise in material handling engineering ensures that each system is tailored to meet the specific requirements of the client, whether it's a small-scale operation or a large industrial facility.
Conclusion and Company Overview
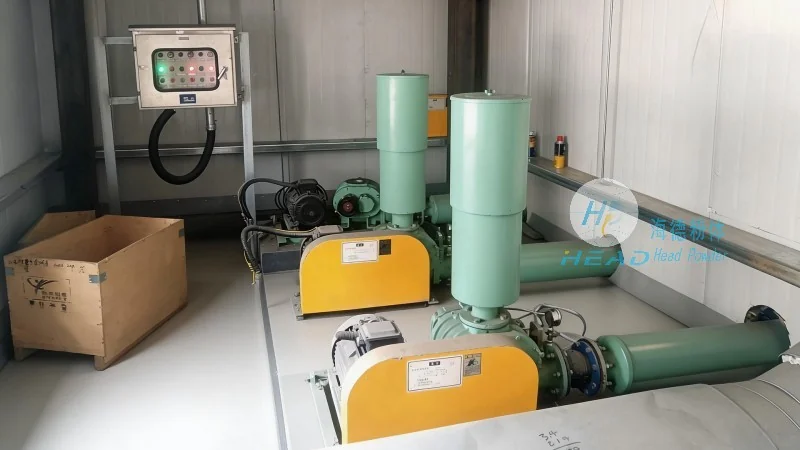
As a leading provider of material handling solutions, Shandong HeadPowder Engineering Co., Ltd. specializes in developing and manufacturing paper chip material conveying systems that meet the highest standards of efficiency and reliability. With a focus on customer-specific solutions and rigorous engineering, the company has established itself as a trusted partner in the industry. HeadPowder's systems are designed to enhance operational productivity while ensuring the integrity of the materials being transported. Based in Shandong, China, the company leverages its local expertise and resources to deliver high-quality products that meet the demands of modern industrial applications. Whether for new installations or system upgrades, HeadPowder's paper chip material conveying systems offer a reliable and efficient solution for material handling needs.




