HeadPowder, a leading manufacturer based in Shandong, China, specializes in providing advanced material handling solutions for industries requiring high precision and dust control. The company's core product, the tonne bag dust-free feeding station with material conveying system, is designed to address the challenges of handling bulk materials while maintaining a clean and safe working environment. This equipment is a critical component in facilities where material transfer needs to be efficient, hygienic, and compliant with stringent industry standards.
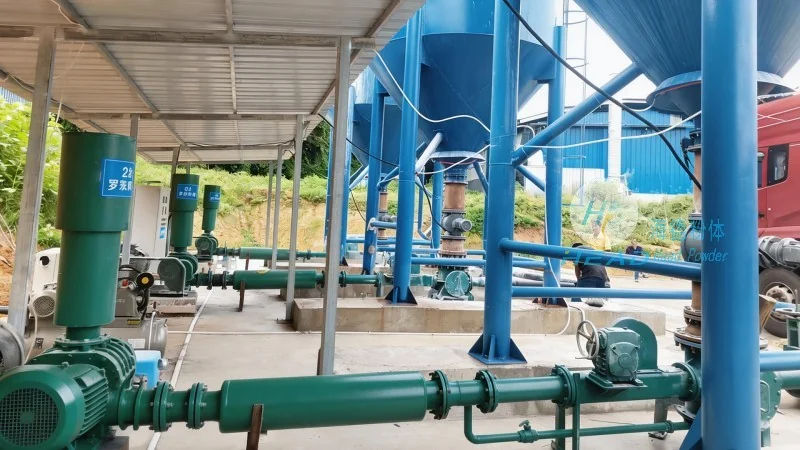
Overview of the Tonne Bag Dust-Free Feeding Station Material Conveying System
The tonne bag dust-free feeding station is an integrated system engineered to facilitate the seamless transfer of bulk materials from tonne bags into processing equipment. It combines advanced sealing technology, precise material flow control, and robust conveying mechanisms to ensure minimal dust generation and optimal material handling efficiency. The system is tailored to meet the demands of various industries, including chemical, pharmaceutical, food processing, and mining, where maintaining a dust-free environment is paramount.
Principle of Operation
The core principle of the tonne bag dust-free feeding station revolves around creating a sealed, negative-pressure environment that prevents dust particles from escaping into the surrounding air. When a tonne bag is placed on the feeding station, the system automatically seals the bag opening with a specialized lid or cover. As the material is discharged from the bag, it is drawn into a hopper or conveyor system through a controlled opening. The system uses a combination of vacuum or pressure differential to ensure that the material flows smoothly without creating excessive dust. The conveying mechanism, typically a screw conveyor or pneumatic system, transports the material to the next stage of processing while maintaining the sealed environment. This design minimizes exposure to airborne contaminants, protecting both personnel and equipment from dust-related issues.
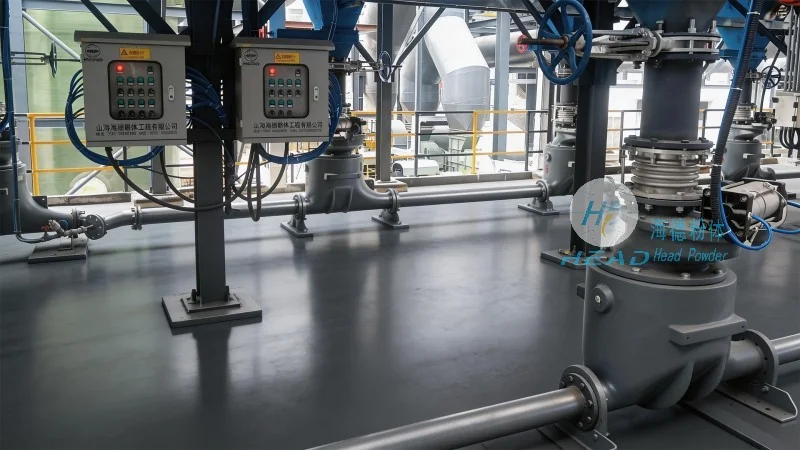
Key Working Scene Characteristics
The tonne bag dust-free feeding station exhibits several distinct characteristics that make it suitable for diverse industrial applications. Firstly, its dust control capabilities are superior, as the sealed design effectively contains particulate matter, reducing the risk of inhalation hazards and contamination of other materials. Secondly, the system offers high operational efficiency, with the ability to handle large volumes of material quickly and consistently. This is achieved through optimized flow rates and minimal downtime during bag changes. Thirdly, the equipment is designed for durability and ease of maintenance, featuring robust construction and user-friendly controls that reduce operational costs over time. Additionally, the system can be integrated with other processing equipment, such as mixers or reactors, to form a complete material handling line, enhancing overall productivity.
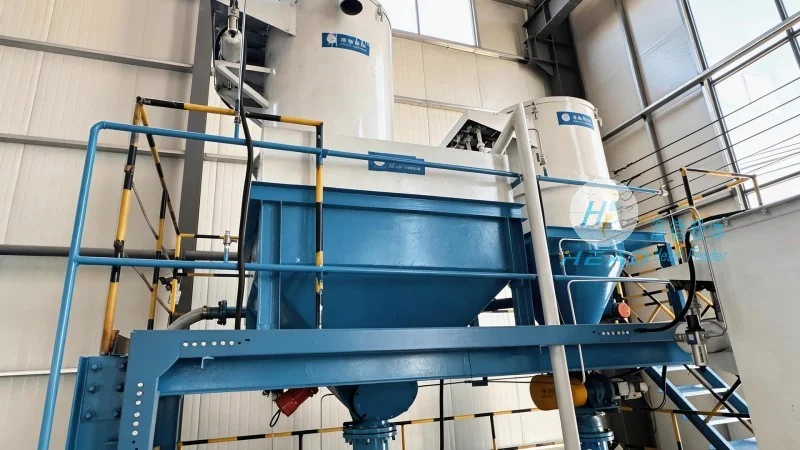
Application Scenarios
The tonne bag dust-free feeding station is widely used in scenarios where bulk materials are received in tonne bags and need to be transferred to processing equipment without compromising safety or quality. For instance, in chemical manufacturing facilities, the system is employed to handle raw materials like powders and granules, ensuring that the production process remains dust-free and compliant with environmental regulations. In pharmaceutical plants, the equipment is crucial for handling active pharmaceutical ingredients (APIs) and excipients, as the dust-free environment prevents cross-contamination and maintains product purity. Similarly, in food processing industries, the system is used to handle ingredients such as flour, sugar, and spices, where hygiene and dust control are critical to product quality and consumer safety. The versatility of the system allows it to adapt to different material types and processing requirements, making it a reliable solution for various working environments.
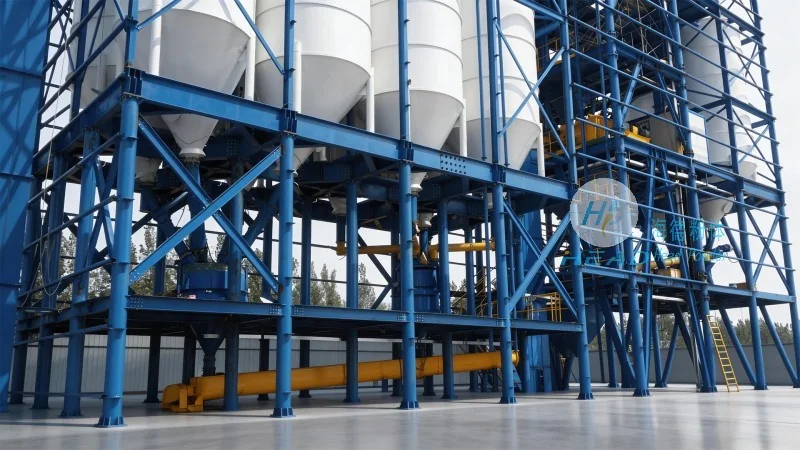
Advantages in Practical Use
Implementing the tonne bag dust-free feeding station offers several practical advantages for industrial operations. One of the most significant benefits is the reduction in labor costs associated with manual handling of bulk materials. The automated system minimizes the need for workers to directly interact with dusty materials, thereby improving workplace safety and reducing the risk of occupational diseases. Additionally, the system enhances product quality by preventing dust contamination, which can affect the consistency and performance of the final product. This is particularly important in industries where material purity is a key factor, such as pharmaceuticals and food processing. Furthermore, the equipment contributes to environmental sustainability by minimizing dust emissions, which helps in complying with local environmental regulations and reducing the company's carbon footprint. The long-term operational efficiency of the system also leads to cost savings through reduced maintenance and increased productivity.
Conclusion
HeadPowder's tonne bag dust-free feeding station with material conveying system is a sophisticated solution designed to address the complex needs of modern industrial material handling. By integrating advanced dust control technology with efficient conveying mechanisms, the equipment ensures safe, hygienic, and productive operations across various industries. The company's commitment to quality and innovation, as reflected in its products, positions it as a trusted partner for businesses seeking reliable material handling solutions. With its headquarters in Shandong, China, HeadPowder continues to deliver cutting-edge equipment that meets the evolving demands of industrial applications, providing customers with a competitive edge in their respective markets.




