Ammonium sulfate is a widely used chemical fertilizer, and its efficient transport is crucial for industrial applications. This article explores the principles and working scene characteristics of air-driven powder transport for ammonium sulfate, highlighting the technical aspects and practical applications.
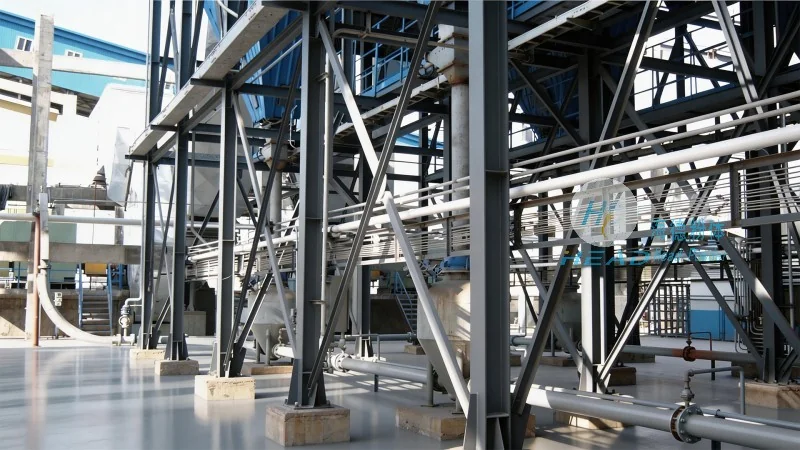
Company Introduction
Shandong HeadPowder Engineering Co., Ltd. is a professional enterprise specializing in powder handling solutions. With years of experience in the field, the company provides advanced air-driven transport systems tailored for various industrial needs. HeadPowder focuses on delivering reliable and efficient solutions for the transportation of bulk powders, including ammonium sulfate, ensuring optimal performance and safety in diverse operational environments.
Principles of Air-Driven Powder Transport
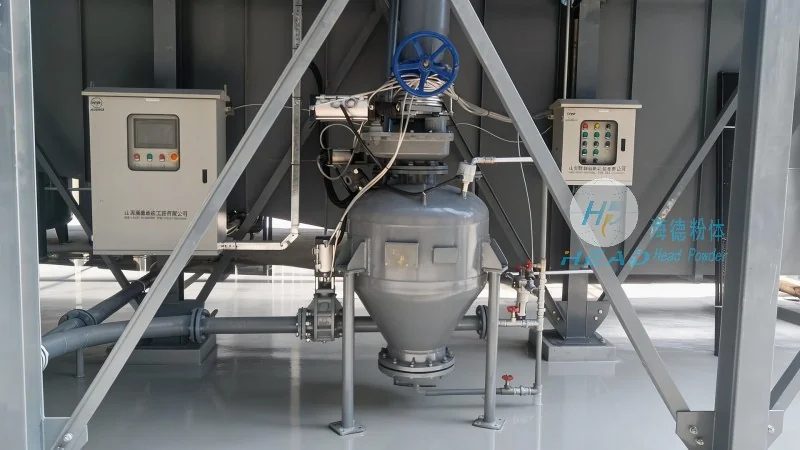
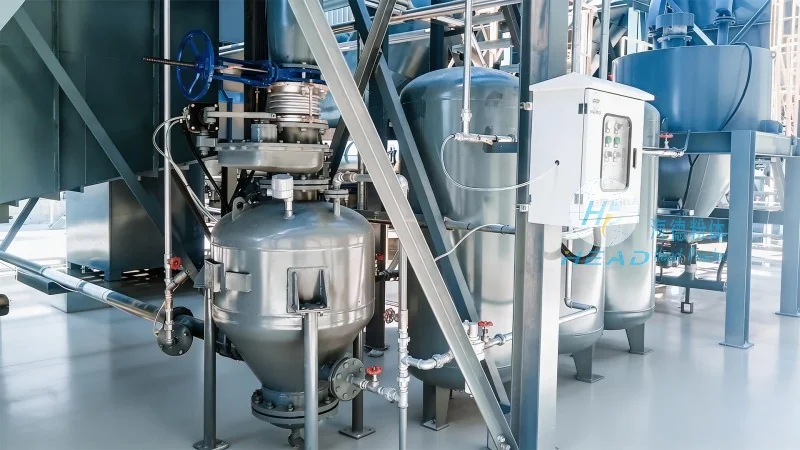
The air-driven powder transport system for ammonium sulfate operates based on the principle of pneumatic conveying. This method involves using compressed air to create a flow that moves the powder particles through a pipeline. The system typically consists of a blower, a hopper for material storage, and a pipeline network. As air is introduced into the hopper, it lifts the ammonium sulfate particles and propels them through the pipeline to the destination. The key to efficient transport lies in controlling the air pressure, flow rate, and particle size to ensure smooth and continuous movement without clogging or degradation of the material.
Working Scene Characteristics
The working scene characteristics of air-driven powder transport for ammonium sulfate vary based on the specific industrial application. In agricultural fertilizer production, the system is often used in large-scale factories to move raw materials from storage to processing units. The transport process requires high capacity and reliability to meet production demands. In chemical processing plants, the system may be integrated into a broader material handling network, ensuring seamless transfer between different stages of production. Additionally, the system is suitable for applications where dust control and environmental safety are critical, as the enclosed pipeline design minimizes particle dispersion and reduces health risks for operators.
Technical Advantages and Practical Applications
HeadPowder's air-driven powder transport systems offer several technical advantages that make them ideal for ammonium sulfate handling. The pneumatic conveying method provides a dust-free environment, which is essential for maintaining product quality and ensuring workplace safety. The system's flexibility allows for easy integration into existing production lines, reducing the need for major infrastructure changes. Furthermore, the high transport efficiency and low maintenance requirements contribute to cost savings and operational efficiency. Practical applications include fertilizer manufacturing, chemical processing, and material handling in industrial facilities where bulk powder transport is required.
Conclusion
Understanding the principles and working scene characteristics of air-driven powder transport for ammonium sulfate is vital for optimizing industrial processes. By leveraging advanced pneumatic conveying technology, companies like Shandong HeadPowder Engineering Co., Ltd. can enhance the efficiency and safety of powder handling operations. The integration of reliable transport systems ensures consistent material flow, reduces downtime, and supports sustainable industrial practices. As the demand for efficient bulk material transport continues to grow, air-driven systems remain a preferred solution for handling ammonium sulfate and other fine powders in various industrial settings.




