Intelligent powder pneumatic conveying equipment has become a critical component in modern industrial material handling systems, especially for applications involving the precise and efficient transport of bulk powders. This equipment, designed by Shandong HeadPowder Engineering Co., Ltd. (hereinafter referred to as HeadPowder), leverages advanced pneumatic technology to ensure reliable and safe material transfer. The following sections will explore the fundamental principles behind this technology and the diverse operational scenarios where it is applied.
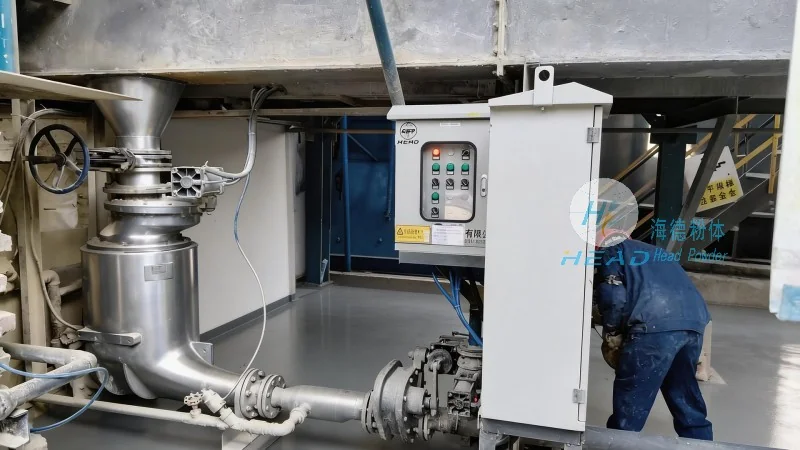
1. Core Principles of Pneumatic Conveying Technology
The operation of intelligent powder pneumatic conveying equipment is based on the fundamental principle of using compressed air or gas to move powder materials through a pipeline system. Unlike traditional mechanical conveying methods, which rely on physical force like gravity or mechanical components, pneumatic conveying utilizes the kinetic energy of the air stream to transport powders. This method is particularly effective for materials that are difficult to handle, such as fine powders, granules, or those that are prone to caking or segregation. The equipment typically consists of a blower, a hopper for material storage, a conveying line, and a receiver for the discharged material. The compressed air is introduced into the system, creating a flow that draws the powder from the hopper and transports it to the destination. The intelligent features of this equipment often include real-time monitoring of pressure, flow rate, and material level, ensuring optimal performance and preventing system failures.
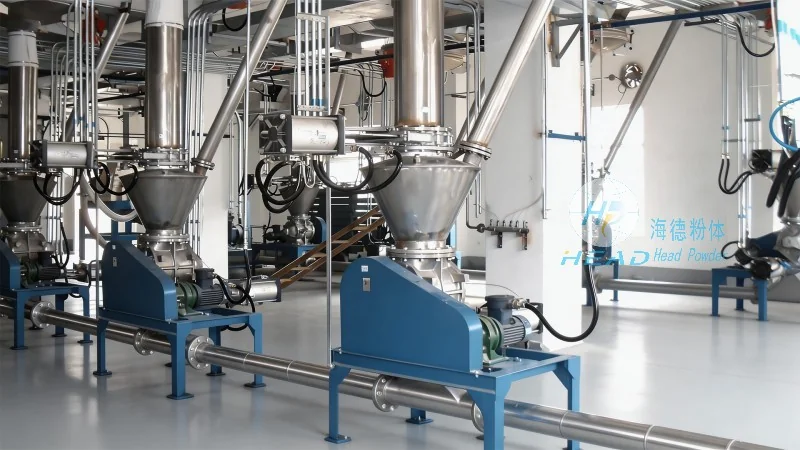
2. Key Working Scenarios and Applications
Intelligent powder pneumatic conveying equipment is widely used across various industries due to its adaptability and efficiency. In the pharmaceutical industry, for example, it is employed to transport active pharmaceutical ingredients (APIs) and excipients with high precision, maintaining strict contamination control and ensuring product quality. The food and beverage sector utilizes this technology for handling powders like flour, sugar, and protein powders, where hygiene and particle size control are paramount. In the chemical industry, it facilitates the transport of reactive powders and hazardous materials, with the intelligent system providing safety features like overpressure protection and material leak detection. Additionally, in the mining and mineral processing industries, it is used to convey raw materials and finished products, improving overall plant efficiency and reducing labor costs. The versatility of the equipment allows it to be integrated into existing production lines, enhancing workflow and reducing downtime.
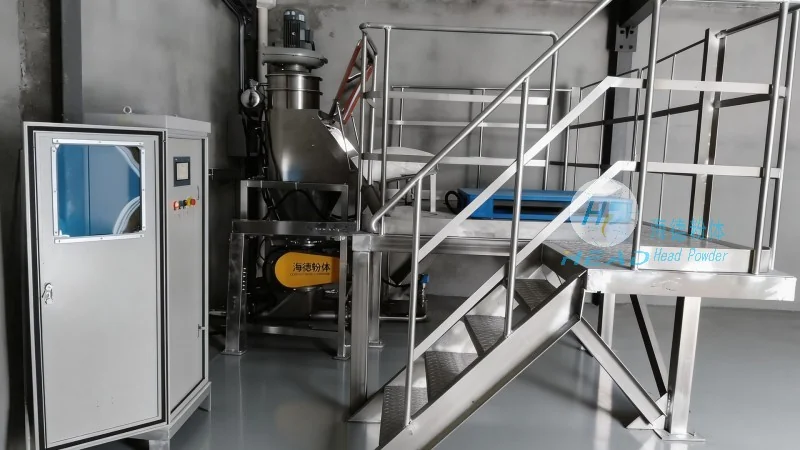
3. Advantages of Intelligent Control Systems
Modern intelligent powder pneumatic conveying equipment is equipped with advanced control systems that enhance operational efficiency and safety. These systems often include sensors for real-time monitoring of pressure, temperature, and material flow, as well as programmable logic controllers (PLCs) that adjust the air flow and conveying speed based on the material characteristics and system conditions. The intelligent features also enable remote monitoring and diagnostics, allowing operators to identify and resolve issues before they escalate into major problems. This not only improves system reliability but also reduces maintenance costs and extends the equipment's service life. Furthermore, the control systems can be programmed to follow specific conveying protocols, ensuring consistent performance and minimizing material loss or degradation during transport.
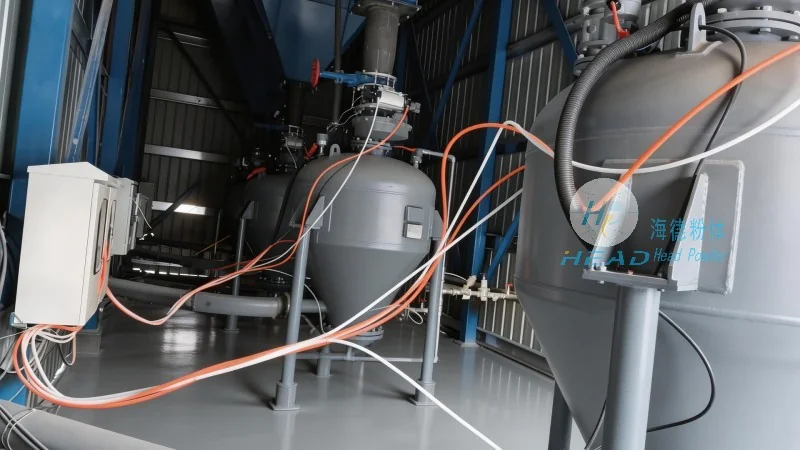
4. Company Background and Technical Expertise
Shandong HeadPowder Engineering Co., Ltd., a leading manufacturer in the field of powder handling equipment, has extensive experience in designing and manufacturing intelligent pneumatic conveying systems. The company, commonly known as HeadPowder, is headquartered in Shandong, China, and has a strong commitment to innovation and quality. With a team of skilled engineers and technicians, HeadPowder develops customized solutions tailored to the specific needs of each client. The company's products are designed to meet international standards and are widely recognized for their reliability, efficiency, and durability. By leveraging advanced technology and rigorous quality control processes, HeadPowder ensures that its equipment delivers optimal performance in various industrial applications.




