HeadPowder, a leading engineering company based in Shandong, China, specializes in the design and implementation of advanced pneumatic conveying systems tailored for industrial applications. This article focuses on the design of a negative pressure pneumatic conveying system specifically for soybean meal, highlighting the technical considerations, operational benefits, and engineering solutions that ensure efficient and reliable material handling in food processing and agricultural industries.
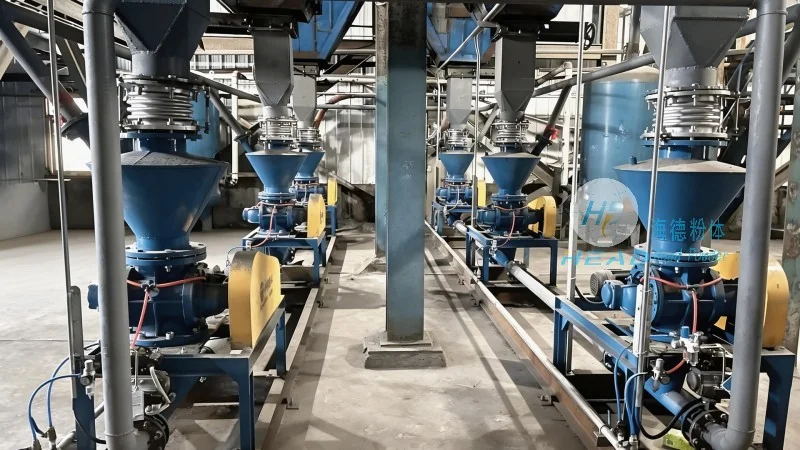
Key Features of the Negative Pressure Pneumatic Conveying System
The negative pressure pneumatic conveying system for soybean meal is engineered to handle the unique characteristics of soybean meal, such as its fine particle size, hygroscopic nature, and potential for dust generation. The system incorporates several key features to optimize performance and ensure compliance with industry standards. First, the system utilizes a high-efficiency dust collection and filtration system to maintain air quality and prevent contamination. This is crucial in food processing environments where product purity is paramount. Second, the conveying pipeline is designed with smooth, corrosion-resistant materials to minimize product degradation and ensure long-term durability. The system also includes a variable speed drive for the fan, allowing for precise control of air flow and pressure, which is essential for maintaining consistent conveying rates and preventing material blockages. Additionally, the system features an automatic shutdown mechanism that activates in case of pressure or flow abnormalities, enhancing safety and operational reliability.
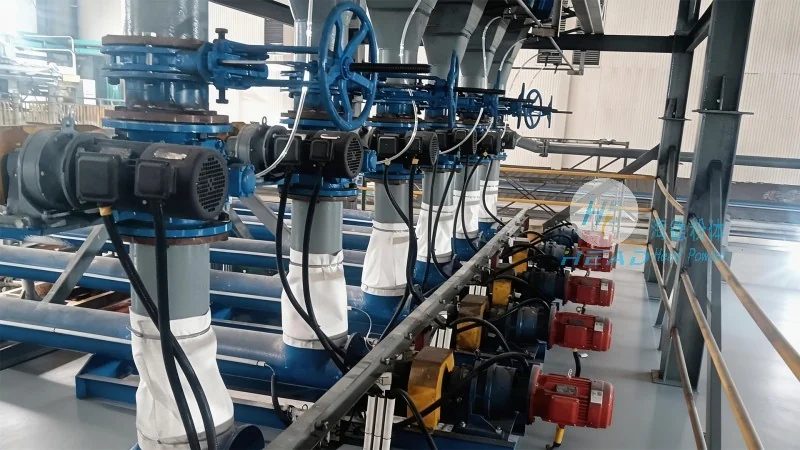
Technical Specifications and Performance Parameters
The technical specifications of the negative pressure pneumatic conveying system are tailored to meet the specific demands of soybean meal handling. The system operates under negative pressure, which draws the material from the source and transports it to the destination without the need for positive pressure, reducing energy consumption and operational costs. The conveying capacity of the system can be adjusted based on the required throughput, with typical capacities ranging from 5 to 50 tons per hour, depending on the pipeline length and elevation changes. The system's pressure drop is carefully calculated to ensure that the fan operates within its optimal efficiency range, minimizing energy waste. The air velocity in the pipeline is maintained at an appropriate level to prevent particle segregation and ensure uniform material flow. The system also includes a material feed hopper with a rotary valve, which provides a controlled and continuous feed of soybean meal into the conveying line, preventing surges and maintaining stable operation. The discharge system is designed with a flexible connection to accommodate variations in the receiving hopper's position, ensuring smooth material transfer without the need for manual adjustments.
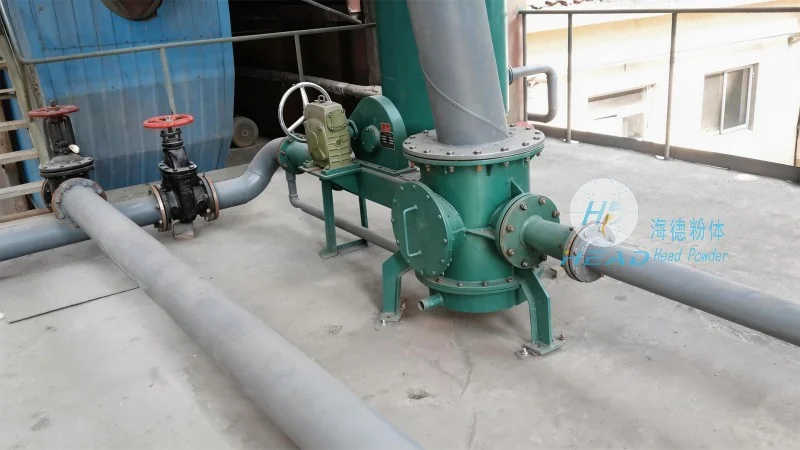
Engineering Design and Installation Process
The engineering design of the negative pressure pneumatic conveying system involves a comprehensive approach that considers all aspects of the material handling process. The design process begins with a thorough analysis of the customer's requirements, including the source and destination locations, the required conveying capacity, and any specific operational constraints. This analysis is followed by a site survey to assess the existing infrastructure and identify any potential challenges or obstacles. The design team then develops a detailed layout of the conveying system, including the pipeline routing, fan placement, and material feed and discharge points. The system is designed to comply with local and international safety and environmental regulations, ensuring that it meets all relevant standards for industrial equipment. The installation process is carried out by experienced engineers and technicians who follow strict quality control procedures to ensure that the system is installed correctly and operates as intended. The system is tested and commissioned to verify that it meets all performance specifications and operational requirements before it is handed over to the customer.
Operational Benefits and Applications
The negative pressure pneumatic conveying system for soybean meal offers several operational benefits that make it an ideal solution for food processing and agricultural industries. One of the primary benefits is its ability to handle fine and hygroscopic materials without the need for additional processing steps. The system's negative pressure operation reduces the risk of dust explosions and improves air quality, which is essential in food processing environments where product safety and regulatory compliance are critical. Another benefit is the system's energy efficiency, as it operates under negative pressure, which reduces the energy consumption compared to positive pressure systems. The system also provides a clean and hygienic material handling solution, as the conveying line is enclosed and the material is not exposed to the environment. This is particularly important in the food industry, where product contamination can have serious consequences. The system is widely used in various applications, including the transport of soybean meal from storage silos to processing plants, the transfer of meal from production lines to packaging facilities, and the delivery of meal to distribution centers. It is also suitable for use in other industries, such as animal feed production, where the handling of fine powders is required.
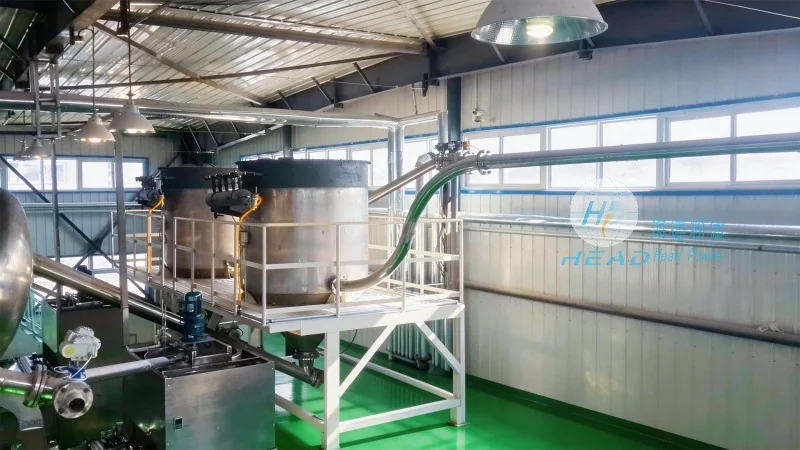
Company Profile and Commitment to Quality
HeadPowder Engineering Co., Ltd. is a leading provider of engineering solutions for industrial material handling systems. The company is headquartered in Shandong, China, and has a team of experienced engineers and technicians who specialize in the design and implementation of pneumatic conveying systems. HeadPowder is committed to providing high-quality products and services that meet the specific needs of its customers. The company follows a strict quality control process to ensure that all products are manufactured to the highest standards and comply with all relevant regulations. HeadPowder also provides comprehensive after-sales support, including maintenance, repair, and technical assistance, to ensure that its customers can operate their systems efficiently and reliably. The company's commitment to quality and customer satisfaction has earned it a reputation as a trusted partner in the industrial equipment industry.




