Coal fly ash, a byproduct of coal combustion, is a material that requires efficient and safe handling for industrial applications. The coal fly ash pneumatic conveying system is a specialized equipment designed to transport this fine particulate material over long distances with minimal loss and contamination. This system combines the principles of fluidization and air pressure to move ash from its source to a designated storage or processing location.
Understanding the Core Components of the System
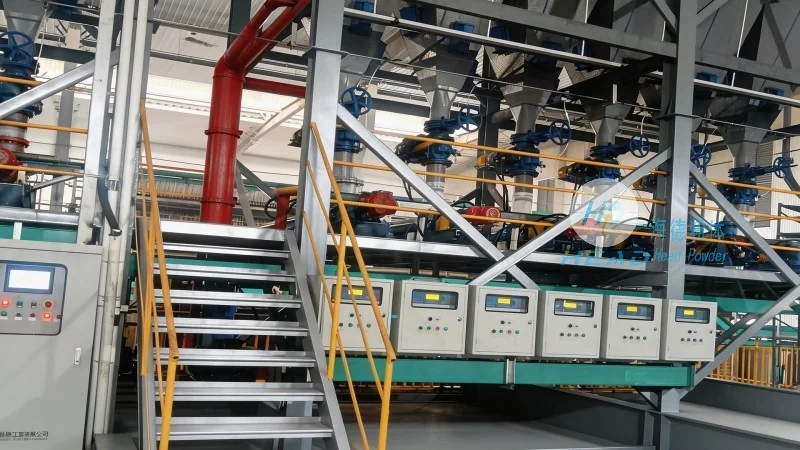
The system typically consists of several key components that work in tandem to ensure smooth operation. These include a hopper or feeder to store and meter the ash, a blower or compressor to generate the necessary air pressure, a pipeline network to convey the ash, and a receiver or silo to collect the material at the destination. Each component is engineered to handle the specific properties of coal fly ash, such as its fine particle size and potential for dust generation.
Design Principles for Efficient Coal Fly Ash Handling
Designing a coal fly ash pneumatic conveying system involves several critical principles aimed at maximizing efficiency and minimizing operational issues. The first principle is the selection of the appropriate conveying velocity, which must be high enough to keep the ash particles suspended in the air stream but not so high as to cause excessive pressure drop or wear on the system components. The second principle is the use of a consistent air flow rate, which ensures that the ash particles are transported without settling or clogging the pipeline. Additionally, the system design must account for the ash's moisture content and potential for agglomeration, as these factors can affect the system's performance and require additional equipment like dryers or agglomerators.
How the System Operates: A Step-by-Step Overview
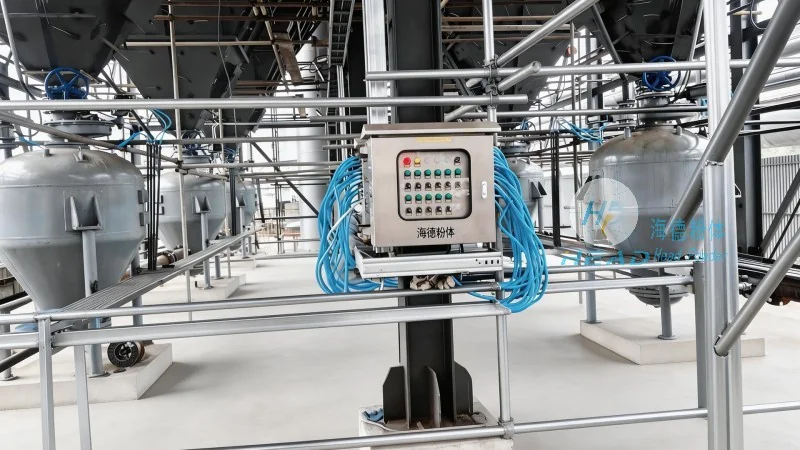
The operation of a coal fly ash pneumatic conveying system begins with the ash being fed from a storage hopper into the conveying line. The blower then introduces compressed air into the line, creating a high-velocity air stream that lifts and transports the ash particles. As the ash travels through the pipeline, it is kept in suspension by the air flow. At the receiving end, the air and ash mixture is separated, usually through a cyclone separator or a filter, and the ash is collected in a silo or storage tank. The air is then filtered and discharged back into the environment, ensuring compliance with air quality regulations.
Key Advantages of Using a Pneumatic Conveying System for Coal Fly Ash
There are several advantages to using a pneumatic conveying system for coal fly ash handling. First, it offers a dust-free and enclosed transport process, which reduces the risk of environmental contamination and improves workplace safety. Second, the system can transport ash over long distances with minimal material loss, making it suitable for large-scale industrial operations. Third, the equipment is relatively compact and can be integrated into existing industrial facilities, reducing the need for extensive construction or modification. Finally, the system is highly flexible, allowing for changes in the conveying route or capacity without major overhauls.
Applications and Industries That Benefit from This Technology
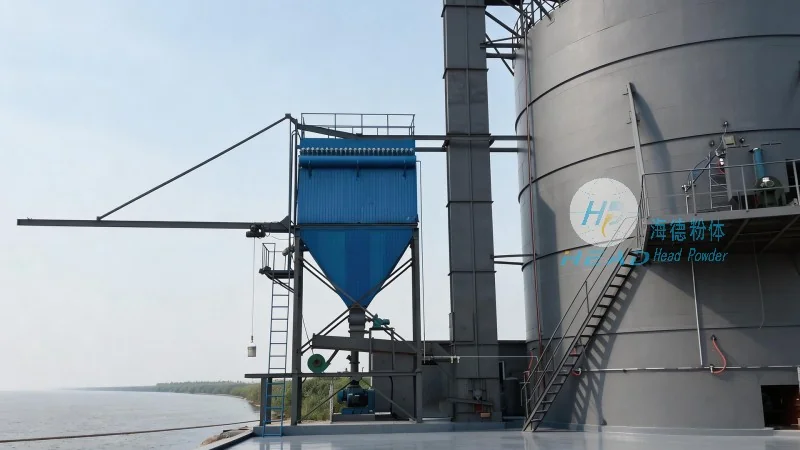
The coal fly ash pneumatic conveying system is widely used in various industries that rely on coal as a fuel source. These include power plants, cement manufacturing facilities, and industrial boilers. In power plants, the system is used to transport ash from the boiler to a storage facility or to a recycling plant where it can be used as a raw material for concrete or other building materials. In cement plants, the ash is often used as a supplementary cementitious material, and the conveying system ensures that it is delivered to the mixing plant efficiently and without contamination. Other industries that benefit from this technology include chemical processing plants and industrial waste management facilities, where ash is a byproduct that needs to be handled safely and effectively.
The Role of Shandong HeadPowder Engineering Co., Ltd. in Providing These Systems
Shandong HeadPowder Engineering Co., Ltd., a leading manufacturer of coal fly ash handling equipment, specializes in designing and supplying pneumatic conveying systems tailored to the specific needs of their clients. With years of experience in the industry, the company has developed a deep understanding of the challenges associated with coal fly ash transport and has engineered systems that address these challenges effectively. The company's systems are designed to meet the highest standards of efficiency, reliability, and safety, ensuring that clients can operate their facilities with minimal downtime and maximum productivity. By partnering with Shandong HeadPowder Engineering Co., Ltd., industrial facilities can benefit from state-of-the-art technology and expert guidance to optimize their coal fly ash handling processes.




