A grain pneumatic conveying system is a specialized piece of equipment used in the agricultural and food processing industries to transport bulk materials like grains, powders, and other dry commodities. Unlike traditional mechanical conveyors that rely on belts or chains, pneumatic systems utilize air pressure to move materials through a network of pipes. This method offers several advantages, including the ability to transport materials over long distances, vertical lifting capabilities, and the option to handle materials in a closed system, which helps maintain hygiene and prevent contamination. The core of such a system is the combination of air movement and material handling, making it an essential tool for efficient grain processing and storage operations.
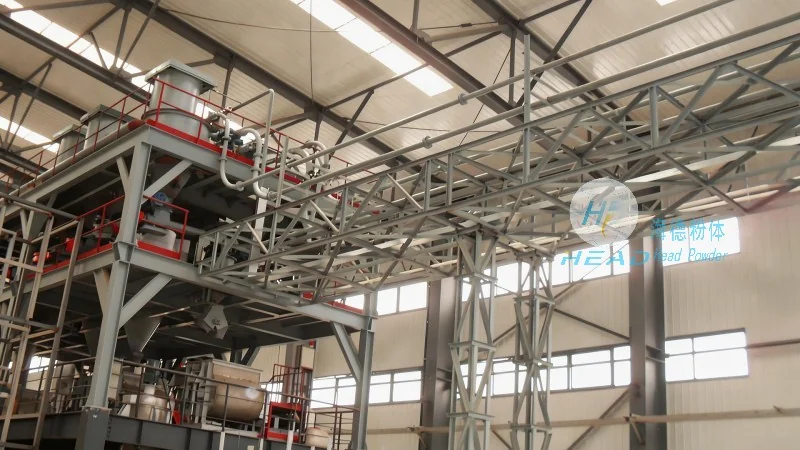
Key Components of a Grain Pneumatic Conveying System
The effectiveness of a grain pneumatic conveying system depends on its key components, each playing a critical role in the overall operation. The primary components include the hopper or feed hopper, which holds the material to be conveyed; the air mover, such as a rotary lobe blower or a positive displacement blower, which generates the necessary air pressure; the conveying line, typically made of metal or plastic pipes, which transports the material and air mixture; and the discharge device, which releases the material at the destination. Additionally, a filter system is often included to clean the air after it has passed through the conveying line, ensuring that the air is returned to the environment without dust or particles. Each component must be carefully selected and sized to match the specific requirements of the material being handled and the distance it needs to travel.
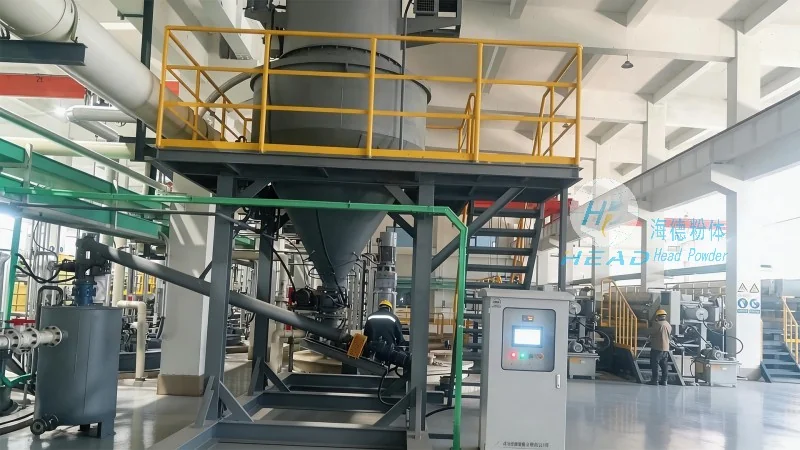
Design Principles and Operational Mechanics
The design of a grain pneumatic conveying system is based on several fundamental principles of fluid dynamics and material handling. The most common design is the "pressure system," where the air mover operates under positive pressure, pushing the material through the system. In this setup, the air and material are mixed at the inlet of the conveying line, and the mixture travels to the discharge point. The other design is the "vacuum system," where the air mover creates a negative pressure, drawing the material into the system. Pressure systems are generally more suitable for long-distance and vertical conveying, while vacuum systems are better for short-distance and horizontal transport. The design also considers factors such as the material's density, flowability, and moisture content, as these properties affect the air velocity required to move the material efficiently. Engineers must calculate the necessary air volume and pressure to ensure that the material is conveyed without clogging or excessive wear on the system components.
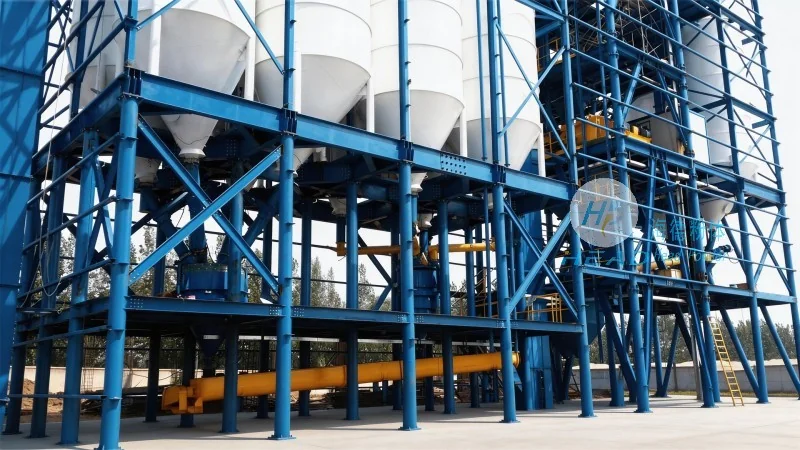
Benefits of Using Grain Pneumatic Conveying Systems
Implementing a grain pneumatic conveying system offers numerous benefits for businesses in the agricultural and food processing sectors. One of the most significant advantages is improved efficiency and productivity. By automating the material handling process, companies can reduce labor costs and increase throughput, as the system can operate continuously without the need for manual intervention. Another key benefit is enhanced hygiene and safety. Since the system operates in a closed environment, it minimizes the risk of dust exposure, which is a major health hazard in grain handling facilities. This also helps maintain the quality of the product, as the material is protected from contamination by dust, moisture, or other environmental factors. Furthermore, pneumatic conveying systems are versatile and can be adapted to various applications, from small-scale farms to large industrial processing plants. They can handle a wide range of materials, including different types of grains, seeds, and powders, making them a flexible solution for diverse operational needs. The system's ability to transport materials vertically and horizontally also optimizes space utilization in facilities, allowing for more efficient layout designs.
Application Scenarios and Industry Standards
Grain pneumatic conveying systems are widely used in various applications across the agricultural and food processing industries. In grain storage facilities, these systems are used to transfer grain from silos to processing equipment or to move grain between different storage areas. In flour mills, they are essential for conveying raw materials like wheat and other grains to the milling machines. The systems are also used in seed processing plants to transport seeds for cleaning, sorting, and packaging. Additionally, they are employed in the production of animal feed, where various ingredients are mixed and conveyed to the final packaging stage. When designing and implementing a pneumatic conveying system, it is crucial to adhere to industry standards and regulations to ensure safety and efficiency. These standards cover aspects such as material compatibility with the conveying line, air quality requirements, and safety features like explosion-proof designs for handling flammable materials. Companies must also consider local regulations regarding dust control and environmental impact, as these can affect the design and operation of the system. By following these standards, businesses can ensure that their grain pneumatic conveying systems are reliable, safe, and compliant with industry requirements.
About Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a leading manufacturer and supplier of grain pneumatic conveying systems and related equipment. With its headquarters located in Shandong, China, the company has established itself as a trusted partner for businesses seeking efficient and reliable material handling solutions. HeadPowder specializes in designing and manufacturing customized pneumatic conveying systems tailored to the specific needs of its clients. The company's products are known for their high quality, durability, and energy efficiency, making them suitable for a wide range of applications in the agricultural and food processing industries. HeadPowder's team of experienced engineers and technicians work closely with clients to understand their operational requirements and provide tailored solutions that enhance productivity and reduce costs. The company's commitment to innovation and customer satisfaction has earned it a reputation as a leading provider in the industry, with a focus on delivering products that meet the highest standards of performance and safety. Whether for small-scale farms or large industrial operations, HeadPowder offers a range of pneumatic conveying systems that help businesses optimize their material handling processes and improve overall operational efficiency.




