Bin pump powder pneumatic conveying systems represent a sophisticated method for transporting bulk powders and granular materials over long distances with high efficiency. This technology is widely utilized in various industrial sectors, including chemical, food, pharmaceutical, and cement industries, due to its ability to handle a wide range of powder characteristics and provide reliable, low-maintenance operation. The system typically consists of a hopper, a bin pump, a conveying line, and a receiver, all working in tandem to ensure seamless material transfer.
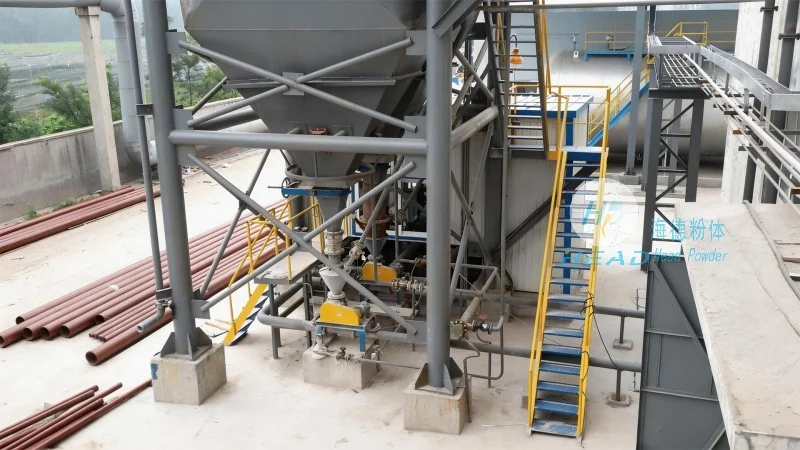
Working Principle of Bin Pump Powder Pneumatic Conveying
The core of the bin pump system lies in its ability to create a pressure differential that drives the material through the conveying line. The process begins with the material being fed into the hopper. When the bin pump is activated, it generates a vacuum or pressure within the hopper, causing the powder to be drawn into the pump chamber. The pump then compresses the material, forcing it through the pipeline to the destination receiver. This cycle repeats continuously, maintaining a steady flow of material. The bin pump's design allows for precise control over the conveying rate, ensuring that the system operates optimally under varying load conditions.
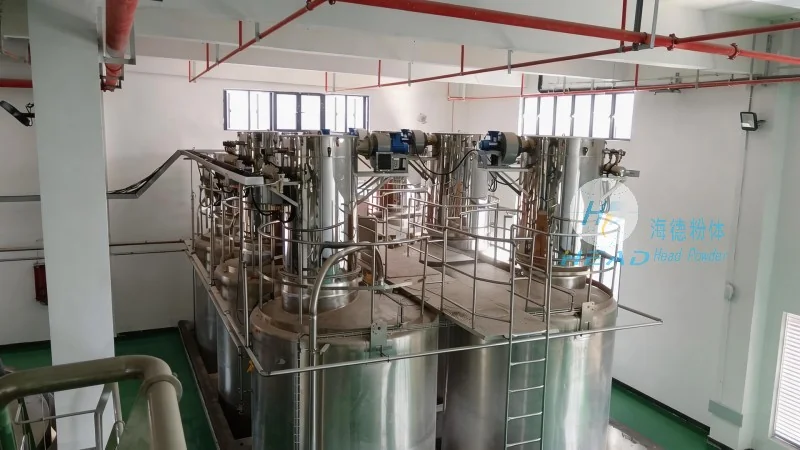
Key Characteristics of Bin Pump Powder Pneumatic Conveying
Several distinct characteristics make bin pump systems an attractive choice for industrial applications. Firstly, they offer high conveying capacities, capable of transporting large volumes of powder per hour, which is essential for high-throughput operations. Secondly, the system is highly flexible, as it can handle different powder types—ranging from fine powders to coarse granules—without requiring significant modifications. Thirdly, bin pumps are known for their low maintenance requirements; the absence of moving parts in the conveying line reduces wear and tear, leading to longer service life and lower operational costs. Additionally, the system provides excellent dust control, as the material is contained within a sealed environment, minimizing environmental impact and ensuring workplace safety. Another notable feature is the ability to operate over long distances, with some systems capable of conveying materials up to several kilometers, making it suitable for large-scale industrial plants.
Company Profile: Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., operating under the brand name HeadPowder, is a leading manufacturer specializing in the design, development, and supply of advanced powder handling equipment. With a strong focus on innovation and quality, the company has established itself as a trusted partner in the industry, providing customized solutions tailored to the specific needs of clients. HeadPowder's expertise lies in the engineering of efficient and reliable bin pump systems, ensuring that customers receive products that meet international standards and deliver optimal performance. The company's commitment to customer satisfaction and technical excellence has earned it a reputation for delivering solutions that enhance operational efficiency and reduce costs for its clients.
Conclusion
Bin pump powder pneumatic conveying systems offer a robust and efficient solution for bulk material handling, combining advanced technology with practical design. Their ability to handle diverse powder types, operate over long distances, and maintain low maintenance costs makes them a preferred choice in various industrial applications. With the support of companies like Shandong HeadPowder Engineering Co., Ltd., these systems continue to evolve, providing industries with reliable and sustainable solutions for their material handling needs.




