Organic fertilizer powder pneumatic conveying systems have become increasingly vital in modern agricultural operations, offering efficient and environmentally friendly solutions for transporting bulk organic fertilizers. This technology facilitates the movement of organic fertilizer powders from storage silos or production facilities to application points, such as fields or processing plants, without the need for mechanical components like belts or buckets. The following sections will delve into the working principle and key characteristics of this system, providing a comprehensive understanding of its functionality and advantages.
Working Principle of Organic Fertilizer Powder Pneumatic Conveying
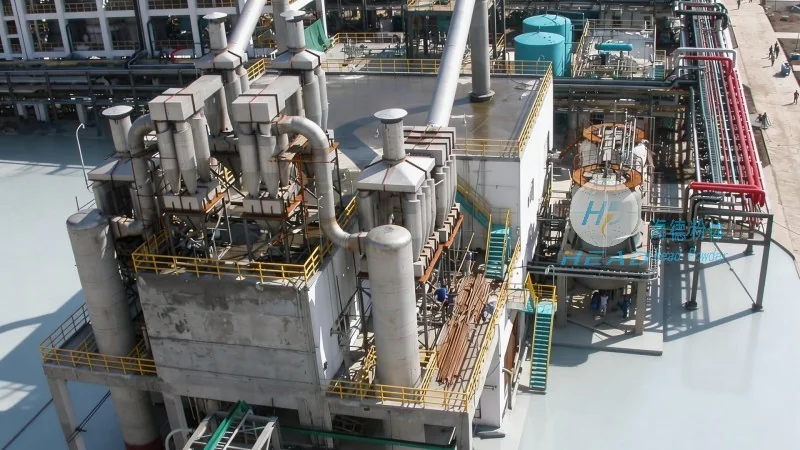
The core mechanism of organic fertilizer powder pneumatic conveying relies on the use of compressed air or vacuum to transport dry powder materials through a network of pipes. There are two primary modes of operation: pressure conveying and vacuum conveying. In pressure conveying, a positive pressure is generated at the inlet of the conveying line, typically using a blower or compressor, which forces the organic fertilizer powder into the pipeline. The air and powder mixture travels through the system, with the powder being separated from the air at the discharge point, often through a cyclone separator or filter. Vacuum conveying, on the other hand, uses a vacuum pump to create a negative pressure at the inlet, drawing the organic fertilizer powder into the pipeline. The powder is then transported to the collection point where it is discharged under pressure or by gravity.
During the conveying process, the organic fertilizer powder is suspended in the air stream, which allows for efficient and continuous movement. The velocity of the air is critical; it must be sufficient to keep the powder particles suspended but not so high as to cause excessive wear on the system components or excessive energy consumption. The system typically includes components such as a hopper for material storage, a feeder to control the flow rate, a conveying line, and a separator for powder recovery. The selection of the conveying mode (pressure or vacuum) depends on factors like the distance to be covered, the height of the transfer, and the characteristics of the organic fertilizer powder, including its particle size, moisture content, and flowability.
Key Characteristics of Organic Fertilizer Powder Pneumatic Conveying
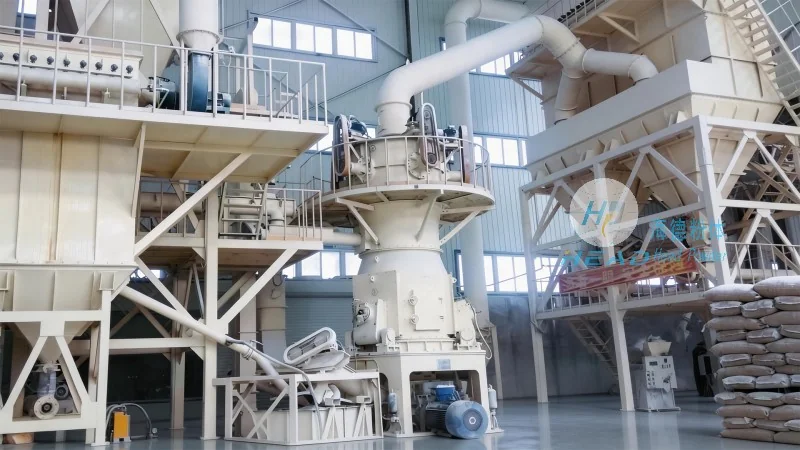
Organic fertilizer powder pneumatic conveying systems exhibit several distinct characteristics that make them advantageous in agricultural applications. Firstly, they offer high conveying efficiency, capable of transporting large volumes of organic fertilizer over significant distances with minimal energy consumption compared to traditional mechanical systems. The ability to handle bulk materials without the need for manual handling reduces labor costs and improves operational safety. Secondly, these systems are highly flexible, allowing for easy integration into existing agricultural infrastructure and adaptation to varying production and application needs. The modular design of the system enables adjustments to the conveying line length, height, or capacity as required.
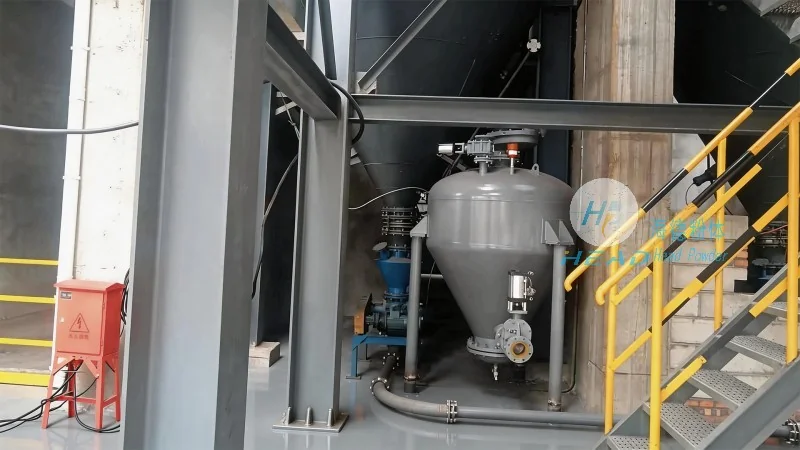
Another critical characteristic is the environmental friendliness of pneumatic conveying. Unlike mechanical systems that may generate dust or require lubricants, pneumatic systems operate with clean air, minimizing pollution and ensuring compliance with environmental regulations. The enclosed pipeline system also prevents the loss of organic fertilizer during transport, reducing waste and improving resource utilization. Furthermore, the system's ability to handle a wide range of organic fertilizer types, including those with varying particle sizes and moisture levels, enhances its versatility. This adaptability is particularly valuable in organic farming, where different types of organic fertilizers may be used depending on soil conditions and crop requirements.
Applications and Benefits in Agricultural Settings
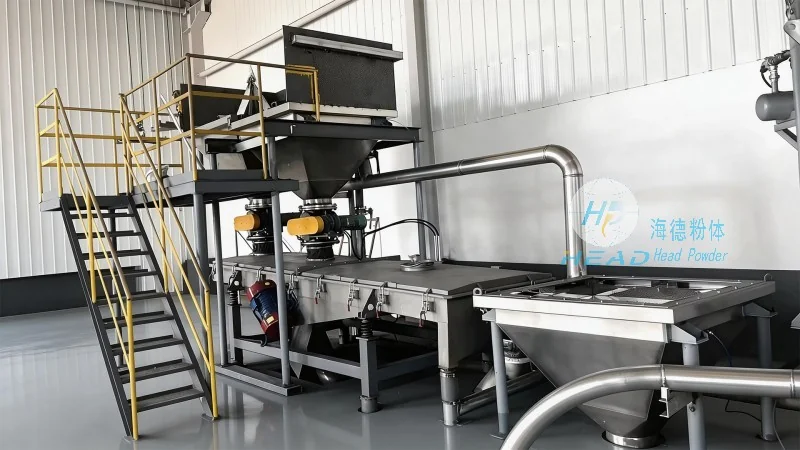
The application of organic fertilizer powder pneumatic conveying systems in agricultural settings is widespread, contributing to more efficient and sustainable farming practices. These systems are commonly used in large-scale organic fertilizer production facilities to transport raw materials from storage to processing units and finished products to storage or distribution points. In field application, they enable the precise and uniform distribution of organic fertilizers, ensuring optimal nutrient delivery to crops. The systems also play a role in processing plants, where organic fertilizers may be blended with other materials or processed into granules before final application. The benefits extend beyond efficiency and environmental protection; they also enhance the overall productivity of agricultural operations by reducing downtime associated with material handling and improving the consistency of fertilizer application.
Conclusion and Company Overview
Organic fertilizer powder pneumatic conveying represents a sophisticated and efficient technology for handling bulk organic fertilizers in agricultural and industrial settings. Its working principle, based on air pressure or vacuum to transport powders through enclosed pipelines, offers significant advantages in terms of efficiency, flexibility, and environmental sustainability. The characteristics of these systems, including high conveying capacity, low energy consumption, and adaptability to various organic fertilizer types, make them a preferred choice for modern agricultural operations. As the demand for sustainable and efficient agricultural practices grows, the importance of such systems will continue to increase. Shandong HeadPowder Engineering Co., Ltd., a leading provider in this field, specializes in the design, manufacturing, and implementation of organic fertilizer powder pneumatic conveying systems, leveraging advanced engineering and technology to meet the evolving needs of the agricultural industry. With a focus on quality and innovation, the company ensures that its systems deliver reliable performance and contribute to the advancement of sustainable farming practices.




