Bulk bag packing powder conveying is a pivotal technology in the handling of dry bulk materials, enabling the efficient transfer of powders from a source to a destination while maintaining material integrity and safety. This process is widely used across industries such as chemicals, food and beverage, pharmaceuticals, and construction, where large volumes of powders need to be moved reliably and cost-effectively. The method relies on bulk bags (super sacks) as the primary container, which are designed to hold substantial quantities of material and facilitate easy loading and unloading. Understanding the principles and working scene characteristics of this technology is crucial for optimizing industrial operations and selecting the appropriate equipment for specific applications.
The Core Principles of Bulk Bag Packing Powder Conveying
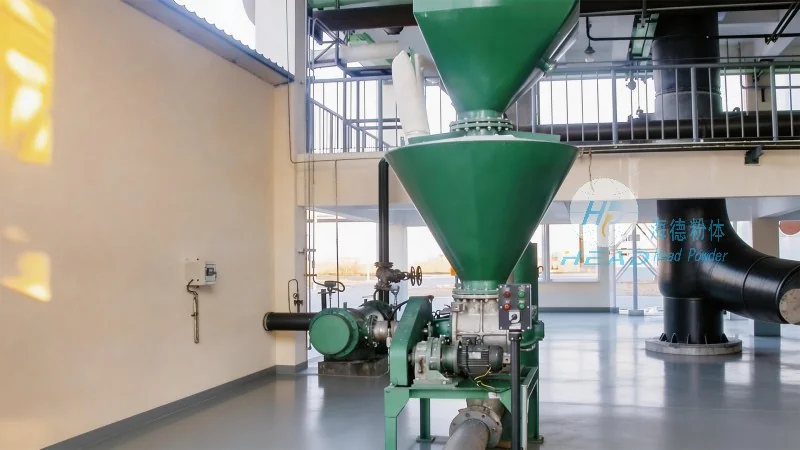
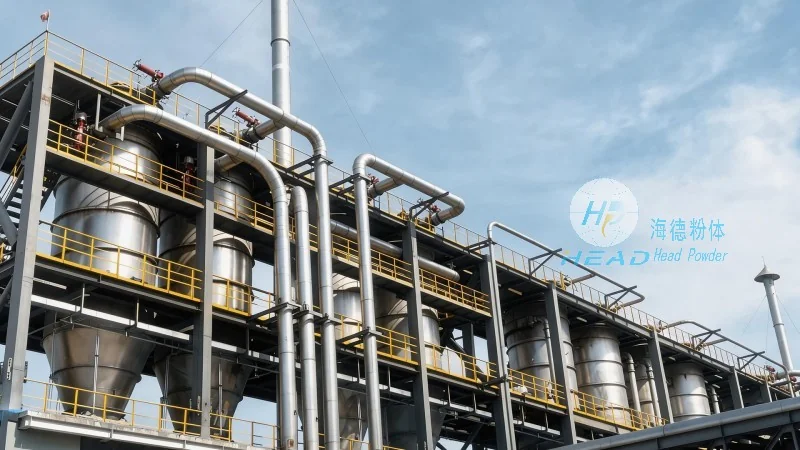
The fundamental principles of bulk bag packing powder conveying revolve around two primary conveying methods: negative pressure (vacuum) and positive pressure (pressure). Negative pressure systems utilize a vacuum to draw material from the source into the conveying line, while positive pressure systems employ compressed air or gas to push material forward. The choice between these methods depends on several factors, including the material's properties (e.g., particle size, moisture content, and flowability), the distance between the source and destination, and the required throughput. Negative pressure systems are often preferred for handling fine powders or materials that are prone to dust generation, as they minimize particle breakage and maintain a stable flow. Positive pressure systems, on the other hand, are suitable for handling coarse materials or when a longer conveying distance is required, as they can maintain higher pressure and flow rates. Additionally, advanced systems may incorporate a combination of both methods, known as mixed pressure conveying, to address complex material handling challenges. The system typically includes components such as a hopper, a rotary valve, a conveying line, and a bulk bag discharger, all working in tandem to ensure smooth and continuous material transfer. Dust control is a critical aspect of these systems, with features like pulse-jet filters and cyclone separators used to maintain air quality and prevent dust accumulation, ensuring compliance with environmental regulations and workplace safety standards.
Working Scene Characteristics of Bulk Bag Packing Powder Conveying
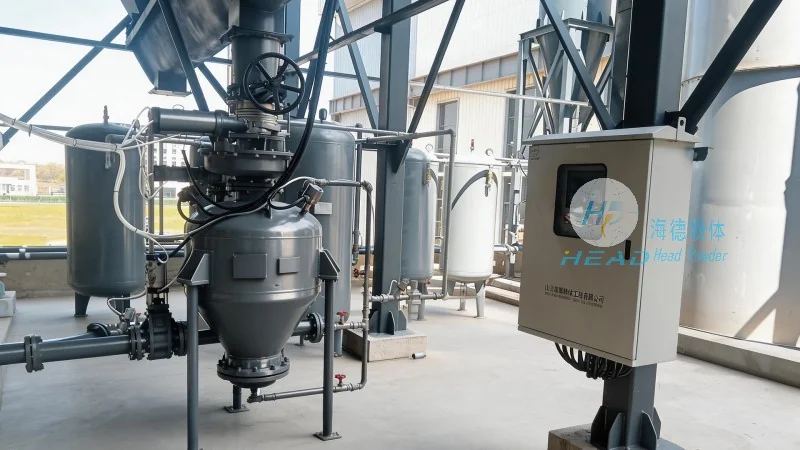
The working scene characteristics of bulk bag packing powder conveying vary significantly based on the industry and the specific application, each presenting unique challenges and requirements. In the chemical industry, for example, the process may involve handling hazardous or reactive powders, such as chemicals used in manufacturing or industrial processes. This requires specialized equipment with explosion-proof designs, material compatibility, and strict safety protocols to prevent accidents and ensure worker protection. The food and beverage industry demands stringent hygiene standards, with equipment made from food-grade materials (e.g., stainless steel) and easy-to-clean surfaces to prevent contamination and maintain product quality. The pharmaceutical industry requires sterile and contamination-free systems, with closed-loop conveying to prevent cross-contamination and ensure product purity. In the construction sector, bulk bag packing powder conveying is commonly used for transporting cement, fly ash, and other building materials, where high throughput and durability are essential to meet production demands. Each of these scenarios highlights the importance of tailored solutions, as the material's properties, operational constraints, and regulatory requirements must all be considered. The adaptability of bulk bag packing powder conveying systems makes them suitable for a wide range of applications, from small-scale laboratory operations to large-scale industrial plants, and the ability to customize systems to meet specific needs is a key advantage.
Company Overview: Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., operating under the brand name headpowder, is a leading manufacturer and supplier of advanced powder handling solutions. With a strong commitment to innovation and customer satisfaction, the company specializes in designing and manufacturing bulk bag packing powder conveying systems that meet the diverse needs of various industries. HeadPowder's team of experienced engineers and technicians leverages cutting-edge technology and practical engineering expertise to develop reliable, efficient, and cost-effective solutions. The company's headquarters is located in Shandong, China, where it maintains state-of-the-art research and development facilities, ensuring continuous improvement and adherence to international quality standards. By focusing on customer-centric design and tailored solutions, headpowder delivers systems that optimize material flow, reduce downtime, and enhance overall operational efficiency. The company's product line includes a range of bulk bag packing and conveying equipment, such as vacuum and pressure conveying systems, bulk bag fillers, and dischargers, all designed to handle different types of powders and applications. HeadPowder's dedication to quality and customer service has established it as a trusted partner in the powder handling industry, providing solutions that help businesses improve productivity and maintain compliance with industry regulations.




