Principle and Working Scene Characteristics of Gravity Dust Removal Powder Body Conveying System Equ
Release time:2026-09-19 08:01:30
name of the company:Shandong Headpowder Engineering Co., Ltd.
telephone:156-6277-7102
contacts:Zhang manager
Headpowder, the abbreviation for Shandong HeadPowder Engineering Co., Ltd., is a professional manufacturer based in Shandong, China. The company specializes in the research, development, and production of advanced powder conveying and dust removal equipment. With a focus on providing efficient and reliable solutions for industrial powder handling, Headpowder has established itself as a trusted partner in various industries requiring precise and safe material transport.
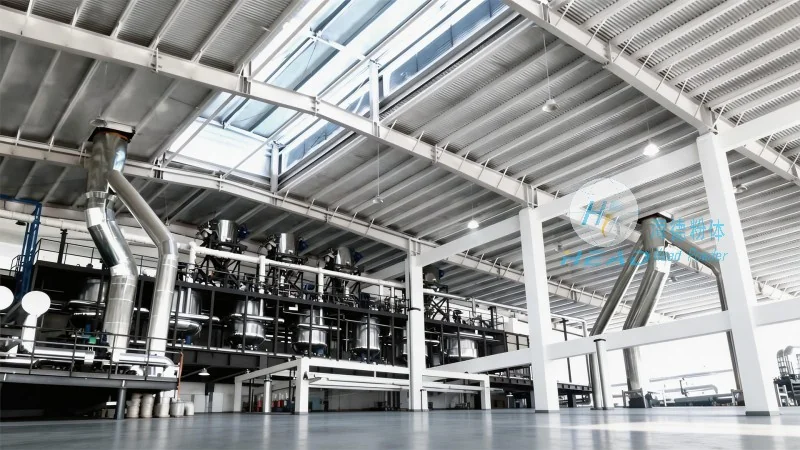
Principle of Gravity Dust Removal Powder Conveying System
The gravity dust removal powder body conveying system operates on the fundamental principle of combining gravity-driven flow with air-assisted separation to transport fine powders. The system integrates a dust collector with the conveying pipeline, creating a closed loop that ensures minimal dust leakage. Raw powder is first introduced into a hopper, where it is then released into the conveying line under the influence of gravity. As the powder moves through the pipeline, the air flow generated by the system helps to separate larger dust particles from the powder stream. These dust particles are captured by the dust removal unit, while the purified powder continues along the conveying path to the target location. This design effectively reduces airborne dust and maintains a clean operational environment.
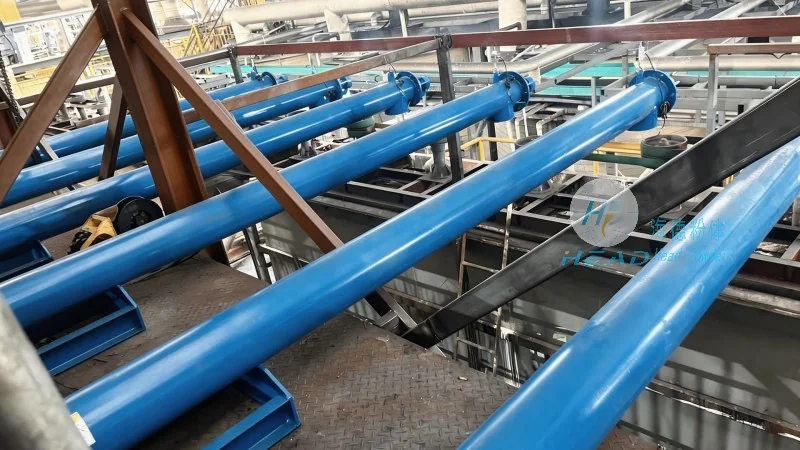
Working Scene Characteristics
The gravity dust removal powder conveying system is particularly well-suited for industrial applications where fine powders need to be transported over moderate distances with low energy consumption. Key working scene characteristics include:
- Industrial facilities such as cement plants, chemical processing units, and food processing operations, which handle large volumes of powders on a daily basis.
- Environments where dust control is a priority, as the integrated dust removal feature helps to maintain air quality and comply with environmental regulations.
- Scenarios with space constraints, as the system can be installed in compact areas without sacrificing performance.
- Applications requiring low maintenance and long service life, due to the minimal moving parts and robust design of the equipment.
Key Features and Benefits
Headpowder's gravity dust removal powder conveying system offers several advantages that make it an ideal choice for industrial powder handling. The system is designed to be energy-efficient, reducing operational costs compared to traditional pneumatic conveying methods. Additionally, the integrated dust removal feature ensures compliance with environmental standards while maintaining a safe working environment. The equipment is also constructed with high-quality materials, providing durability and long-term reliability. These features make the system suitable for continuous operation in demanding industrial settings.
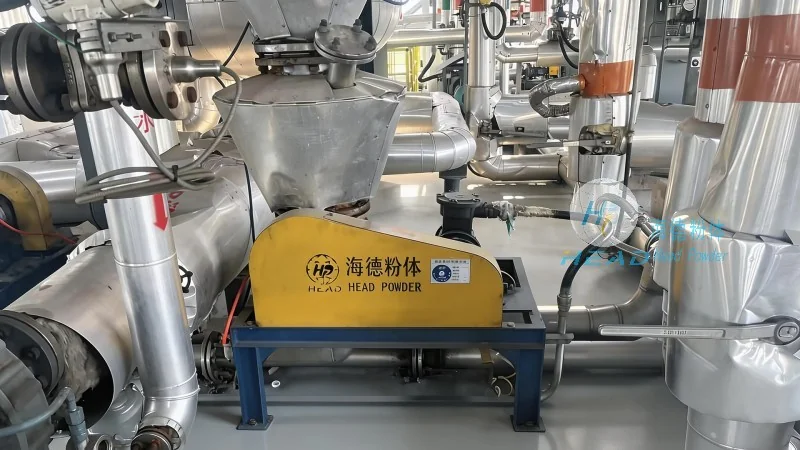
Application Examples
Real-world applications of the gravity dust removal powder conveying system include the transport of cement, flour, and other fine powders in manufacturing processes. For instance, in a cement plant, the system can be used to move raw materials from storage silos to production lines, while effectively capturing dust emissions. Similarly, in a food processing facility, the system ensures the safe and clean transport of flour and other ingredients, preventing contamination and maintaining product quality. These examples highlight the versatility and effectiveness of the system in various industrial contexts.




