HeadPowder, a leading engineering company based in Shandong, China, specializes in the design and manufacturing of advanced material handling solutions. The gray storage material conveying system equipment is a critical component in industrial applications where bulk materials need to be efficiently transported from storage silos to processing units. This equipment is engineered to handle various types of powders and granules, ensuring reliable and consistent material flow in industrial settings.
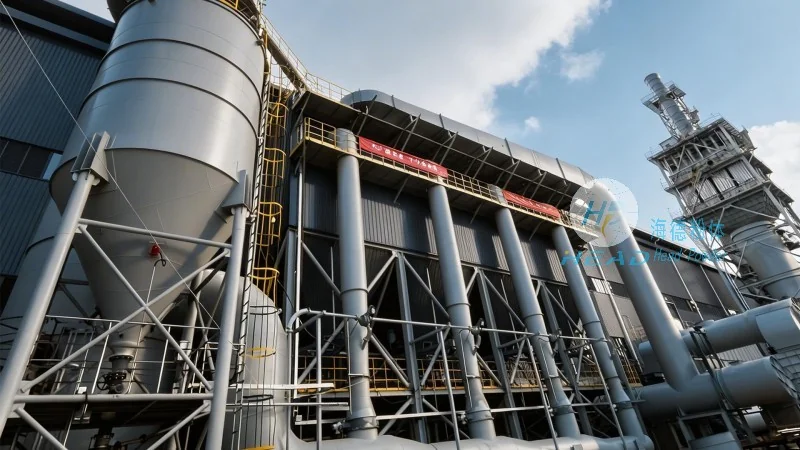
Principle of Operation for the Conveying System
The core principle of the gray storage material conveying system equipment revolves around the use of pneumatic or mechanical methods to transport materials. In pneumatic conveying systems, compressed air is used to create a flow that moves the material through a pipeline. This method is particularly effective for handling fine powders and dust, as it minimizes material degradation and ensures a clean transfer process. Mechanical conveying systems, on the other hand, utilize screw conveyors, belt conveyors, or bucket elevators to move materials. These systems are often preferred for handling bulkier materials or when the material is sensitive to air exposure. The choice between pneumatic and mechanical systems depends on the specific characteristics of the material being transported, such as particle size, moisture content, and flowability.
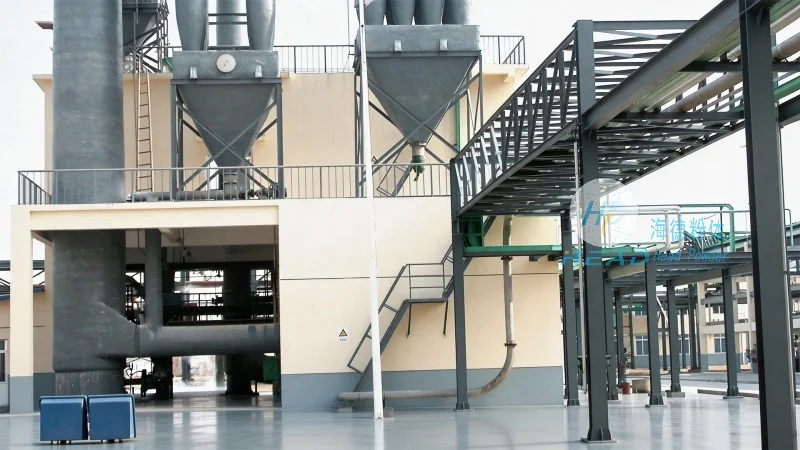
Key Working Scene Characteristics
The gray storage material conveying system equipment is designed to operate in diverse industrial environments, each with unique requirements. One common working scene is in cement and concrete production facilities, where large quantities of raw materials like limestone, clay, and gypsum are stored in silos and need to be conveyed to mixing stations. The equipment in this scenario must handle high volumes of material with minimal downtime, ensuring continuous production. Another typical working scene is in chemical processing plants, where various powders and granules are used in the manufacturing of chemicals. The conveying system must maintain strict contamination control, as even small amounts of impurities can affect the quality of the final product. Additionally, in food processing industries, the equipment is used to transport ingredients like flour, sugar, and spices, where hygiene and safety are paramount. The system is designed with stainless steel components and sealed pipelines to prevent cross-contamination and ensure compliance with food safety regulations.
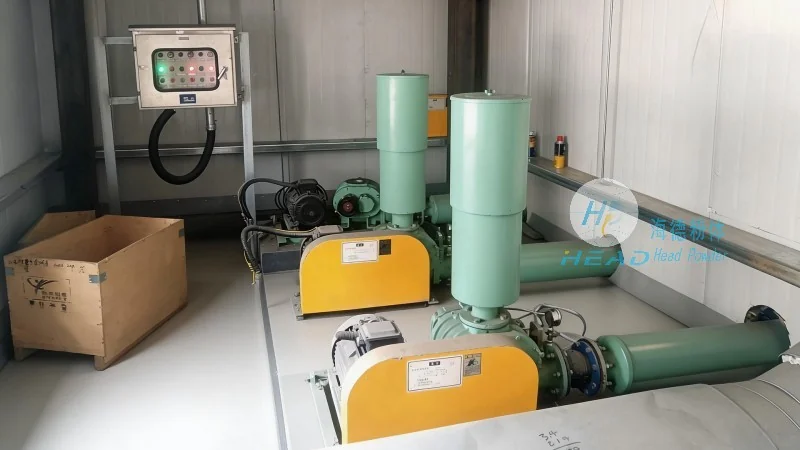
Advantages and Applications
The gray storage material conveying system equipment offers several advantages that make it suitable for a wide range of industrial applications. One of the primary advantages is its ability to handle large volumes of material with high efficiency, reducing labor costs and increasing production throughput. The system is also highly flexible, as it can be easily integrated with existing storage and processing equipment. This adaptability allows companies to scale their operations without significant modifications to the conveying system. Furthermore, the equipment is designed for durability and low maintenance, with components that are resistant to wear and corrosion. This reduces the overall operational costs and extends the lifespan of the system. The applications of this equipment span multiple industries, including construction, chemical manufacturing, food processing, and pharmaceuticals. In each of these industries, the conveying system plays a crucial role in ensuring smooth material flow and maintaining production efficiency.




