Understanding the operational principles and application scenarios of molybdenum concentrate powder material handling systems is crucial for optimizing industrial processes in mining and metallurgical sectors. This article delves into the technical foundation and practical deployment aspects of such systems, providing insights into their design, functionality, and real-world implementation.
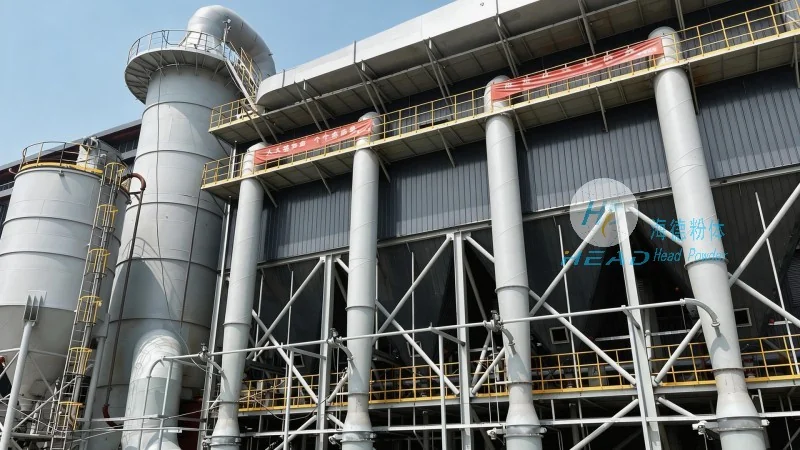
Overview of Molybdenum Concentrate Powder Material Handling Systems
Molybdenum concentrate powder, a critical raw material in the production of molybdenum-based alloys and chemicals, requires specialized handling equipment to ensure efficiency, safety, and product integrity. The material handling systems designed for molybdenum concentrate powder typically integrate multiple components, including feeding mechanisms, conveying devices, storage solutions, and control systems. These systems are engineered to address the unique challenges posed by the fine, abrasive, and sometimes hazardous nature of molybdenum concentrate powder, such as dust generation, caking, and material flow variability.
Core Components and Working Principles
The fundamental principle of molybdenum concentrate powder material handling systems revolves around the efficient transfer of material from one point to another while maintaining consistent flow rates and minimizing material degradation. Key components include:
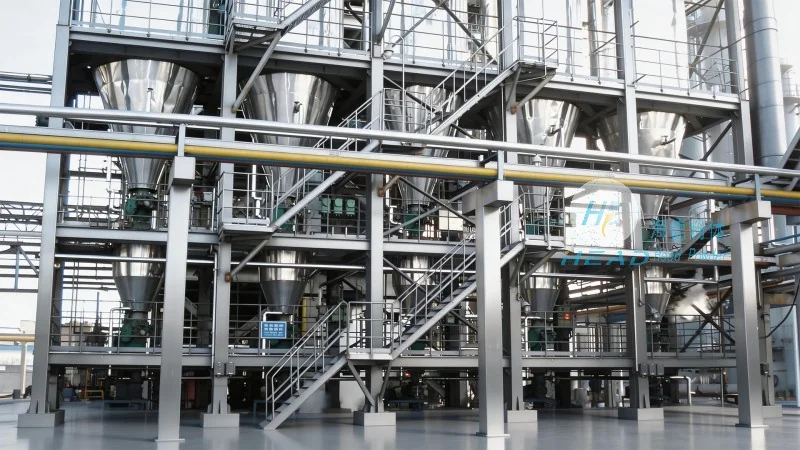
- Feeding Equipment: Typically, rotary valves or screw feeders are used to control the flow of molybdenum concentrate powder from storage silos or hoppers into the conveying system. These devices ensure a steady and controlled feed, preventing overloading or underflow that could disrupt the entire process.
- Conveying Systems: For long-distance or elevated material transport, pneumatic conveying systems or belt conveyors are commonly employed. Pneumatic systems use air pressure to move the powder through pipelines, while belt conveyors rely on friction to transport material along a continuous belt. The choice of conveying method depends on factors like material properties, distance, and budget constraints.
- Storage Solutions: Bulk storage silos or hoppers are essential for storing molybdenum concentrate powder before processing. These structures are designed to prevent material caking and ensure uniform material flow. Some systems incorporate agitators or vibrators to maintain material mobility within the storage vessel.
- Control Systems: Advanced control systems, often integrated with sensors and automation software, monitor and regulate the entire material handling process. These systems can adjust feed rates, conveyor speeds, and storage levels in real-time, optimizing operational efficiency and reducing downtime.
Working Scene Characteristics and Application Examples
The working scene characteristics of molybdenum concentrate powder material handling systems vary based on the specific industrial application. For instance, in mining operations, these systems are often deployed in ore processing plants where molybdenum concentrate is extracted from ore and then transported to refining facilities. The systems must handle large volumes of material and operate under harsh environmental conditions, such as high temperatures and dust exposure.
In metallurgical plants, the material handling systems are integrated into production lines that convert molybdenum concentrate into molybdenum metal or molybdenum compounds. Here, the systems need to maintain high purity standards, as any contamination or material degradation can affect the quality of the final product. The working environment may involve high-pressure or high-temperature processes, requiring specialized equipment with robust construction and corrosion resistance.
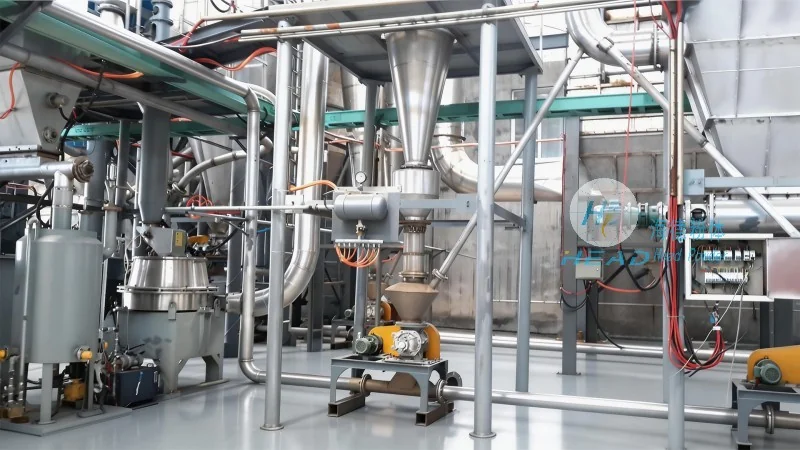
Operational Advantages and Industry Standards
Implementing molybdenum concentrate powder material handling systems offers several operational advantages. These include improved process efficiency through automated control, reduced labor costs due to minimized manual handling, and enhanced safety by minimizing human exposure to dust and hazardous materials. Additionally, these systems help in maintaining consistent product quality by ensuring uniform material flow and preventing segregation or caking.
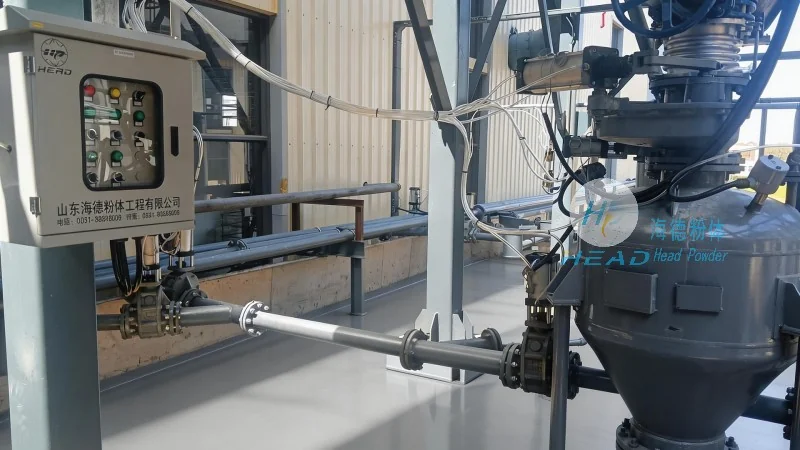
Compliance with industry standards, such as those set by the International Organization for Standardization (ISO) and the American Society of Mechanical Engineers (ASME), is critical for ensuring the safety and reliability of molybdenum concentrate powder material handling systems. These standards cover aspects like equipment design, material handling safety, and environmental protection, ensuring that systems meet regulatory requirements and perform reliably over their service life.
Conclusion
Molybdenum concentrate powder material handling systems are sophisticated industrial solutions designed to meet the demanding requirements of the mining and metallurgical industries. By understanding their working principles and application scenarios, businesses can optimize their operations, enhance product quality, and ensure compliance with industry standards. The integration of advanced technology and robust engineering in these systems makes them essential for the efficient and safe handling of molybdenum concentrate powder in various industrial settings.




