When it comes to efficiently managing paper chip materials in industrial settings, specialized material handling systems play a crucial role. These systems are designed to transport, sort, and process paper chips with precision, ensuring optimal workflow and productivity. Understanding the underlying principles and the specific characteristics of working scenes is essential for selecting the right equipment for your operations.
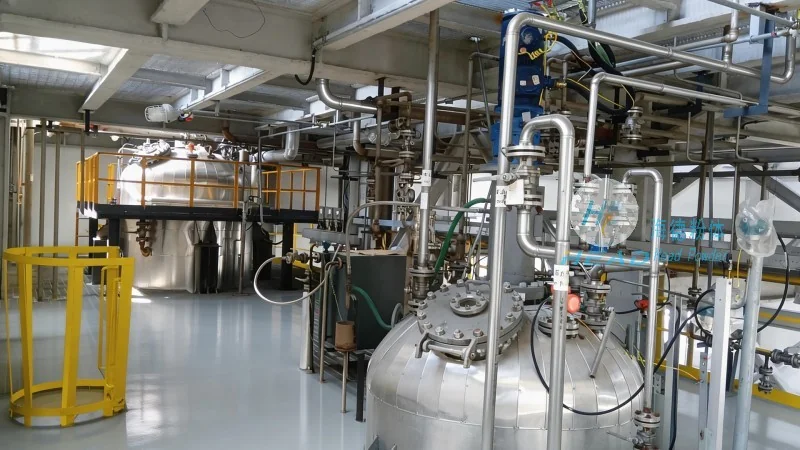
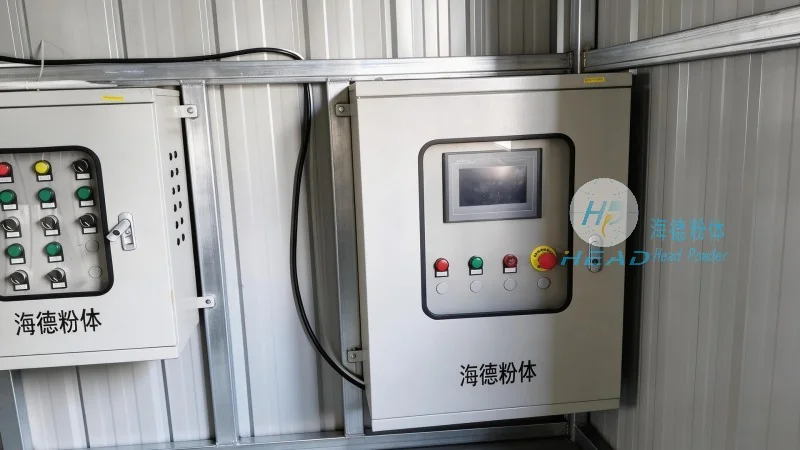
The Working Principles of Material Handling Equipment for Paper Chips
At the heart of paper chip material handling systems lies a combination of mechanical, electrical, and control technologies. The primary function is to move paper chips from one location to another within a production facility or processing plant. This is typically achieved through various types of conveyors, such as belt conveyors, screw conveyors, or chain conveyors, each tailored to the specific characteristics of the paper chip material—like size, weight, and moisture content. The systems often incorporate sensors and control panels to monitor the flow of materials, adjust speed, and prevent blockages or jams. Additionally, many modern systems use automation and digital controls to enhance efficiency and reduce human intervention, ensuring consistent performance and minimizing downtime.
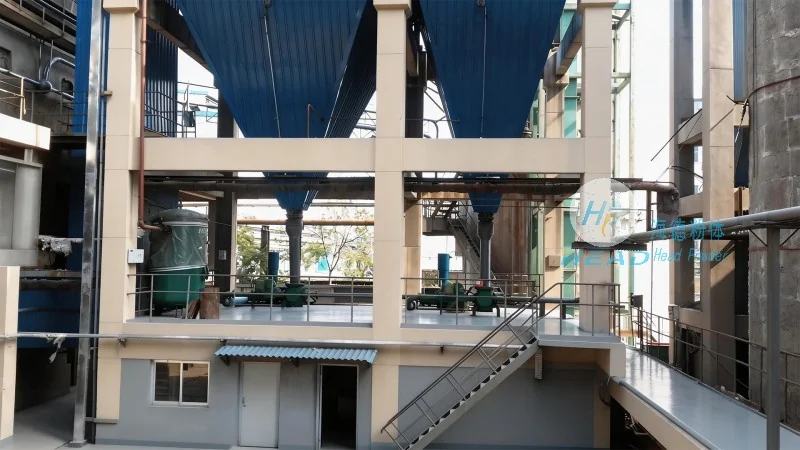
Key Working Scene Characteristics of Paper Chip Material Handling Systems
The effectiveness of paper chip material handling systems is heavily influenced by the specific working scenes in which they operate. These characteristics can vary significantly based on the industry, production scale, and the nature of the paper chip material being handled. For instance, in the paper and pulp industry, systems may need to handle large volumes of wet or dry chips, requiring robust and water-resistant components. In contrast, in recycling facilities, the systems might need to sort different types of paper chips, incorporating sorting mechanisms like magnetic separators or optical sensors to separate recyclable materials from non-recyclables. The working environment, including factors like temperature, humidity, and dust levels, also impacts the design and selection of the equipment. Systems designed for harsh environments may feature corrosion-resistant materials and sealed components to ensure durability and reliability. Furthermore, the layout of the facility and the need for integration with other production lines or machinery also influence the choice of material handling solutions. Whether in a small-scale workshop or a large-scale industrial plant, the right system must adapt to the unique demands of the working scene to maximize operational efficiency.
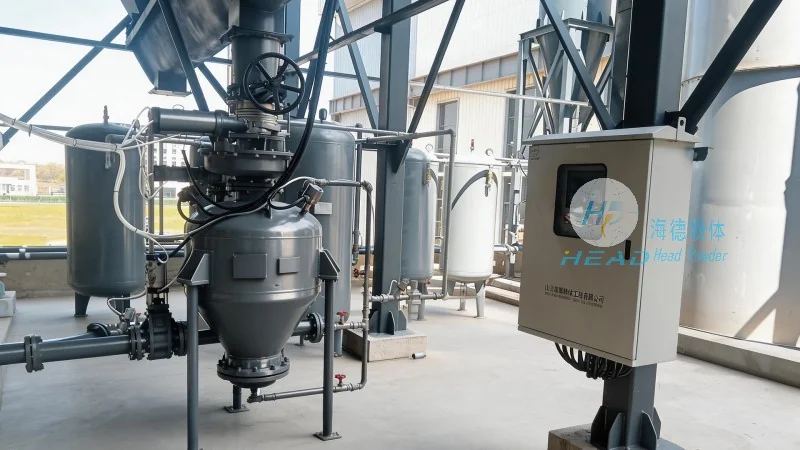
HeadPowder Engineering: Providing Innovative Solutions for Paper Chip Material Handling
Shandong HeadPowder Engineering Co., Ltd., a leading manufacturer based in Shandong, China, specializes in developing and supplying high-quality paper chip material handling systems. With years of experience in the industry, HeadPowder Engineering has developed a range of equipment tailored to meet the diverse needs of clients across various sectors. The company’s systems are designed with the core principles of efficiency, reliability, and adaptability in mind, ensuring they can handle a wide variety of paper chip materials and working conditions. By leveraging advanced technology and robust engineering, HeadPowder Engineering’s solutions help businesses streamline their material handling processes, reduce operational costs, and improve overall productivity. The company’s commitment to quality and customer satisfaction is reflected in its comprehensive product line, which includes conveyors, sorters, and control systems, all engineered to deliver superior performance and longevity. Whether you are in the paper manufacturing, recycling, or related industries, HeadPowder Engineering offers the expertise and equipment needed to optimize your paper chip material handling operations.




